Introduction: C45 in the DIN 17200 Family
C45 is the most widely used medium-carbon steel in the German DIN 17200 standard (now superseded by EN 10083-2, but still specified on drawings and purchase orders across Europe and export markets). With approximately 0.45% carbon, it occupies the sweet spot between machinability and strength — hard enough to wear well, soft enough to machine without exotic tooling, and responsive to heat treatment in ways that make it the default shaft and axle grade for German-engineered machinery.
This guide covers C45’s full specification: chemical composition, mechanical properties, hardness, heat treatment, international equivalents, and what buyers should verify when sourcing from Chinese mills that advertise “DIN C45” or “C45E” supply.
Chemical Composition (DIN 17200 / EN 10083-2)
| Element | C45 (1.0503) Min – Max % | C45E (1.1191) Note |
|---|---|---|
| Carbon (C) | 0.42 – 0.50 | Same; E = controlled sulfur for machinability |
| Silicon (Si) | ≤ 0.40 | Same |
| Manganese (Mn) | 0.50 – 0.80 | Same |
| Phosphorus (P) | ≤ 0.030 | ≤ 0.030 |
| Sulfur (S) | ≤ 0.035 | 0.020 – 0.040 (deliberately higher for chips) |
| Chromium (Cr) | ≤ 0.40 | Same |
| Nickel (Ni) | ≤ 0.40 | Same |
| Molybdenum (Mo) | ≤ 0.10 | Same |
The base grade is C45 (1.0503). C45E (1.1191) is the “improved machinability” variant with controlled sulfur; C45R adds lead for even freer machining but is restricted in some jurisdictions. For general engineering, C45 or C45E are the grades buyers encounter.
Mechanical Properties by Delivery Condition
EN 10083-2 defines several delivery conditions, each with different property targets:
| Condition | Yield (MPa) | Tensile (MPa) | Elongation (%) | Hardness (HB) |
|---|---|---|---|---|
| +U (Untreated) | — | — | — | ≤ 255 |
| +A (Annealed) | — | — | — | ≤ 207 |
| +N (Normalized) | ≥ 305 | 570 – 710 | ≥ 16 | ≈ 170 – 210 |
| +QT (Quenched & Tempered)* | ≥ 370 – 490 | 630 – 780 | ≥ 14 – 17 | ≈ 190 – 250 |
* QT values depend on the tempering temperature selected by the producer to meet the agreed hardness window.
Practical note for buyers: if your drawing says “C45” with no condition symbol, you will receive +U (as-hot-rolled) material at up to 255 HB. That is too hard for comfortable machining on many manual lathes. Specify +A (annealed) for heavy machining, +N for general structural use, or +QT with a hardness range when strength is critical.
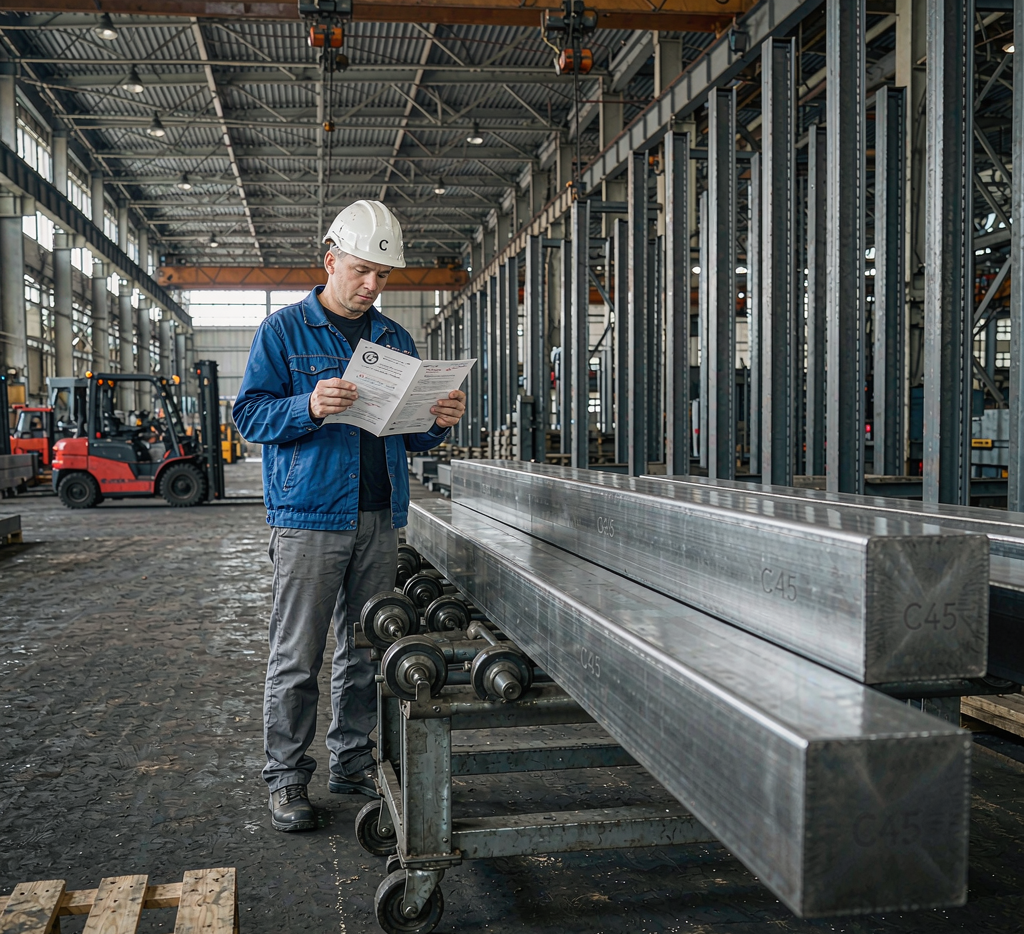
Hardness and Heat Treatment Response
C45’s 0.45% carbon content makes it an ideal candidate for through-hardening in small sections and surface hardening in larger ones:
- Annealed (+A): 163 – 207 HB. Soft, machinable, minimal internal stress.
- Normalized (+N): 170 – 210 HB. Uniform grain structure, good for welding and subsequent machining.
- Quenched & tempered (+QT): temper at 550°C → ~28 HRC (≈ 270 HB); temper at 400°C → ~40 HRC; temper at 200°C → ~52 HRC. The usual engineering window is 28 – 34 HRC for shafts and 40 – 45 HRC for wear parts.
- Induction hardened: surface to 55 – 60 HRC with a tough, unhardened core. Common for bearing journals and gear teeth on large shafts where through-hardening is impractical.
International Equivalents
| Germany (DIN/EN) | USA (ASTM/SAE) | Japan (JIS) | China (GB) | Britain (BS) |
|---|---|---|---|---|
| C45 / 1.0503 | 1045 | S45C | 45# / 45钢 | 080M46 |
| C45E / 1.1191 | 1045 (resulfurized) | S45C (S-content control) | — | — |
For general engineering, C45, 1045, and S45C are treated as interchangeable. For pressure equipment or structural code work, check the specific standard’s notch-toughness and through-thickness requirements — they vary.
Machinability and Tooling
C45 in the annealed or normalized condition machines well with standard carbide inserts. Expected cutting speeds: 180 – 250 m/min for turning with coated carbide, 20 – 35 m/min for drilling with HSS. Chip breaking is acceptable; use a chip-breaker geometry for automated lathes. C45E with elevated sulfur produces smaller, more brittle chips and allows 10 – 15% higher speeds, at the cost of slightly reduced transverse toughness.
Weldability
C45 is weldable with precautions. Carbon equivalent (IIW) runs 0.55 – 0.65, which places it in the preheat zone:
- Up to 12 mm: low-hydrogen electrodes, 100°C preheat recommended.
- 12 – 25 mm: 150 – 200°C preheat, low-hydrogen process, controlled interpass.
- Over 25 mm: 200 – 250°C preheat; post-weld stress relief at 550 – 600°C strongly advised.
Many designers avoid welding C45 and opt for keyed or shrink-fit joints instead. If welding is unavoidable, specify +A or +N delivery to minimize as-rolled hardness in the heat-affected zone.
Common Applications
- Transmission shafts, crankshafts, and spindle axles
- Gears, pinions, and sprockets (often induction-hardened on teeth)
- Connecting rods and hydraulic piston rods
- Machine tool beds and structural frames where moderate strength is sufficient
- General forgings and normalized bar for welded fabrications
What Buyers Should Verify
- Delivery condition symbol (+A, +N, +QT) on the order and certificate
- For +QT: tempering temperature and resulting hardness range on the MTC
- Heat number traceability from ladle to bar marking
- Dimensional tolerance per EN 10060 (round bar) or EN 10059 (plate)
- EN 10204 3.1 or 3.2 certificate type
- For C45E: sulfur range to confirm machinability variant
Frequently Asked Questions
1. What is the difference between C45 and C45E?
C45E is a resulfurized variant with controlled sulfur (0.020 – 0.040%) for improved machinability. Mechanical properties are essentially the same; C45E forms smaller chips and allows higher cutting speeds.
2. Can C45 reach 60 HRC?
Only on the surface via induction or flame hardening. Through-hardened C45 in water quench reaches roughly 55 HRC at the surface but falls off rapidly in sections over 20 mm. For through-hardness above 50 HRC in large sections, move to 4140/42CrMo4.
3. Is C45 the same as 1045 steel?
Functionally yes for general engineering. ASTM 1045 and DIN C45 are both approximately 0.45% carbon with similar Mn levels. For code-governed work, verify the specific standard’s test requirements.
4. What hardness should I expect from normalized C45?
Typically 170 – 210 HB. If your application needs softer material for machining, order +A (annealed) at ≤ 207 HB. If you need higher strength, specify +QT with a target hardness window.
5. Can I buy C45 from Chinese mills?
Yes — Chinese 45# (GB/T 699) is the direct equivalent. Many Chinese mills are certified to EN 10083-2 and can supply C45 with EN 10204 3.1 certificates. Verify the mill’s certification scope and request a sample MTC before placing the first order.
Conclusion
C45 is the workhorse of medium-carbon engineering steels — predictable, heat-treatable, machinable, and globally understood. The key to sourcing it successfully is specifying the delivery condition: +A for machining, +N for welding and structural use, +QT for strength. A purchase order that says only “C45” invites the cheapest delivery condition the mill can supply, which may not match your workshop’s needs.
Huaxia-Steel supplies DIN C45 / EN 10083-2 C45E round bar, plate, and forgings in annealed, normalized, and quenched-and-tempered conditions, with EN 10204 3.1 certification. Send us your size, condition, and hardness target for a same-week quotation.