Most carbon steel plate and coil produced in a hot strip mill develops a tight, dark blue mill scale (magnetite / Fe3O4) on its surface. Mill scale is brittle, cracks under forming strain, and accelerates corrosion in storage and service. Removing it cleanly is not optional — paint adhesion, galvanneal quality, cold-rolling performance, and downstream forming all depend on the surface being free of oxides. The standard industrial method to deliver that clean surface is pickling followed by oiling, often abbreviated as P&O in mill parlance.
This article walks through the pickling and oiling process step by step — chemistry, line layout, time/temperature control, environmental controls, surface quality targets, and the procurement specifications you should put on the purchase order to ensure you receive material with a clean, uniformly oiled, easily stored surface.
What Is Pickling and Oiling?
Pickling is a chemical surface-cleaning process that uses hot acid solutions to dissolve iron oxides (mill scale, rust, and welding discoloration) from the surface of carbon steel. Once the steel is scale-free, it is immediately protected from re-oxidation by a controlled application of rust-preventative oil. The combined pickling line (PL) or pickle-and-oil line (P&O line) integrates these operations into a single continuous process for hot-rolled coil and plate.
Why Pickling-and-Oiling Matters
- Removes mill scale and rust: Mill scale from hot rolling has poor paint adhesion and cracks under forming strain. Pickling provides a uniform, oxide-free substrate.
- Provides temporary corrosion protection: Oil coating prevents flash rust during warehouse storage and shipping.
- Improves downstream processing: Cold-rolling, galvanizing, and painting all require a scale-free surface to avoid surface defects.
- Enables tight thickness tolerance: Pickled coil has a more consistent surface, which improves cold-rolling mill gauge control.
- Improves weld and braze quality: Clean steel welds more uniformly with less spatter and porosity.
The Pickling Acid Chemistry
Three acid systems dominate carbon steel pickling. Each has its own operating characteristics, waste handling requirements, and suitability for different grades.
| Acid System | Concentration (typical) | Temperature (°C) | Pros | Cons |
|---|---|---|---|---|
| Hydrochloric acid (HCl) | 10 – 20% | 60 – 90 | Fast pickling, good scale removal, easy regeneration, less hydrogen embrittlement | Aggressive fume (HCl vapor), requires fume scrubbers |
| Sulfuric acid (H2SO4) | 8 – 25% | 70 – 95 | Cheaper acid, well-known chemistry, suitable for thicker scale | Slower pickling, risk of over-pickling (iron loss), higher hydrogen embrittlement |
| Mix acid (HCl + H2SO4 blends) | — | — | Combined benefits | Complex waste handling |
Most modern pickling lines use hydrochloric acid (HCl) at 12 – 18% concentration and 75 – 85 °C temperature because of faster cycle times, better surface finish, and easier acid regeneration by absorption of the spent liquor on resin beds or spray-roaster regeneration.
Acid Inhibitor Additives
To reduce acid attack on the bare metal after scale removal (called “overpickling” or “iron loss”), pickling baths include organic inhibitors — typically 0.1 – 0.5% of compounds like Rodine, Berol, or proprietary formulations based on amines or fatty alcohols. Inhibitors reduce the dissolution rate of the clean steel by 70 – 90% while leaving the acid attack on oxide largely unchanged. The typical pickling loss in a modern inhibited HCl line is 0.5 – 2.0% of strip thickness per side.
The Pickling Line Layout
A modern continuous pickle-and-oil line has these stages:
- Entry section / pay-off reel: Coil loading, uncoiling, cropping of weld points.
- Welding / stitching: Joining coil ends by flash-butt welding or stitching for continuous processing.
- Looper tower: Accumulates strip to allow continuous threading while entry / exit sections stop.
- Pre-heating (optional): Pre-heating the strip to 40 – 60 °C improves pickling efficiency and reduces thermal shock.
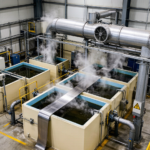
- Pickling tanks (3 – 5 in series): Counter-current acid flow: fresh acid in the last tank, spent acid overflows from the first. Each tank exposes the strip for 15 – 60 seconds.
- Water rinse: Two stages of deionized or fresh water rinse to remove residual acid and dissolved iron salts.
- Hot water rinse / passivation: Final rinse with hot water (60 – 80 °C) often with a mild alkaline passivation additive.
- Air drying / squeeze rolls: Removes bulk surface water before oiling.
- Electrolytic cleaning (optional): Some lines add cathodic or anodic electrolytic cleaning for extra cleanliness.
- Oiling station: Roll coater or electrostatic oiler applies 0.5 – 3.0 g/m² of rust-preventative oil per side.
- Tension leveler / stretcher:
- Side trimmer: Trims uneven edges.
- Inspection station: Visual and surface quality check.
- Exit section / tension reel: Recoils the finished P&O coil for banding and shipping.
Process Parameters You Should Know
| Parameter | Typical Value | Effect |
|---|---|---|
| HCl Concentration | 12 – 18% | Higher = faster pickling, more acid fume |
| Pickling Temperature | 75 – 85 °C | Higher = faster, but more vapor and uniform attack |
| Strip Speed | 60 – 180 m/min | Faster = shorter pickle time per meter, requires higher acid temp |
| Total Pickling Time (cumulative across tanks) | 45 – 180 s | Longer = more complete scale removal, more iron loss |
| Iron Content (in bath, max) | 80 – 130 g/L Fe | Higher = reduced efficiency, must be regenerated |
| Rinse Water Temperature | 60 – 80 °C | Hot rinse = better drying, fewer residues |
| Oil Coating Weight | 0.5 – 3.0 g/m² per side | Higher = better corrosion protection, but may interfere with welding or painting |
| Oil Type (typical) | Rust-preventative mineral oil (Type I, Class A) | Suitable for indoor storage up to 6 – 12 months |
| Surface Roughness after Pickling | Ra 2 – 8 μm | Profiled for paint adhesion or smoother for cosmetic panels |
After Pickling: Surface Quality Targets
The output of a well-controlled pickle-and-oil line should meet these surface criteria:
- Color: Uniform pale gray to off-white. Streaks of dark gray indicate residual mill scale; rust stains indicate insufficient oil.
- Surface roughness: Ra 2 – 5 μm typical for hot-rolled pickled coil suitable for further processing.
- No visible scale: At inspection station, scan with UV lamp or visual under angled lighting.
- Oil uniformity: Coating weight checked by FTIR or gravimetric wipe at multiple points along coil.
- No acid residue: pH of surface water extract should be ≥4.5 to prevent in-package corrosion.
Common Pickling Defects and How to Avoid Them
| Defect | Symptom | Cause | Prevention |
|---|---|---|---|
| Residual scale | Dark streaks, rough patches | Insufficient pickle time, low temperature, dirty acid | Increase temp / time, monitor acid concentration |
| Pitting | Pin-hole pock-marks on surface | Over-pickling, high Fe in bath, no inhibitor | Replace bath, add inhibitor, reduce time |
| Streaking | Lighter / darker bands along coil length | Non-uniform acid flow, damaged squeeze rolls, oscillation issues | Service leveler rolls, adjust oscillation frequency |
| Flash rust | Orange staining within 24 h of pickling | Oil coat too thin, oil type wrong, storage humidity | Increase oil coat, switch to Type II oil, dry storage |
| Hydrogen embrittlement | Delayed cracking in high-strength grades | Excessive H2 pickup from acid bath, especially H2SO4 | Bake after pickling (200 °C for 4 h), use HCl rather than H2SO4 |
| Pickling stain / black spots | Dark spots, often in patches | Localized acid attack, inhibitor uneven | Improve inhibitor mixing, check water rinsing |
Pickling-and-Oiling Specifications to Put on the PO
When purchasing P&O coil or plate, include the following in your purchase order or technical specification:
- Surface finish: “Pickled and oiled, suitable for further cold rolling / painting / galvanizing as applicable.”
- Oil type and weight: Specify the oil grade (e.g., “ASTM A1008 Commercial Steel rust-preventative oil type, 1.0 – 2.0 g/m² per side”).
- Surface roughness maximum: If needed, specify Ra value (e.g., “Ra ≤5 μm”).
- Surface cleanliness: “Free of mill scale, rust, and acid residue; pH of surface extract ≥4.5.”
- Flash-rust limit: “No visible rust staining on receipt at the buyer’s warehouse, for a period of X weeks / months from shipment.”
- Storage life: Specify how long the surface must remain rust-free under defined storage conditions.
Environmental and Waste Treatment
Pickling generates acidic wastewater with high iron content, plus acid mists and vapors. Modern lines include:
- Acid regeneration: Spray-roaster or fluid-bed system recovers HCl from iron chloride, returning it as fresh acid.
- Wastewater treatment: Neutralization with lime (Ca(OH)₂) to precipitate iron as iron hydroxide sludge, then settling and filtration.
- Fume scrubbing: Packed-tower scrubbers with NaOH solution to capture HCl vapor before discharge.
- Sludge handling: Iron hydroxide sludge is dewatered and either landfilled (regulated) or, increasingly, sent for metal recovery in cement kilns or steelmaking.
A modern integrated steel mill with full pickling effluent treatment can recycle 95 – 99% of its acid and nearly all of its rinse water — making pickling a far more sustainable process than it was 30 years ago.
P&O vs. Other Surface Conditions for Hot-Rolled Coil
| Surface Condition | Surface State | Typical Application |
|---|---|---|
| Hot-Rolled, Mill Scale (HR) | Dark blue / black mill scale intact | Structural applications, plate for fabrication where scale is acceptable |
| Pickled and Oiled (P&O) | Clean gray, oiled | Cold-rolling feed stock, tube manufacturing, fabrication needing clean weld surface |
| Pickled, Oiled, and Skin-Passed | Clean, lightly temper-rolled for flatness | Automotive exposed panels, high-precision stampings |
| Cold-Rolled (CR) | Smooth, bright, oiled | Appliances, automotive, deep-drawing applications |
| Galvanized (GI / GA) | Zinc-coated (hot-dip or galvanneal) | Outdoor construction, automotive body, HVAC |
The acid regeneration circuit turns waste pickle liquor (iron chloride) back into reusable acid. The two dominant technologies:
| Method | Output | Recovery Rate | Energy Cost |
|---|---|---|---|
| Spray Roaster | Iron oxide powder + 18 – 20% HCl | 95 – 99% | High (450 – 600 °C) |
| Fluid-Bed Reactor | Iron oxide powder + 18 – 20% HCl | 95 – 99% | High (200 – 350 °C) |
| Resin Ion Exchange | Clean water + iron chloride solution | Recovered as iron oxide after drying | Medium |
The recovered iron oxide is often sold as raw material for pigments, ferrite production, or steelmaking feedstock — closing the loop.
Pickling vs. Mechanical Descaling
For heavy plate and large-diameter pipe, mechanical descaling methods are also used. Each has trade-offs:
| Method | Mechanism | Pros | Cons |
|---|---|---|---|
| Shot Blasting | Steel shot impacts surface, fractures scale | No acid, no fumes, works for thick plate | Roughens surface; can leave embedded shot |
| Combined: shot removes 80 – 90% of scale; pickle removes remainder | Faster, less acid consumption | Higher capital cost for two lines | |
| Water-Jet Descaling | High-pressure water spray erodes scale | No chemical, no fumes | Slower than acid; limited effectiveness on heavy scale |
| Molten NaOH bath reacts with scale | Effective for stainless, also for heavy scale | Energy-intensive |
Modern carbon steel pickling lines use shot-blasting followed by light pickling — this combination reduces acid consumption by 30 – 50%, lowers wastewater volume, and produces a more uniform surface for downstream processing.
Specific Energy and Water Consumption
A typical continuous pickle-and-oil line operating at 120 m/min consumes (per ton of strip processed):
| Input | Quantity |
|---|---|
| Hydrochloric acid (100% HCl basis) | 5 – 8 kg/t |
| Process water (rinse + make-up) | 1.5 – 3.0 m³/t |
| Steam (for heating acid bath) | 40 – 70 kg/t |
| Rust-preventative oil | 0.6 – 2.0 kg/t |
| Electrical power (line drives) | 50 – 80 kWh/t |
| Lime (for wastewater treatment) | 8 – 12 kg/t |
Modern state-of-the-art lines with full energy integration, water cascading, and heat recovery can reduce these by 20 – 40% — making P&O coil more sustainable than older plants.
History and Modern Adoption
Pickling was first applied industrially for steel in the late 1800s, originally using sulfuric acid. The switch to hydrochloric acid in continuous lines began in the mid-20th century, with widespread adoption through the 1970s and 1980s as continuous strip mills scaled up. Today, more than 80% of hot-rolled carbon steel coil is pickled and oiled before shipment, reflecting both the technical necessity and the convenience for downstream processing.
In parallel, the coil weight has increased dramatically. Lines in 1960 processed 5 – 8 t coils at 30 – 50 m/min; modern lines process 25 – 30 t coils at 120 – 200 m/min, and the world’s most advanced mills reach 250 m/min with 40 t coils. This shift drove innovation in acid regeneration, environmental control, and defect detection.
The recent focus is on digital quality control — automated surface inspection using line-scan cameras with machine-learning defect classification. Modern lines flag defect coordinates in real time, enabling the operator to mark sections for slitting out at the exit section. This drastically reduces the rate of defect-related claims reaching customers.
Selection Guide: When P&O vs Alternatives
| Application | Recommended Surface | Reason |
|---|---|---|
| ERW tube feedstock | P&O | Scale-free for clean weld seam |
| Cold-rolling mill feed | P&O or annealed | Scale-free surface for cold roll forming |
| Stamping (auto panels) | Cold-rolled (skin-passed) | Best surface finish and uniformity |
| Hot-rolled structural use | Mill scale (no pickle) | Scale acceptable; cost-optimized |
| Outdoor construction | Galvanized (GI / GA) | Atmospheric corrosion protection |
| Painting base | P&O or cold-rolled | Clean substrate for primer adhesion |
FAQs
Does P&O coil have a storage life limitation?
Yes. The standard rust-preventative oil on commercial P&O coil gives 6 – 12 months of indoor storage protection under dry conditions. Beyond that, the oil degrades, residual moisture penetrates, and flash rust develops. For longer storage (6 – 24 months), specify Type II or Type III oil with higher inhibitor loading. For export shipping in containers, additional VCI (volatile corrosion inhibitor) paper or film is often added inside the coil eye.
Can pickled coil be welded without further surface prep?
Yes — P&O coil can be welded directly without further mechanical or chemical cleaning, which is one of the major advantages over hot-rolled mill-scale material. For best weld quality, wipe the surface with a clean dry cloth to remove excess oil (excess oil can cause porosity in gas-shielded welding). For galvanized parts, however, the zinc layer requires different welding parameter settings (lower heat input, special electrode / wire).
What is the difference between pickling and shot blasting for scale removal?
Pickling is a chemical process that dissolves the scale. Shot blasting (or grit blasting) is a mechanical process that physically hammers the scale off the surface using high-velocity steel shot. Pickling produces a smoother, more uniform surface with no embedded shot contamination. Shot blasting is preferred for very heavy plate (≥25 mm) where pickle time would be too long, and for parts with complex geometries. For continuous coil processing, pickling is the standard. For heavy plate, both pickling and shot blasting lines are used, often with plate passing through pickling after blasting.
Is pickling-and-oiling compatible with all downstream coatings?
Most downstream coatings work well on P&O steel — paints, primers, powder coats, and adhesives. The standard P&O oil layer must be removed (degreased) before most coatings, however, since oil interferes with paint adhesion. Wipe with solvent, alkaline wash, or vapor degreasing prior to coating. Some specialty oils are designed to be “weld-through” or “paint-through” and don’t require removal — check with the mill.
How does pickling affect mechanical properties?
Pickling removes surface material (typically 10 – 50 μm per side), but does not change the bulk mechanical properties of the steel. Hydrogen embrittlement is the only mechanical concern, primarily for high-strength grades (≥800 MPa tensile, like spring steel or quenched-and-tempered grades). Mitigation is to bake the steel at 200 – 250 °C for 2 – 6 hours after pickling. For standard carbon steels (≤500 MPa tensile), hydrogen embrittlement is rarely an issue.
Get a Quote
Need hot-rolled pickled and oiled (P&O) coil or plate for your project? Huaxia-Steel supplies P&O coil from 1.0 – 6.0 mm thickness and plate from 5 – 50 mm, with controlled oil coating weight, EN 10204 3.1 mill certification, and global shipping. Send your specification (grade, thickness, width, coil weight, oil type, packaging) to [email protected] for a mill-direct quotation.