Black oxide coating is one of the most requested surface conversions on carbon steel export orders — and one of the most misunderstood. Buyers ask for “black oxide” expecting everything from a decorative black finish on fasteners to a corrosion-resistant coating for hydraulic parts, and the difference between those expectations is process temperature, topcoat chemistry and salt-spray life. This guide explains how black oxide coating on carbon steel actually works: the hot alkaline process and its cold-room-temperature cousin, the conversion chemistry, why the oil or wax topcoat does most of the corrosion work, realistic salt spray numbers, dimensional effects that matter for threaded parts, and a checklist for inspecting black oxide shipments on arrival.
What Black Oxide Actually Is
Black oxide is a conversion coating — a chemical transformation of the steel surface itself, not a deposited layer like paint, plating or zinc. In the standard hot process, parts are immersed in a boiling alkaline salt solution (sodium hydroxide with nitrate and nitrite oxidizers at roughly 135–145 °C). The caustic oxidizer attacks the iron surface and precipitates magnetite — Fe3O4, a black iron oxide — which grows from and into the substrate. The resulting layer is typically 0.6–0.9 μm thick per side, so thin that threaded parts keep their gauge: a 1.5 × pitch allowance on fasteners easily absorbs it, and dimensional change is usually below the resolution of production inspection.
Because the coating is formed from the substrate, it cannot peel, chip or flake the way deposited coatings can. It also follows the surface perfectly — a ground shaft keeps its finish reading through the black; a blast-cleaned surface keeps its tooth. What black oxide does not do is provide meaningful corrosion protection by itself. Magnetite is porous at the micro scale and cathodic to the steel beneath it. Bare black oxide on carbon steel survives roughly a few hours to 24 hours of salt spray. The corrosion performance lives in the after-dip — the oil, wax or polymer topcoat that seals the pores — which is why “black oxide” in commercial language always means “black oxide plus topcoat.”
Hot Black Oxide vs Cold Black Oxide
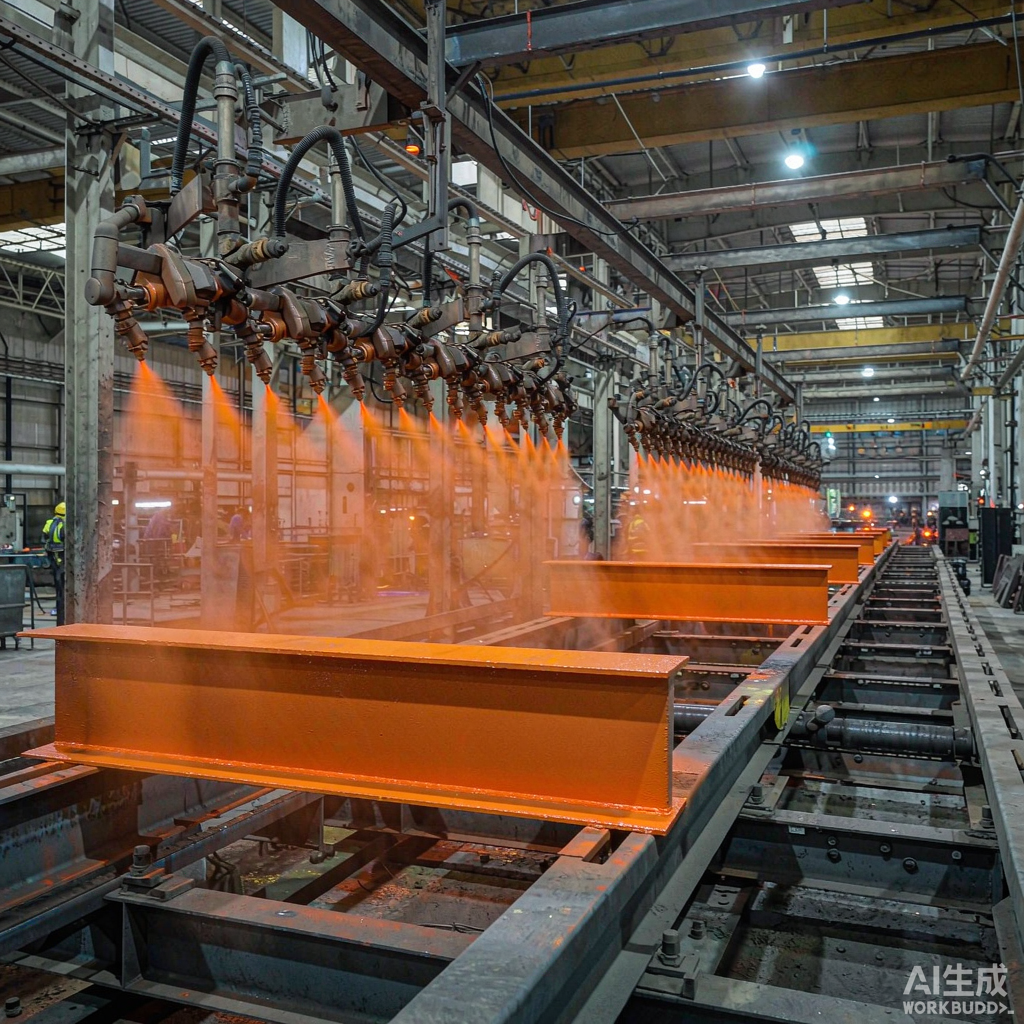
Two process families dominate, and their results are not interchangeable:
| Attribute | Hot black oxide (alkaline, 135–145 °C) | Cold black oxide (room temp, acidic) |
|---|---|---|
| Mechanism | true magnetite conversion from substrate | copper-selenium deposition compound |
| Appearance | uniform jet black, matte to satin with oil | gray-black, less uniform on alloy steels |
| Wear resistance | good — integral layer | limited — deposited film |
| Salt spray with oil topcoat | typically 24–96 h (ASTM B117) | often below 24 h |
| Dimensional change | ≈ 0.6–0.9 μm per side | slightly more, less predictable |
| Batch consistency | high, rack or barrel processed | operator sensitive |
| Typical use | fasteners, shafts, gears, tools, hydraulic parts | touch-up, decorative, small lot work |
For export-grade work the hot process is the default, and most serious coating shops in China run barrel lines for fasteners and rack lines for long parts. The cold process has legitimate niche uses — refurbishing, touch-up of machined areas, interior decorative parts — but specifying “black oxide” on a drawing without naming the process invites the cheap version. Writing “hot alkaline black oxide per MIL-DTL-13924 Class 1” or “SAE J1880” closes that loophole; both military and automotive specifications describe the hot conversion process.
The Process Line, Step by Step
A production hot black oxide line runs eight stations, and quality problems trace back to skipped or under-timed steps as often as to the black bath itself:
- 1. Alkaline clean: heated caustic soak to strip cutting oils and drawing compounds. Residual oil is the number one cause of blotchy black.
- 2. Rinse: overflow or spray rinse to stop alkaline drag-in.
- 3. Acid pickle / derust: hydrochloric or sulfuric dip removes rust, heat-treat scale and drawing scale. A 1–2 minute light pickle also activates the surface for uniform conversion.
- 4. Second rinse.
- 5. Black oxide bath: 135–145 °C boiling caustic-nitrate solution. Immersion 5–20 minutes depending on alloy and load; medium-carbon and Cr-Mo steels blacken slightly slower than plain low-carbon steel, and high-sulfur free-machining grades can need adjusted chemistry.
- 6. Rinse.
- 7. Optional second black dip for deep uniform color on large or alloy loads.
- 8. Topcoat: the performance step. Water-displacing rust-preventive oil (the standard choice), dry-to-touch waxes, emulsions, or polymer sealers are applied while parts are warm so the displacing fluid pulls water out of the pores.
The topcoat choice sets the finish and the corrosion life: light machine oil gives the classic satin black and the best salt spray; dry waxes give a cleaner-handling part with somewhat less protection; polymer sealers give a low-gloss, fingerprint-resistant finish for showroom hardware. State the topcoat on the purchase order — “black oxide, oil dip” and “black oxide, dry wax” are different products in the same trade name.
Corrosion Performance: Realistic Numbers
Black oxide is often oversold as a rust-proof finish. The honest numbers, from industry test data and specification minimums, look like this:
| System | Typical ASTM B117 salt spray to first rust |
|---|---|
| Bare black oxide (no topcoat) | 2–24 h |
| Black oxide + light rust-preventive oil | 24–96 h |
| Black oxide + heavy oil dip | up to 96–120 h |
| Black oxide + wax | 24–72 h |
| Black oxide + polymer sealer | 48–120 h depending on system |
| For comparison: zinc plating + passivation | 72–200 h (white rust) |
The practical conclusion for buyers: black oxide is an appearance, dimensional-stability and mild-humidity-protection finish, not a substitute for galvanizing, zinc plating or coatings in wet, salty or outdoor service. It excels where parts are handled, stored indoors, lightly oiled in service, or where dimensional tolerance and weldability disallow plated layers — hydraulic fittings, machine tool components, gears, firearms hardware, indoor fasteners, tools.
Dimensional, Material and Design Considerations
- Threaded and precision parts: 0.6–0.9 μm per side is below most thread tolerance allowances, which is why black oxide is the standard finish on high-strength bolts where zinc plating’s 5–8 μm buildup would threaten thread fit or hydrogen embrittlement.
- No hydrogen embrittlement risk: no electroplating current means no hydrogen charging — a decisive advantage for quenched-and-tempered parts above grade 10.9 and for springs.
- Surface pre-finish carries through: the coating follows the substrate, so burrs, tool marks and scale all remain visible under black. Decide the pre-finish (shot blast, ground, phosphated-pre-blackened) before processing, not after.
- Alloy content slows blackening: plain carbon steel converts fastest; Cr-Mo steels, silicon spring steels and cast irons need longer immersion or double dips for full color.
- Weldments: weld first, then blacken — post-welding a blackened part burns the coating and leaves an unrepaired bright patch that only a re-dip can restore.
- Heat treatment sequence: blacken after final heat treatment; the 140 °C bath cannot alter Q&T properties, but grinding after blackening cuts through the coating.
Specifications You Can Name on a PO
Black oxide is a specification desert if you let suppliers self-define. These are the citable references:
- MIL-DTL-13924 — US military black oxide: Class 1 alkaline (hot) for ferrous parts, Class 4 for corrosion-resistant steels. The most widely accepted anchor spec.
- SAE J1880 / AMS 2485 — automotive and aerospace hot alkaline black oxide; AMS 2485 carries PPG-level audit expectations.
- ASTM D5627 — standard terminology for black oxide coatings.
- Company specs (fastener OEMs, hydraulic component makers) — typically add salt spray minimums of 24–72 h with oil and color uniformity panels.
A clean purchase-order line reads: “Black oxide, hot alkaline process per MIL-DTL-13924 Class 1, rust-preventive oil topcoat, salt spray ≥ 48 h to first red rust (B117), no dimensional change beyond 1.0 μm per surface.” Suppliers who can meet that line are serious; suppliers who cannot should be disqualified for anything beyond decorative work.
Inspection Checklist on Arrival
- Color uniformity: jet black with no red tones (under-converted), rainbow interference bands (thin coating) or gray streaks (poor cleaning) across the batch.
- Topcoat present: fresh oil film or specified sealer — a chalky, dry-feeling black indicates the oil step was skipped.
- Dimensional spot check on threads and fits with go/no-go gauges; black oxide should not change gauging results.
- Adhesion: rub with white paper — light oil transfer is normal; black powder transfer means poor conversion or a wiped coating.
- Packaging: VCI paper or oil-impregnated wrap; black oxide parts packed wet against plain cardboard will rust in transit within days in humid season.
When the checklist is applied at the factory gate rather than after the sea voyage, black oxide remains one of the best value finishes in the export trade — a few cents per kilogram for a dimensionally inert, non-embrittling, professional black finish that machines, welds and gauges like bare steel.
Troubleshooting Guide: What Bad Black Oxide Looks Like
Most black oxide quality complaints trace to one of a handful of line problems, and each has a visible signature. Use this table when reviewing rejected or suspect batches — it maps what you see to the root cause and what the coating shop should do about it:
| Symptom | Most likely cause | Corrective action |
|---|---|---|
| Red-brown tint or rust spots within hours | under-converted bath (low temperature or short immersion) | verify bath at 140 °C with titration; re-dip the batch |
| Blotchy gray streaks | oil residue from poor alkaline cleaning | extend cleaning time, check cleaner concentration, re-run |
| Rainbow / interference colors | coating too thin — bath spent or time too short | recharge bath salts; double dip for alloy grades |
| Black powder wipes off | over-cooked smut not rinsed, or coating grown past limits | extend rinse; check bath concentration; reduce immersion |
| White crystalline residue | alkaline salts dragged through rinses | improve rinsing; demineralized final rinse |
| Uneven color on one rack face | parts touching or rack shadowing in bath | re-rack with spacing; rotate barrel load |
| Flash rust before blackening | parts stood too long between pickle and black bath | reduce transfer time; add activator stage |
A capable coating shop runs titration on the black bath every shift, keeps cleaning and rinse chemistry on the same control schedule, and can show you process records when asked. Shops that cannot produce bath control records are the ones that ship the blotchy lots — and the difference in price between a disciplined coater and a casual one is small relative to the cost of a reworked container.
Cost, Lead Time and Sourcing Structure
Black oxide pricing is volume-driven and process-driven. Barrel processing small fasteners in multi-ton lots lands at the bottom of the range; racked long shafts, parts needing extensive pre-cleaning (heat-treated scale, welded fabrications) or premium polymer topcoats land at the top. What does not vary much is the premium over bare steel: even the expensive end of black oxide processing stays far below zinc plating, and roughly an order of magnitude below quality powder coating. That cost position explains the finish’s dominance on machine internals — you buy a professional black, dimensionally silent finish, without paying plating money.
Lead time is best controlled by geography: the cleanest supply chains put the coater inside or next to the fastener or machining plant, so parts move from machine to bath to packed carton without an extra freight leg. When quoting finished black oxide parts, ask whether coating is in-house or subcontracted — an outsourced coater adds 3–7 transport days and a second quality gate. For scheduled programs, agree a coating schedule buffer of one week and an inspection protocol at the coater’s gate rather than after arrival; catching a bad bath lot at the coater costs a re-dip, catching it at destination costs a container return.
Black Oxide vs the Alternatives: Choosing Correctly
Black oxide competes with three other finishes for the same parts, and the selection usually comes down to one question: what does the part need protection from, and for how long?
| Finish | Corrosion life (B117) | Dimensional impact | Relative cost | Best fit |
|---|---|---|---|---|
| Black oxide + oil | 24–96 h | ≈ 0.7 μm/side — gauge-safe | 1× | precision threads, high-strength fasteners, machine internals |
| Zinc electroplate + passivate | 72–200 h | 5–8 μm/side — gauge risk on fine threads | 1.5–2× | general hardware needing real corrosion life |
| Mn-phosphate + oil | 48–120 h | 2–8 μm/side | 1.2–1.5× | gears, wear parts, anti-galling service |
| Powder / paint | 240–500 h | 60–120 μm — masking required | 4–8× | visible surfaces, outdoor equipment |
The pattern is clear: where the part is precision, high-strength, welded, or sees service in oil, black oxide wins on engineering grounds alone. Where the part is a commodity fastener for a wet climate, zinc plating wins on corrosion economics. Where the part is a gear or a wear surface, manganese phosphate is the technical sibling. Problems start when a purchase order names a finish loosely — “blackened” or “black coated” — and the supplier picks the cheapest reading. Writing the exact process and the topcoat eliminates the ambiguity for a fraction of a cent per part.
Working With Your Coating Supplier
The best black oxide results come from buyers who treat the coater as a process partner rather than a commodity vendor. Share the substrate details — steel grade, prior heat treatment, machining coolant type — because each influences the cleaning and conversion steps; a part arriving wet in sulfurized cutting oil needs a different pre-clean than a dry heat-treated gear. Approve a first-article panel with the color and topcoat you expect, and keep it as the acceptance reference for the program. Agree the inspection method in advance: color panels viewed under defined lighting, oil-film verification by weight gain, salt spray coupons per lot where the contract demands them.
On scheduled programs, reserve coating capacity the way you reserve mill capacity. Black bath lines run batch cycles and a busy coater schedules around load size; a buyer who releases parts in weekly waves gets consistent attention, while a buyer who dumps a quarterly rush onto the line gets whatever process shortcuts the schedule forces. The finish is cheap — the discipline around it is what you are actually buying.
FAQ
Does black oxide prevent rust?
Only mildly, and only with a topcoat. Bare black oxide rusts within hours of salt spray; with a proper rust-preventive oil dip it reaches 24–96 hours. For outdoor or wet service, specify galvanizing or zinc plating instead — black oxide is an appearance and dimensional-stability finish, not a corrosion barrier.
Will black oxide change my part dimensions?
By about 0.6–0.9 μm per surface — far below thread and fit tolerances. This is precisely why black oxide is preferred on precision and threaded parts where zinc plating’s 5–8 μm buildup would break gauges.
What is the difference between black oxide and phosphate coating?
Both are conversion coatings. Black oxide forms magnetite (Fe3O4) and is very thin with mild protection; manganese or zinc phosphate grows a crystalline phosphate layer 2–20 μm thick that holds more oil and gives better corrosion and anti-galling performance, at the cost of more dimensional change and a grayer finish. Phosphate + oil usually beats black oxide + oil on salt spray.
Can grade 10.9 or 12.9 bolts be black oxide finished?
Yes — and it is the preferred finish at those strength levels, because the immersion process carries no hydrogen embrittlement risk, unlike electroplated zinc which requires post-bake above grade 10.9. High-strength fasteners for machine building are commonly supplied black oxide plus oil.
How much does black oxide cost per ton?
Barrel-processed small parts typically add USD 150–350 per ton; racked large parts, USD 300–800 per ton depending on size, pre-cleaning needs and topcoat. The process is far cheaper than zinc plating or painting and adds negligible lead time when the coater is adjacent to the mill or machining supplier.
Need carbon steel parts or bars finished in hot black oxide with oil topcoat, salt spray certificates and controlled dimensional results? Send us your drawing, spec reference (MIL-DTL-13924 / SAE J1880) and quantity — Huaxia-Steel quotes finished parts with coating test data within 24 hours.