Carbon Steel Pipe Schedule Chart and Wall Thickness Explained
Every carbon steel pipe purchase order comes back to a single question: what schedule? Schedule 40, Schedule 80, Schedule 160, XXS — these designations appear in every pipe specification, every quote and every MTC. Misreading the schedule chart leads to under-rated pipe, costly rework, or over-priced material that does not fit the system.
This guide explains what pipe schedules mean, how wall thickness relates to nominal pipe size, how to read the standard ASME B36.10 / B36.19 tables, and which schedule to select for typical carbon steel applications. Whether you are sourcing A106 Gr.B, A53 Gr.B, API 5L or A333 pipe, the schedule selection rules apply the same way.
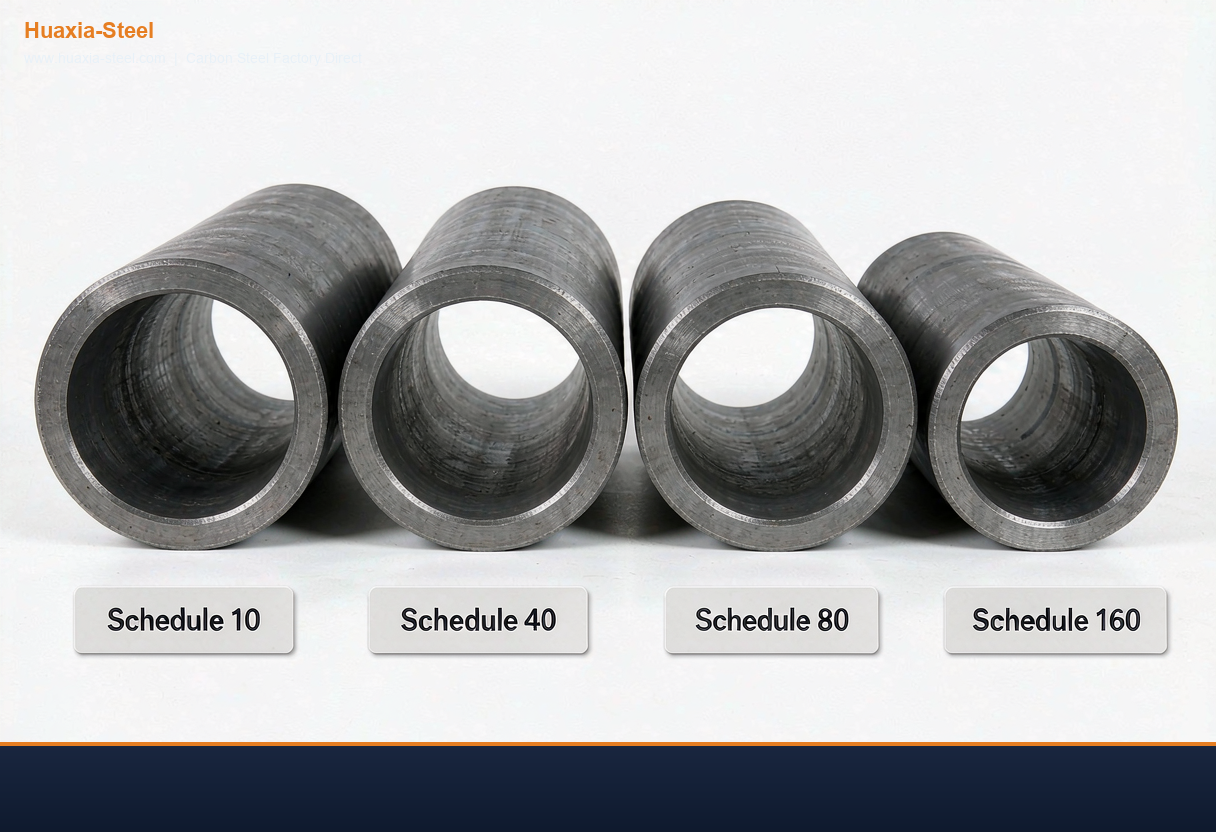
1. What is a Pipe Schedule?
Pipe schedule is a wall-thickness designation system introduced by the American National Standards Institute in 1927 and now standardised by ASME B36.10 (carbon and alloy steel) and ASME B36.19 (stainless steel). The schedule number is approximately equal to 1000 × P / S, where P is the internal design pressure and S is the allowable stress. In practical terms, higher schedule numbers mean thicker walls.
The schedule system replaced the older “standard”, “extra strong” and “double extra strong” labels. Today the schedule system covers ten standard schedules (5S, 10, 20, 30, 40, 60, 80, 100, 120, 140, 160, XXS) plus special schedules for specific applications. The two most common in carbon steel piping are Schedule 40 (Std) and Schedule 80 (XS).
2. Schedule vs Nominal Pipe Size
The schedule number alone does not define wall thickness — you also need the nominal pipe size (NPS). For the same schedule, wall thickness varies with NPS. For 1/2 inch NPS, Schedule 40 is 2.77 mm. For 16 inch NPS, Schedule 40 is 12.7 mm. The schedule is a relative measure, not a millimetre value.
Outside diameter (OD) is fixed by NPS regardless of schedule. For NPS 1, OD is 1.315 inch (33.4 mm). For NPS 12, OD is 12.75 inch (324 mm). Schedule determines the wall thickness, which determines the inside diameter (ID = OD − 2 × wall).
| NPS | OD (inch) | OD (mm) | Sch 40 (mm) | Sch 80 (mm) | Sch 160 (mm) | XXS (mm) |
|---|---|---|---|---|---|---|
| 1/2 | 0.840 | 21.3 | 2.77 | 3.73 | 4.78 | 7.47 |
| 3/4 | 1.050 | 26.7 | 2.87 | 3.91 | 5.56 | 7.82 |
| 1 | 1.315 | 33.4 | 3.38 | 4.55 | 6.35 | 9.09 |
| 1-1/2 | 1.900 | 48.3 | 3.68 | 5.08 | 7.14 | 10.16 |
| 2 | 2.375 | 60.3 | 3.91 | 5.54 | 8.74 | 11.07 |
| 3 | 3.500 | 88.9 | 5.49 | 7.62 | 11.13 | 15.24 |
| 4 | 4.500 | 114.3 | 6.02 | 8.56 | 13.49 | 17.12 |
| 6 | 6.625 | 168.3 | 7.11 | 10.97 | 18.26 | 21.95 |
| 8 | 8.625 | 219.1 | 8.18 | 12.70 | 23.01 | 22.23 |
| 10 | 10.750 | 273.0 | 9.27 | 15.09 | 28.58 | 25.40 |
| 12 | 12.750 | 323.8 | 10.31 | 17.48 | 33.32 | 25.40 |
| 16 | 16.000 | 406.4 | 12.70 | 21.44 | 40.49 | — |
| 20 | 20.000 | 508.0 | 15.09 | 26.19 | 49.99 | — |
| 24 | 24.000 | 609.6 | 17.48 | 30.96 | 59.54 | — |
4. Common Schedule Selections
For typical carbon steel piping, the following schedules are most common:
| Schedule | Typical Service |
|---|---|
| Sch 5S / 10S / 10 | Thin-wall service: condensate, low-pressure water, instrumentation |
| Sch 20 | Low-pressure process, fire water mains |
| Sch 40 (Std) | General process piping, utility steam, compressed air |
| Sch 80 (XS) | Higher-pressure process, oil and gas gathering, hot oil |
| Sch 120 | High-pressure process, refinery hydrocracker piping |
| Sch 160 | Very high-pressure: high-pressure feedwater, ammonia, ethylene |
| XXS | Specialty high-pressure: high-pressure boilers, critical steam headers |
Sch 40 is the workhorse for most general-purpose piping. Sch 80 is used where higher pressure, mechanical strength or corrosion allowance is required. Sch 160 and XXS are reserved for critical high-pressure service.
5. Wall Thickness Tolerance per ASME B36.10
ASME B36.10 specifies the wall-thickness tolerance for seamless and welded pipe. The standard tolerance is −12.5% of nominal — meaning the actual wall thickness at any point must not be less than 87.5% of the schedule value. A tighter tolerance of −10% applies to certain critical service pipe.
For pipe supplied to ASTM A106, A53, A333 or API 5L, the mill typically delivers wall thickness at or near nominal. For sour service or critical pressure piping, always specify the tightened tolerance and verify on the MTC.
6. Weight per Foot and Shipping Cost Impact
Wall thickness directly affects the pipe weight per foot, which affects both raw-material cost and shipping cost. For the same NPS, doubling the wall thickness roughly doubles the weight and therefore the cost per metre.
The chart below shows weight comparison for NPS 4 pipe:
| Schedule | Wall (mm) | Weight (kg/m) | Relative to Sch 40 |
|---|---|---|---|
| Sch 10 | 2.11 | 6.55 | 0.40x |
| Sch 20 | 4.78 | 13.4 | 0.81x |
| Sch 40 (Std) | 6.02 | 16.5 | 1.00x |
| Sch 80 (XS) | 8.56 | 22.7 | 1.38x |
| Sch 120 | 11.13 | 28.3 | 1.72x |
| Sch 160 | 13.49 | 34.0 | 2.06x |
Switching from Sch 40 to Sch 80 adds roughly 38% material weight. For a 100-tonne order, that translates to an extra 38 tonnes of steel plus the corresponding shipping, customs and handling cost.
7. How to Read an MTC Schedule Reference
On the mill test certificate, the pipe schedule is usually stated as “Schedule 40” or “SCH 40”. The corresponding wall thickness in millimetres or inches is also stated. When verifying the MTC against the purchase order, confirm three items:
- NPS matches the purchase order
- Schedule matches the purchase order
- Actual measured wall thickness falls within B36.10 tolerance (nominal −12.5%)
8. Common Procurement Errors
The three most common schedule errors in pipe procurement are:
- Confusing “Std” with Sch 40 — “Std” is Schedule 40, but the abbreviation is sometimes used loosely. Always quote the full schedule number on the PO.
- Forgetting that Sch 40 changes with NPS — Sch 40 NPS 1/2 is 2.77 mm; Sch 40 NPS 12 is 10.31 mm. Always specify NPS and schedule together.
- Selecting Sch 80 by default for “high pressure” — if the design pressure is moderate, Sch 80 is over-spec and wastes material. Compute the required wall thickness from the Barlow formula and select the next available schedule.
9. Frequently Asked Questions
Is Schedule 40 the same as Standard Weight?
Yes. “Standard” (Std) and Schedule 40 (Sch 40) are the same designation. Modern purchasing documents should use “Schedule 40” for clarity. ASME B36.10 Table 1 lists “STD” as the legacy name.
Can Schedule 80 pipe be threaded?
Generally no. Threading reduces effective wall thickness and Sch 80 pipe is rarely supplied in threadable sizes above 2 inch NPS. For threaded joints above NPS 2, use Class 2 or Class 3 threading per ASME B1.20.1 with thicker pipe, or use socket-weld connections.
What is the difference between Sch 40 and Sch 40S?
Sch 40S and Sch 40 have identical dimensions. The “S” suffix indicates ASME B36.19 stainless-steel dimension compatibility. Sch 40 pipe per B36.10 and B36.19 have the same wall thickness values.
How do I calculate the working pressure for a given schedule?
Use the Barlow formula P = (2 × S × t) / (D − 1.2 × t). For ASTM A106 Gr.B pipe (S = 20,000 psi at 200°F per ASME B31.1), NPS 4 Sch 40 (D = 4.5 in, t = 0.237 in), the internal pressure is approximately 1,890 psi. For higher temperature, S decreases — check ASME B31.1 Table A-1 for the temperature derated stress.
10. Threading Considerations for Threaded Pipe
Threaded pipe (NPT) is governed by ASME B1.20.1 in the United States and ISO 7-1 internationally. The threading process cuts a tapered thread into the pipe end, which reduces the effective wall thickness in the thread zone. For this reason, threaded pipe is typically limited to:
- Maximum NPS — 6 inch (most applications limit to NPS 2 or NPS 4)
- Maximum pressure — Class 2000 lb fittings, typically limited to 2000–2500 psi at ambient temperature
- Maximum temperature — 250°F for standard carbon steel; higher temperatures require alloy materials
Thread engagement must follow ASME B1.20.1: hand-tight engagement plus a defined number of turns beyond hand-tight. For pressure-tight joints, use thread sealant (PTFE tape, pipe dope) or weld the threaded joint for critical service. Do not rely on threads alone for critical pressure piping above 600 psi.
11. Cost and Lead Time Considerations
Schedule pricing for carbon steel pipe depends on the schedule, NPS, quantity and delivery destination. As a rule of thumb:
- Sch 10 / 20 / 30 are the lowest-cost options, typically 20–40% below Sch 40
- Sch 40 (Std) is the most common and most competitively priced schedule
- Sch 80 (XS) adds 30–50% over Sch 40 for the same NPS
- Sch 120 / 160 add 70–110% over Sch 40
- XXS can be 2–3 times the Sch 40 price due to limited mill capacity
- A106 Gr.B adds 10–20% over A53 Gr.B for the higher specification
- A333 Gr.6 adds 25–40% over A106 for low-temperature requirement
- API 5L X42 / X52 adds 5–15% over A106 for line pipe service
Standard lead time is 15–30 days for stocked Sch 40 / Sch 80 pipe and 30–60 days for mill-run orders. Special schedules (Sch 120, 160, XXS) or large-quantity orders may require 60–90 days lead time. Cut-to-length and threading add 5–10 days to standard lead time.
Need carbon steel pipe in a specific NPS and schedule for your project? Huaxia Steel supplies A106 Gr.B, A53 Gr.B, API 5L and A333 pipe in all standard schedules from Sch 10 through SSXS, with EN 10204 3.1 / 3.2 certification and SGS / BV / TUV inspection. Email [email protected] with your NPS, schedule, quantity and delivery destination, and we will reply with a mill-direct quotation within 24 hours.