Induction Bending vs Hot Bending for Carbon Steel Pipe: Process, Tolerances, and Selection
Pipe bending reshapes straight pipe into direction-changing runs without resorting to elbows. For carbon steel process piping, structural piping, and line pipe for oil and gas, induction bending and hot bending (also called “hot induction bending” or “oxy-fuel bending”) are the two dominant methods. They share the principle of heating a narrow band of the pipe and pushing it over a bend die, but the heat source, accuracy, mechanical effect on the material, and unit cost differ significantly.
This guide compares both processes and explains how to specify bending per ASME B16.49 (for line pipe) and ASME B31.3 (for process piping), where to use cold bending instead, and how to vet a carbon steel bending shop.
1. Why Bend Carbon Steel Pipe?
Common reasons to bend instead of using factory elbows:
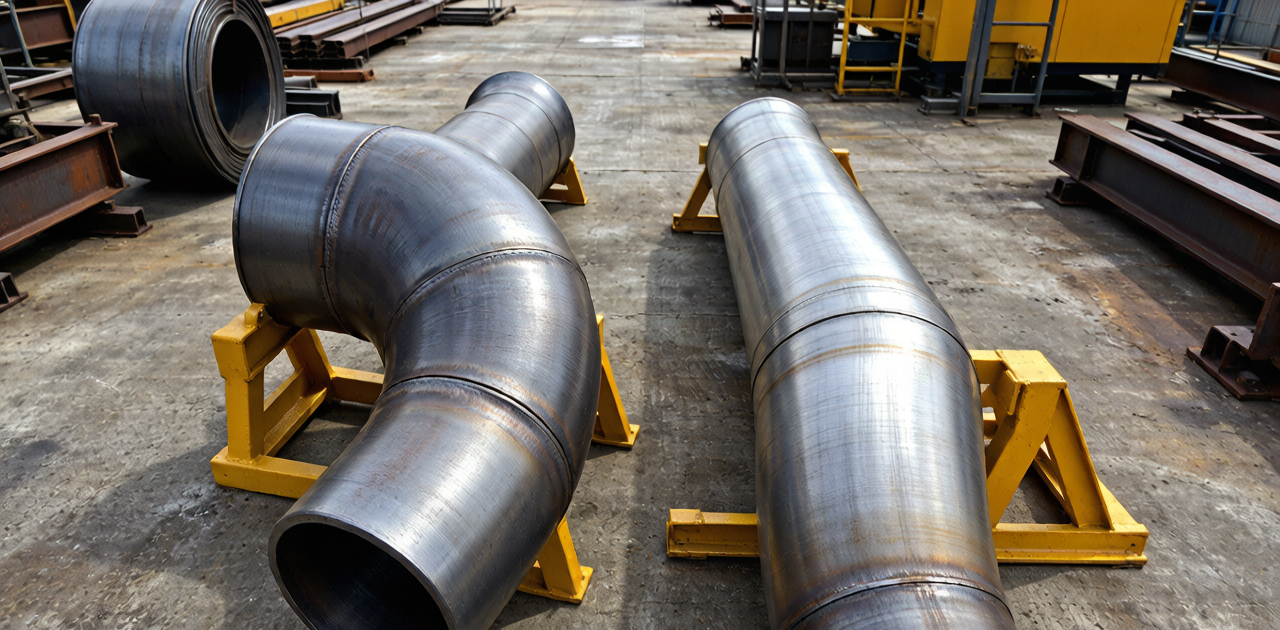
- Reduced field welds: A single long-radius bend replaces 2-4 butt-weld elbows, cutting weld cost and NDE time.
- Lower pressure drop: Smooth bends with no weld-induced turbulence are favored in slurry lines and long-distance pipelines.
- Custom radius: Field layout may require a radius that no standard elbow matches.
- Faster construction: One bend delivered to site beats three elbows plus two welds.
For pipe DN 100 to DN 600, custom bends also allow compound or multi-plane geometry that is impractical with standard fittings.
2. Process Fundamentals
2.1 Induction Bending (Cold-side / Push-Through)
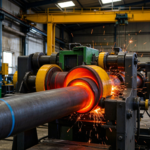
An induction coil heats a 25-50 mm wide band of the pipe to 850-1000 degrees C. A die pushes the pipe through the coil, plastically deforming the heated zone over a fixed bend radius. Cooling happens by water spray or air, depending on the steel grade. The pipe feeds continuously through the coil, so the process can produce very tight or very large radii by changing die geometry.
Key characteristics:
- Heat zone width: narrow, typically 25-50 mm.
- Heat source: high-frequency induction (1-10 kHz, kW to MW).
- Cooling rate: medium (water spray), can be modified.
- Bend angle: any angle from 1 degree to 180 degrees in one continuous pass.
- Typical radius: 3D to 10D (D = nominal pipe diameter); tighter bends possible at thinner walls.
2.2 Hot Bending (Oxy-fuel or “Pyrolysis” Method)
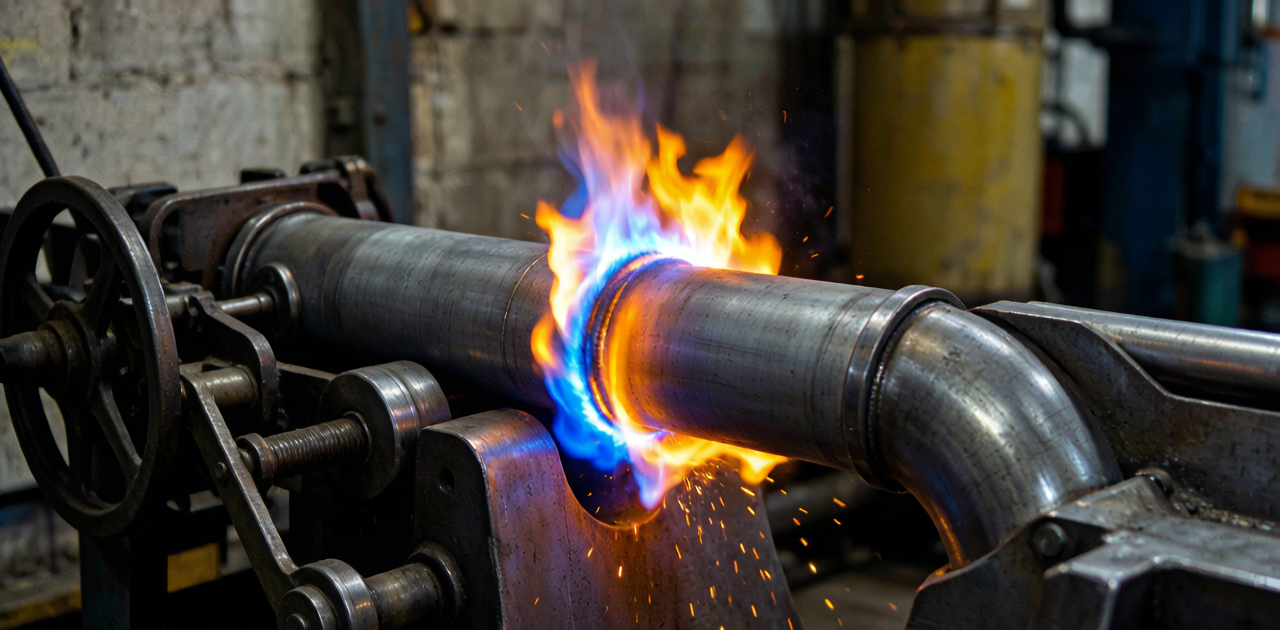
The pipe is heated with oxy-fuel torches (propane + oxygen, or natural gas + oxygen) along a wider band – typically 100-200 mm. A winch or hydraulic ram drags the pipe over the bend die. This is the older method, also called “hot induction bending” historically but distinct from modern high-frequency induction bending.
Key characteristics:
- Heat zone width: wider, 100-200 mm, with steeper thermal gradient.
- Heat source: combustion of fuel gas with oxygen, controlled manually or by CNC ring burner.
- Cooling rate: slower (air cool) to avoid hard zones.
- Bend angle: continuous, but angle accuracy is operator-dependent.
- Typical radius: 5D to 40D, well suited for large-radius piggable pipeline bends.
3. Side-by-Side Process Comparison
| Parameter | Induction Bending | Hot Bending (Oxy-fuel) |
|---|---|---|
| Heat source | High-frequency induction coil (electrical) | Oxy-fuel torch ring burner |
| Heat band width | Narrow (25-50 mm) | Wide (100-200 mm) |
| Temperature control | Precise (pyrometer + PLC) | Operator / scanner controlled |
| Repeatability | High | Moderate |
| Minimum radius | 2D-3D for small diameter; 5D for line pipe | 5D standard; tighter on thin wall |
| Maximum radius | Up to 10D routinely; larger with care | 20D-40D routinely for pipeline |
| Maximum diameter | DN 600 (24 in) typical; larger at specialty shops | DN 1200 (48 in) and larger routinely |
| Cooling | Water spray or accelerated air | Air cool (slower) |
| Power / fuel cost | Electricity (heavy infrastructure) | Oxygen + propane / natural gas |
| Setup cost | High (coil, generator, bending machine) | Lower (torches, winch) |
| Production rate | Continuous, faster per bend | Slower, more manual handling |
| Suitable batch size | Mid to high volume runs | Low to mid volume; large radius single bends |
4. Effect on Carbon Steel Mechanical Properties
4.1 Induction Bending Effect
During induction bending, the heat-affected zone (HAZ) is narrow and the cycle is short. The pipe material experiences:
- Local austenitizing in the HAZ.
- Deformation while hot, leading to grain refinement on cool-down.
- Water spray tends to produce a slightly higher hardness than air cooling – typically 10-20 HB increase in the HAZ.
- For normalized steels (e.g., ASTM A106 Gr.B, API 5L X65), the bend zone usually meets parent pipe strength; some codes ask for re-normalizing after bending.
4.2 Hot Bending Effect
The wider HAZ and slower cooling can lead to:
- Larger grain growth in the HAZ.
- Coarse-grained bainite or ferrite-pearlite depending on cooling.
- Lower hardness change than induction bending.
- Greater risk of scale, decarburization, and surface oxidation if atmosphere is not controlled.
For sour service (HIC / SSC per NACE MR0175), hot bending is usually restricted or replaced with induction bending for tighter process control.
5. Dimensional Accuracy and Ovality
Ovality – reduction in cross-section circularity due to bending – is a critical spec per ASME B16.49 and ISO 15590:
| Standard | Maximum ovality allowed at bend | Notes |
|---|---|---|
| ASME B16.49 (induction bends for line pipe) | 2.5% to 5% depending on D/t | Tighter for thicker wall |
| ASME B31.3 (process piping) | Project-specific, often 3%-8% | Defined in line class |
| ISO 15590-1 (pipelines) | 2.5% for D/t < 70; up to 5% for higher D/t | Common for transmission |
| EN 13480 (industrial piping) | Defined per project; typically 5% | European plants |
Induction bending typically achieves tighter ovality (1.0%-2.5%) due to the precise, narrow heating band and die geometry. Hot bending tends to be 3%-5% unless the shop uses internal line-up mandrels.
6. When to Specify Induction Bending
Use induction bending when:
- You need a tight radius (≤ 5D) with high repeatability.
- The pipe is small to medium diameter (DN 50 to DN 600).
- You need ASTM A106, A53, API 5L, or ASME-grade compliance for sour or high-temperature service.
- You need consistent ovality for pigging or close-fit liners.
- You have a batch of similar bends, e.g., 40 identical 3D bends for a refinery.
- Documentation requires traceable parameters (heat input, coil position log).
7. When to Specify Hot Bending
Use hot bending when:
- You need a very large radius (10D or more) on large-diameter line pipe (24-48 inches).
- Cost per bend is the primary driver (no expensive induction rig to set up).
- The bend is a one-off or low-volume (e.g., a single 36 in 30D sag bend for a river crossing).
- Pipeline transmission where ASME B31.4 / B31.11 tolerance is acceptable.
- Site bending in the field where power for induction coil is not feasible.
8. Common Standards and Specifications
- ASME B16.49 – Factory-Made Induction Bends for Pipe and Tube.
- ASME B31.3 – Process Piping (covers bend geometry and material).
- ASME B31.4 / B31.11 – Pipeline Transportation Systems.
- ISO 15590-1 – Pipeline Bends.
- EN 13480 – Metallic Industrial Piping.
- EEMUA 159 – Bends and induction bends.
- MSS SP-43 – Stainless steel pipe; sometimes referenced for stainless bends, but the principles apply for carbon.
For line pipe qualifying per API 5L, the bend shop must maintain an ISO 9001 quality program with full traceability from pipe heat to finished bend.
9. Inspection and Testing of Carbon Steel Bends
Standard inspection after bending includes:
- Dimensional: angle, radius, ovality, wall thickness (especially on extrados), leg lengths.
- Visual: surface defects, wrinkles, gouges, surface laps.
- Hydrostatic test: per project code (often 1.5x design pressure).
- Hardness survey: HAZ and parent metal per NACE MR0175 if sour service.
- Mechanical tests: tensile, impact, flattening (for ductility).
- Non-destructive: 100% MT or UT on the bend zone, depending on code.
- Metallurgical exam: when specified, microstructural review of HAZ.
10. Cost Comparison
Indicative cost split per bend (DN 300, SCH 40, ASTM A106 Gr.B, 3D, 90 degrees):
| Item | Induction Bending (USD per bend) | Hot Bending (USD per bend) |
|---|---|---|
| Setup / tooling | 300-600 | 100-200 |
| Energy | 150-250 | 60-120 |
| Labor | 200-350 | 350-500 (more manual) |
| Inspection / NDE | 200-300 | 200-300 |
| Total typical | 1,000-1,500 | 800-1,200 |
Induction bending has higher setup cost but lower labor cost per bend as volume scales. Hot bending is cheaper for single bends or large radius.
11. Selecting a Bending Shop
When vetting a carbon steel bending supplier:
- Look for OEM experience on similar pipe size, grade, and radius.
- Confirm the coil or burner is properly sized for your pipe OD and wall.
- Ask for a sample bend report with ovality, hardness map, and NDE coverage.
- Check that NDE technicians hold current ASNT or EN 473 certification.
- Verify the shop has a documented welding procedure (if back-end beveling is needed).
- Ask about documentation: EN 10204 3.1 MTC, dimensional report, ovality %.
12. Frequently Asked Questions
Q1: Can induction bending crack the pipe?
On properly heated material at the recommended temperature, no. If the pipe is cold or overheated, surface cracks can form on the extrados. Use a pyrometer and verify mill condition before bending.
Q2: Is hot bending acceptable for sour service?
It depends on the project specification. NACE MR0175 / ISO 15156 restricts hot forming above certain temperatures without re-heat-treatment. Many sour-service projects require induction bending for tighter process control.
Q3: Which is faster?
Induction bending is faster for small to medium diameter, producing typical 90 deg bends in 5-15 minutes once the rig is set up. Hot bending takes 30-90 minutes for the same bend due to operator handling.
Q3: Can both methods produce a 3D bend?
Yes. Induction handles 3D more routinely; hot bending can produce 3D but ovality tends to increase. For D/t > 100, expect ovality closer to 5-8% with hot bending without internal mandrel.
Q4: Do I need to re-normalize after bending?
Only if the specification requires it. Many carbon steel lines accept bend zone in as-bent condition for normalized pipe grades. Check with the engineer of record.
Q5: How does bend differ from a standard elbow?
A bend is a continuous sweep without an abrupt tangent point. An elbow (long or short radius) is a factory-formed fitting with multiple segments welded together. A bend generally has lower pressure drop and fewer welds.
Q6: What is the maximum angle for one bend?
In theory up to 180 degrees in a single pass. Common production range is 30-180 degrees. Compound bends (3D rotation) are also possible with both methods.
13. Conclusion
Induction bending is the modern, repeatable, tight-radius choice for carbon steel pipe in process and pipeline service. Hot bending remains relevant for large-diameter, large-radius, lower-cost bends. Choose based on pipe size, batch volume, accuracy needs, and applicable codes. For critical service – sour, high-temperature, or tight-radius – induction bending is the safer pick. For large pipeline sag bends and field work, hot bending is still standard practice.
Huaxia-Steel partners with certified Chinese bending shops to deliver induction and hot bends in ASTM A106, A53, API 5L X42-X80, and ASME B16.9 material grades. Send us your bend geometry, material grade, and quantity for a quote.
Related Images