When a buyer asks us to prepare carbon steel for export — particularly stainless-replacement parts, hot-rolled sheet that will sit in inventory, or precision components that need a clean base before further coating — the next question almost always is the same: should we pickle and passivate, or should we phosphate? Both are pre-treatment chemistries, both run at modest line temperatures, and both live in the conversation between “as-rolled mill scale” and “ready for paint”. But the chemistries, the equipment footprint, the protection level, and the unit cost are different enough that they cannot be substituted without a specification update. This article lines the two up so your QA plan, your coating supplier, and your end customer all reference the same procedure.
What Each Process Actually Does on Steel
Pickling and passivation
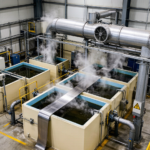
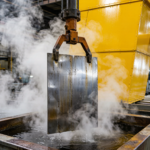
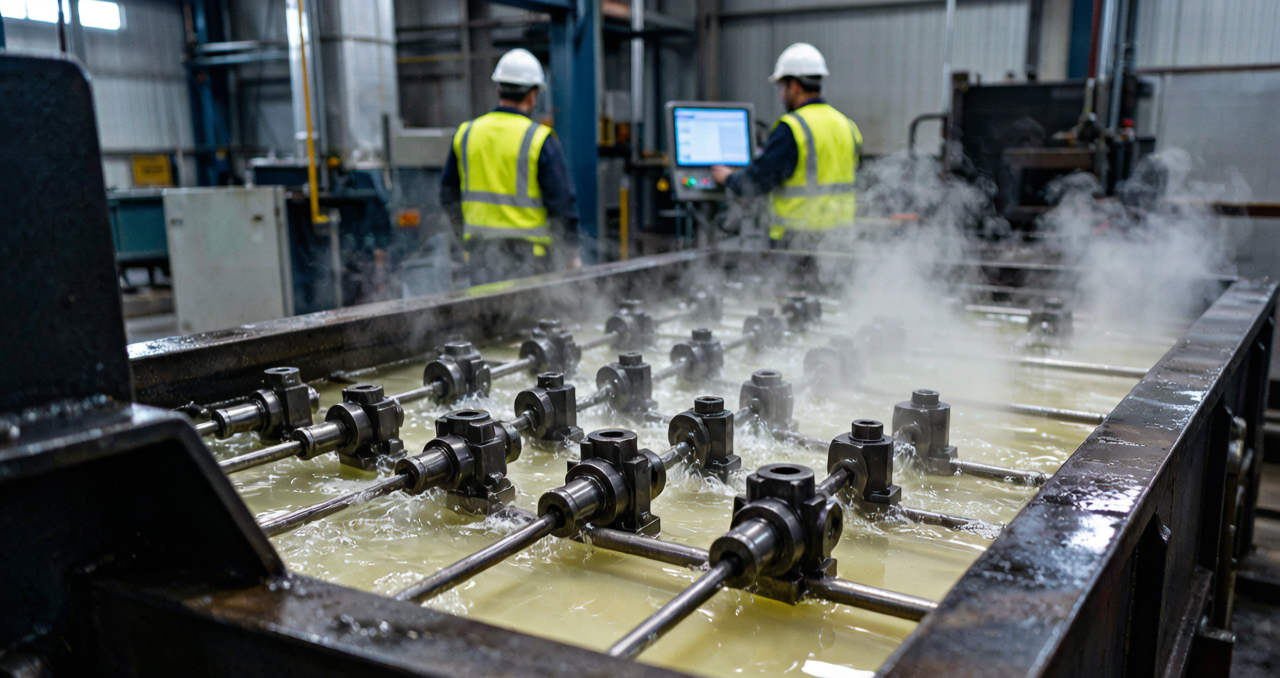
Pickling is an acid bath, typically hydrochloric (HCl) or sulfuric (H2SO4), that removes mill scale, rust, welding discoloration, and the heat-affected tint you see next to weld beads. The bath temperature sits between 40 and 80 deg C for HCl or 60 to 90 deg C for H2SO4; immersion time runs 5 to 30 minutes depending on scale thickness. After pickling the part is rinsed, then moved into a passivation step — most commonly a nitric acid bath (HNO3 20-50 %) or a citric acid bath (4-10 %) for stainless grades, where a thin, dense, chromium-enriched oxide layer is rebuilt on the surface.
The combined pickling-and-passivation cycle is the standard surface preparation for austenitic stainless steel under ASTM A380 and ASTM A967. It also sees regular use on carbon steel when the buyer wants a chemically clean, scale-free surface that can be oiled, painted, plated, or welded without contamination carry-over.
Phosphating (conversion coating)
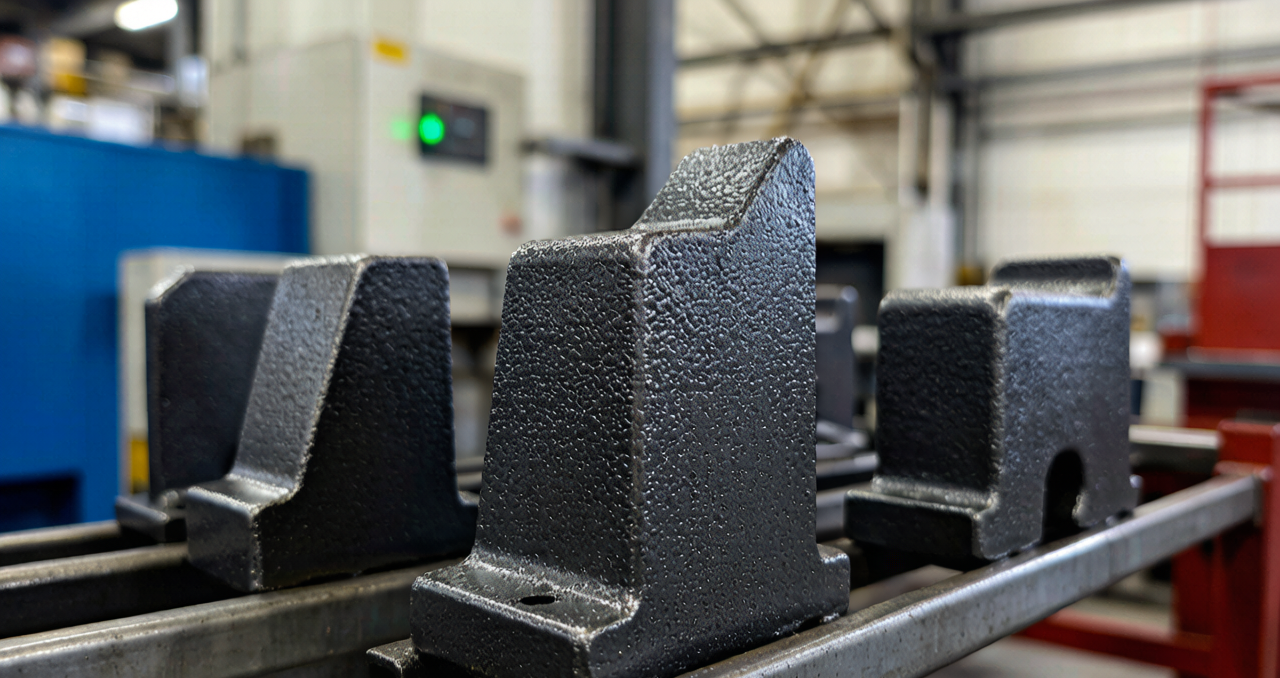
Phosphating is an acidic phosphate bath — zinc phosphate, manganese phosphate, or iron phosphate — that does not remove scale; it converts the metal surface into a crystalline phosphate layer tightly bonded to the substrate. Crystal weight gain is typically 5 to 25 g per square meter. The bath runs at 50 to 95 deg C, with immersion time of 5 to 30 minutes. A final rinse and a seal/dry step follow, often with a topcoat of oil or a corrosion-preventive fluid (RP).
Phosphating is the dominant pre-treatment for carbon steel parts that will subsequently be powder-coated, liquid-painted, or assembled with an oiled anti-rust film. The automotive, appliance, fastener, and construction-hardware industries run phosphating lines by default for this reason.
Process Comparison Table
| Attribute | Pickling + Passivation | Phosphating (Zn/Mn/Fe) |
|---|---|---|
| Main chemistry | HCl or H2SO4, then HNO3 or citric acid | Zinc phosphate, manganese phosphate, iron phosphate |
| Surface effect | Removes scale and oxide; rebuilds a passive oxide layer (stainless) | Replaces the surface with a crystalline phosphate layer (carbon steel) |
| Applicable substrate | Stainless steel primarily; carbon steel when scale removal is the goal | Carbon steel and low-alloy steel by default; not used on stainless |
| Bath temperature | 40-90 deg C | 50-95 deg C |
| Immersion time | 5-30 min pickling; 10-30 min passivation | 5-30 min phosphating; rinse + sealing follow |
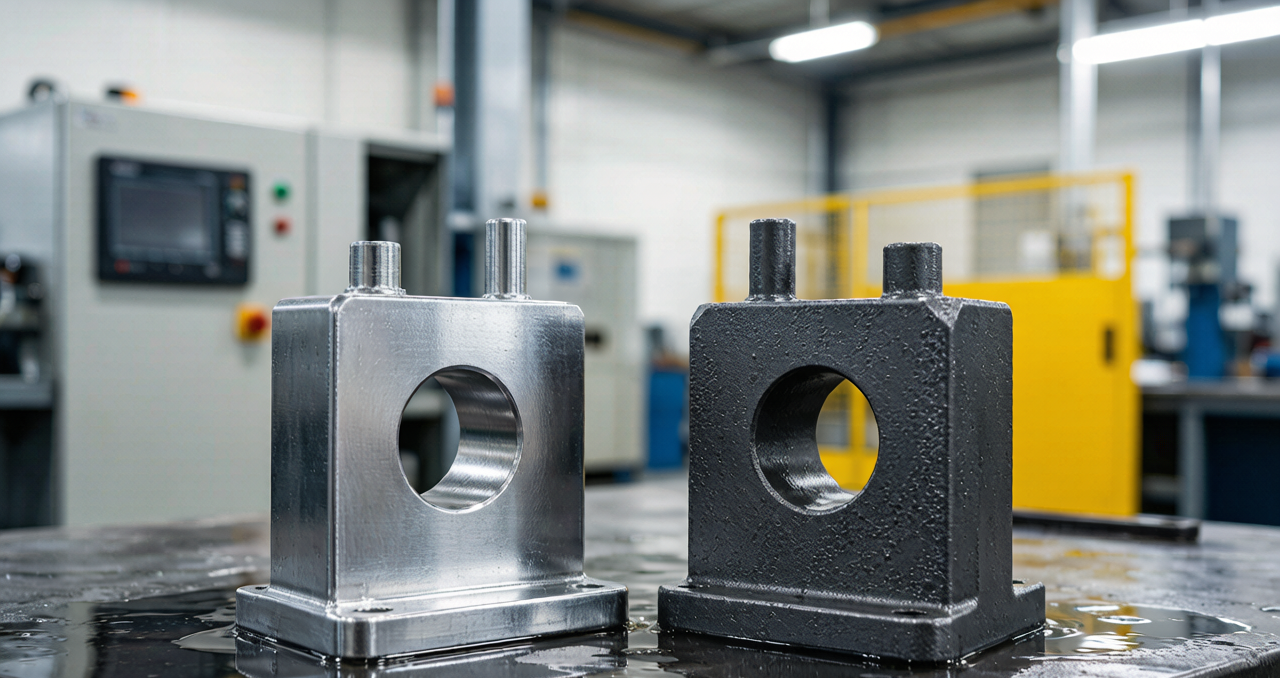
| Surface appearance after treatment | Clean metallic silver/grey; no visible film | Grey crystalline matte; slightly rougher; visible film weight gain |
| Coating weight | None (passive film) | 5-25 g/m2 |
| Corrosion protection (NSS / neutral salt spray) | Low for carbon steel (<24 h, often <8 h without oil); 200+ h for stainless | Improved over bare steel; oil or topcoat adds 24-96 h for carbon steel |
| Paint adhesion | Good when the surface is immediately coated; does not anchor paint by itself | Excellent — the crystalline phosphate structure is the paint anchor of choice for liquid and powder lines |
| Lubricity | None | Particularly with manganese phosphate, very good cold-forming lubricant carrier |
| Effluent handling | Acid neutralization, metal hydroxide sludge | Phosphate sludge, nitrate/nitrite control, pH tuning |
| CapEx / OpEx | Higher acid cost, lower energy; tanks in PP or rubber-lined steel | Lower chemistry cost per m2; heating energy dominates; sludge removal cost |
| Standards commonly referenced | ASTM A380, ASTM A967, ISO 21469 (stainless) | GB/T 6807, DIN 50942, MIL-DTL-16232 (Mn phosphate), ISO 9717 |
Where Pickling + Passivation Wins
Pickling wins when the goal is scale and oxide removal rather than coating buildup. Use it when:
- The steel is austenitic stainless (304, 304L, 316, 316L, 321, 347) and the order specifies ASTM A380 / A967.
- The carbon steel part has heavy mill scale from hot rolling that the next operation (welding, plating, nitriding) cannot tolerate.
- The buyer requires a chemically clean, scale-free, oxide-free surface — for example, before EN 10204 3.2 witnessed hydrostatic testing, before pickling-and-oiling of plate per ASTM A604, or before electroplating.
- The component will live in a controlled environment for a short cycle, with a separately supplied corrosion inhibitor.
Pickling is also the step of choice after heat treatment. Heat tint and oxide scale from the furnace cut into corrosion resistance; pickle removes both, and the passivation step rebuilds the protective layer.
Where Phosphating Wins
Phosphating wins when the part will be painted, coated, or assembled with a corrosion-preventive oil and the bond strength or holding power matters. Use it when:
- The carbon steel part is destined for powder coating or wet paint — the crystalline layer dramatically improves adhesion and salt-spray performance.
- The part is a fastener, screw, or threaded rod — manganese phosphate carries oil and acts as a cold-heading lubricant.
- The buyer asks for a 24 to 96 hour NSS rating without a topcoat — a Mn- or Zn-phosphate plus oil gives that band consistently.
- The end use is cold forming, deep drawing, or extrusion — phosphate plus soap/lubricant is the standard shop practice.
- The component is subject to sliding wear — Mn phosphate has good anti-galling behavior.
For fastener lines and small-batch production of brackets, hinges, brackets, and structural fittings, zinc phosphate plus a dry-in-place oil is the default recipe.
Hybrid Routes You Will Sometimes See
For demanding service environments, the two are often combined:
- Pickle + zinc phosphate + epoxy primer: common in marine-grade structural steel. The pickle removes scale, the phosphate layer anchors the primer.
- Pickle + manganese phosphate + oil: typical for fasteners and cold-formed parts that need both a clean substrate and a lubricious surface.
- Pickle + iron phosphate + paint: an older sequence still in use in appliance cabinets and white-goods OEM lines.
If your drawing calls for both, expect the supplier to ask which is the primary surface preparation and what is the secondary, because the MTC language differs between them.
Cost and Cycle Considerations
For a hypothetical 1 ton batch of small carbon steel parts, ballpark processing time and cost split roughly as follows:
| Process | Cycle time per batch | Chemistry cost per ton | CapEx footprint |
|---|---|---|---|
| Pickle + passivate (HCl then HNO3) | 45-90 min | USD 30-60 | Medium; acid-resistant tanks + scrubber |
| Zinc phosphate + rinse + seal | 30-60 min | USD 20-50 | Medium; heated tanks + sludge filter |
| Manganese phosphate + oil | 45-75 min | USD 25-55 | Medium; heated tanks + oil dip |
| Combined pickle + zinc phosphate | 60-120 min | USD 50-100 | Medium-high; multi-stage line |
Operational discipline matters more than which of the two you pick. Bath temperature drift, pH creep, iron loading in the phosphating tank, and rinse-water TDS all degrade the result faster than a process change does.
Quality Control Tests for Both
Pickling quality is checked by visual inspection (scale removal completeness), water-break test (cleanliness), and — for stainless — the copper-sulfate test or the ferroxyl test for free iron on the surface. Phosphating quality is checked by coating weight (gravimetric), crystal morphology (SEM or optical at 200x), salt-spray performance (ASTM B117), and adhesion (cross-hatch ASTM D3359 tape test) if a topcoat is applied.
A buyer spec that names both must also specify acceptance criteria. Otherwise the QA plan defaults to “no visible scale” and “color is uniform”, which is subjective.
Frequently Asked Questions
Can pickling and passivation be applied to carbon steel?
Pickling yes; passivation in the strict ASTM A967 sense is intended for stainless. On carbon steel, pickling produces a clean scale-free surface that can be oiled or coated, but it does not generate a true passive layer the way it does on stainless. The phrase “pickling and passivation” on a carbon steel drawing should be read as pickling only, with a separate corrosion-preventive step if needed.
Is zinc phosphate or manganese phosphate better for fasteners?
Manganese phosphate. It has superior oil retention and performs better under sliding contact. Zinc phosphate is the standard for body panels and hardware that will be painted.
How long does the protection last in storage?
Pickled carbon steel with no topcoat: 1-3 days in humid storage before surface rust reappears. Zinc phosphate alone: 2-4 weeks. Zinc phosphate plus oil: 3-12 months. Manganese phosphate plus oil: 6-24 months depending on storage environment.
Which process is more environmentally regulated?
Both generate effluent that needs treatment. Phosphating produces phosphate-laden wastewater subject to discharge consent limits; pickling produces acidic rinse water with dissolved metals. In practice, phosphating is the more tightly regulated of the two in many jurisdictions because of phosphorus discharge caps.
Can I do both on the same line?
Yes, but you need dedicated tanks for acid vs. phosphate to avoid cross-contamination. Most commercial finishers run a multi-stage line with separate pre-rinse, pickle, rinse, phosphate, rinse, and seal tanks; they charge accordingly.
How to Specify on Your RFQ
State the substrate, the target process, the standard to follow, the coating weight or film weight expectation, and any acceptance test you want reported. Examples:
- “Carbon steel plate, hot-rolled, ASTM A36, pickled in HCl then water-rinsed, oiled with RP-1, per ASTM A604. MTC to EN 10204 3.1.”
- “Carbon steel fastener grade 8.8, manganese phosphate per MIL-DTL-16232, Grade 4, Class 1, with rust-preventive oil.”
- “Carbon steel sheet for cold forming, zinc phosphate 8-12 g/m2 coating weight, soap-lubricant overcoat, sample salt spray 48 h per ASTM B117, no red rust.”
Request a Quotation
Send your part drawing, batch size, the standard you need to meet, and any paint or oil specification downstream to [email protected]. We will return a process-route quote covering pickle, zinc phosphate, manganese phosphate, or a combined sequence, plus the QA test plan and sample MTC.
Browse Huaxia-Steel for more surface-treatment guidance, coating options, and mill-direct pricing on treated carbon steel plate, sheet, and bar stock.
Related Images