Roll Forming vs Press Brake Bending: Carbon Steel Process Comparison
When a carbon steel coil or sheet needs to become a channel, angle, rail or complex profile, two processes dominate the factory floor: roll forming and press brake bending. Both shape metal without melting, but their tooling economics, tolerance profiles and production speeds differ dramatically. This comparison of roll forming vs press brake bending for carbon steel helps sourcing managers and design engineers pick the right process for volume, precision and budget.
1. How Roll Forming Works
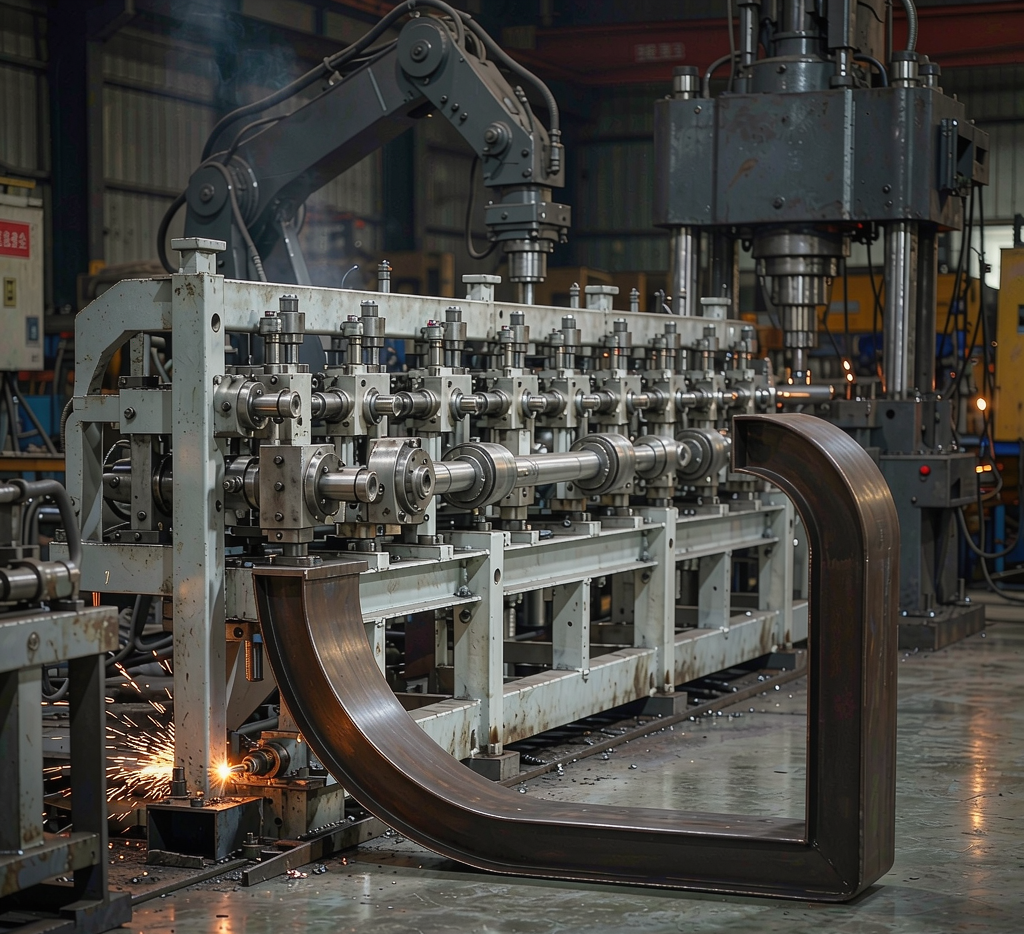
Roll forming feeds a continuous strip of carbon steel through a series of hardened rollers, each set performing a small incremental bend. By the time the strip exits the final stand, it has assumed the desired cross-section—whether a simple C-channel, a complex hat section or a perforated solar rail.
Input material: hot-rolled coil, cold-rolled coil, pickled and oiled strip, pre-painted coil or galvanized coil
Typical thickness range: 0.5 mm to 6.0 mm for carbon steel
Line speed: 10 to 100 metres per minute depending on complexity
Cut-off method: flying shear or rotary punch at line speed
Because the process is continuous, roll forming excels at high volumes of uniform profiles. Once the roll tooling is proven, labour content per metre is minimal.
2. How Press Brake Bending Works
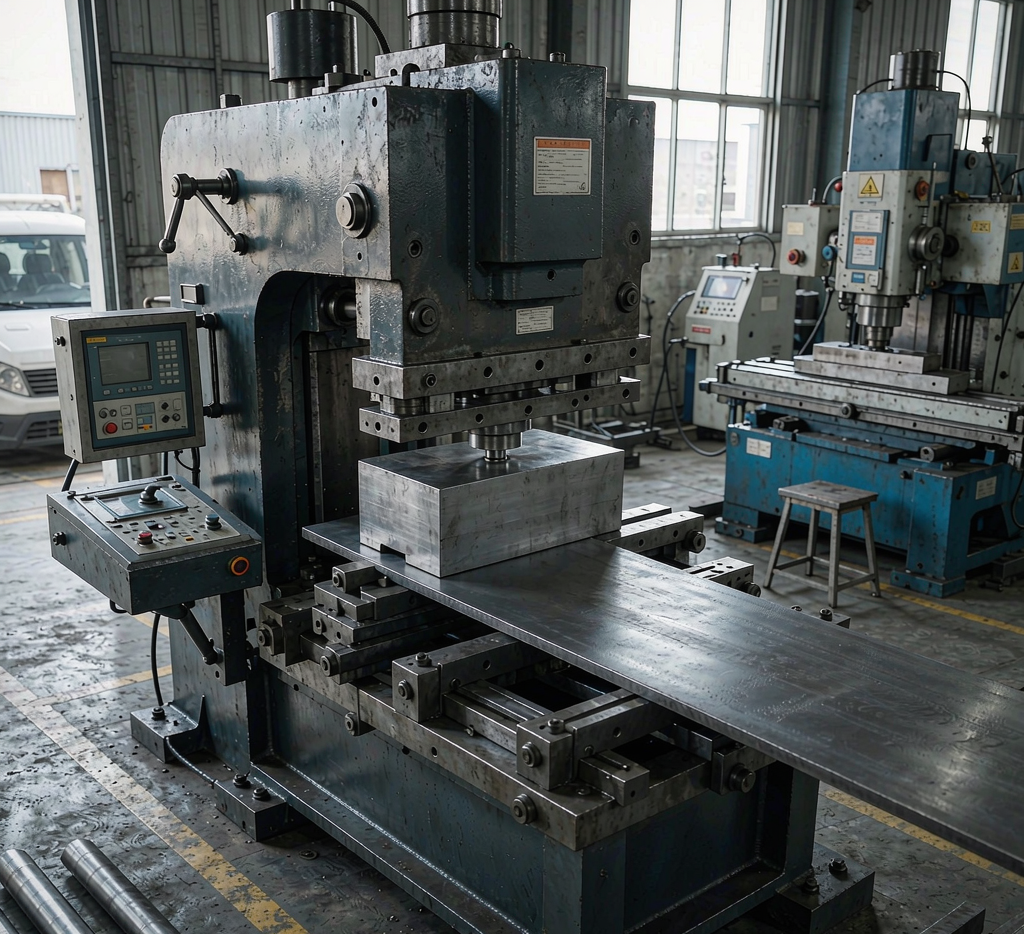
A press brake uses a vertically moving punch and a stationary V-die to create a single bend in a flat blank. Multiple bends—whether in sequence on one machine or distributed across several brakes—produce the final geometry.
Input material: flat blanks, laser-cut or sheared plates
Typical thickness range: 0.5 mm to 25 mm+ for carbon steel
Bend length capacity: up to 8 metres on large CNC brakes
Tool change time: minutes, not weeks
Press brake bending is inherently a batch or job-shop process. It shines when part variety is high, volumes are low to medium, and thick plate must be formed.
3. Process Comparison at a Glance
Factor
Roll Forming
Press Brake Bending
Best volume
High (≥ 5,000 m or pieces/year)
Low to medium (≤ 5,000 pieces/year)
Tooling cost
High upfront ($5,000 – $80,000+)
Low upfront (standard dies)
Per-piece labour
Very low
Moderate to high
Material thickness
0.5 – 6.0 mm typical
0.5 – 25 mm+ typical
Part length
Continuous, cut to any length
Limited by bed size
Cross-section complexity
Excellent (closed profiles possible)
Limited to open bends
Tolerance (typical angle)
± 1.0°
± 0.5° with CNC crowning
Surface marking
Minimal roller polish
Die witness marks possible
Setup changeover
Hours to days
Minutes
Nesting waste
Near zero (coil fed)
Blank skeleton waste
4. Tolerance and Repeatability
For carbon steel thin strip, roll forming holds linear dimensions within ± 0.3 mm and angle within ± 1.0° once the line is warmed up. Springback is managed by over-bending in the final roll stands.
Modern CNC press brakes with real-time angle monitoring and hydraulic crowning can hold angle within ± 0.3° and bend position within ± 0.1 mm per 1,000 mm. For low-volume prototype work or thick plate where roll tooling cannot be justified, the press brake wins on precision.
5. Material Behaviour and Springback
Carbon steel with higher yield strength (Q235, S355, A572 Gr. 50) exhibits more springback than low-strength grades (Q195, A283 Gr. C). Both processes must compensate:
Roll forming: final pass rollers are set to an over-bend angle; strip tension between stands helps stabilize the profile
Because roll forming distributes strain over many stands, it handles high-strength carbon steel with less risk of edge cracking than a single aggressive brake bend.
6. Cost Economics: When to Choose Which
Choose Roll Forming When:
Annual volume exceeds 5,000 metres or 10,000 pieces
The profile is constant or changes only in length
Material thickness is 6 mm or less
You need a closed or semi-closed hollow section
Surface finish must be free of die witness lines
Choose Press Brake Bending When:
Annual volume is low or sporadic
Part geometry changes frequently (job-shop environment)
Plate thickness exceeds 6 mm
Prototype or first-article development is required
Tight angular tolerance (< ± 0.5°) is mandatory
7. Typical Carbon Steel Products by Process
Roll Forming Products
Press Brake Products
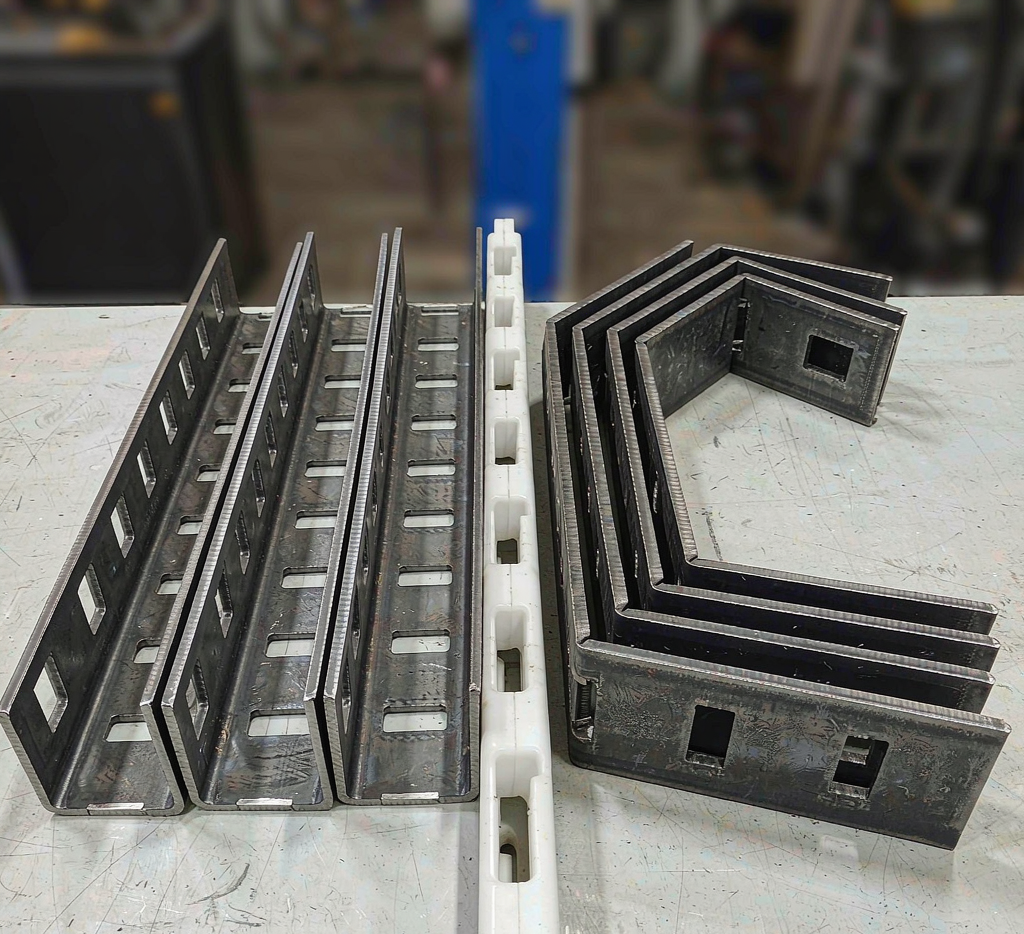
C and Z purlins
Electrical enclosures
Door and window frames
Heavy equipment guards
Solar panel mounting rails
Truck trailer side panels
Storage rack uprights
Ship bulkhead stiffeners
Automotive bumper reinforcements
Bridge girder web plates
HVAC duct flanges
Pressure vessel shells
8. Quality Control and Inspection Points
Regardless of process, buyers should specify inspection criteria on the purchase order:
Dimensional report: profile width, leg length, bend radius, hole position (if pre-punched)
Angle check: go/no-go gauge or digital protractor on first-off and hourly samples
Surface: no scratches deeper than 5% of thickness, no roller slippage marks on cosmetic faces
Flatness: bow and twist per EN 10051 or agreed A6 tolerance for brake-bent plate
MTC review: confirm yield strength matches the springback compensation used by the supplier
FAQ
Can roll forming handle pre-galvanized carbon steel?
Yes, and it is the preferred process for pre-galvanized strip because the gradual bending action preserves the zinc coating better than the sharp pinch of a brake die. Specify GI or GA coil with appropriate zinc weight (Z120 – Z275).
What is the minimum bend radius for press brake bending Q235B?
As a rule of thumb, inside bend radius should be at least 1× material thickness for grain-direction bends and 1.5× for cross-grain bends. Thicker plate or higher-strength grades require larger radii to avoid outer-fibre cracking.
Does roll forming work for carbon steel thicker than 6 mm?
Special heavy-duty roll lines can form up to 12 mm, but tooling cost and motor power rise sharply. Above 6 mm, press brake or profile bending machines are usually more economical unless volumes are extremely high.
Which process produces less scrap?
Roll forming generates minimal scrap because coil is fed continuously. Press brake bending requires individual blanks, leaving skeleton waste. For expensive alloys or coated strip, the roll forming scrap advantage can be decisive.
Can holes and slots be added in-line during roll forming?
Yes. Pre-punching stations or rotary punching units can create holes, slots, embossments and notches at precise spacing while the strip moves. This integration eliminates secondary operations and improves positional accuracy.
Conclusion
Roll forming and press brake bending are complementary rather than competing technologies in carbon steel fabrication. Roll forming delivers unbeatable unit economics for long runs of thin, uniform profiles. Press brake bending offers flexibility, thick-plate capacity and rapid changeover for diverse, low-volume work. By mapping your annual volume, thickness range and tolerance needs against the comparison above, you can specify the right process—and the right supplier—before releasing the RFQ.
Looking for a carbon steel roll forming or press brake bending partner in China? Huaxia-Steel supplies precision-formed carbon steel sections, brackets and panels to ASTM, EN and JIS specifications with full MTC documentation.
If you require further information about our metal sheet products or architectural projects, please don’t hesitate to leave your contact details and message here.
Our team of experts will respond within 24 hours to continue the discussion and provide you with any additional information you requires.