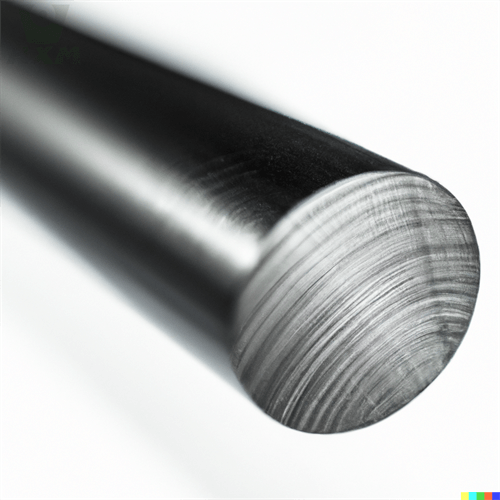
65Mn spring steel round bar is China’s most widely used high-carbon spring steel for shafts, spring components, agricultural blades and wear parts: a manganese-silicon grade to GB/T 1222 with 0.62–0.70% carbon, hardened to 40–50 HRC and combining high yield strength with good fatigue resistance at a fraction of alloy steel cost. Export buyers use 65Mn round bar wherever a part needs more strength than 1045 can deliver but does not justify 5160 or 6150 alloy pricing — from clutch components and U-bolts to mower blades and harrow discs. Huaxia-Steel supplies 65Mn round bar from audited partner mills in hot rolled, hot rolled bright and cold drawn conditions, with EN 10204 3.1 certificates, spheroidize-annealed options for machining, and cut-to-length service.
Product Overview
65Mn is a high-carbon manganese spring steel. The carbon (0.62–0.70%) provides the martensite hardness ceiling after quenching, while manganese (0.90–1.20%) improves hardenability so even moderate-size sections quench through in oil. The grade is supplied in four commercial conditions: hot rolled (as-rolled, mill scale), hot rolled and descaled, spheroidize annealed (best machinability, hardness ≤ 229 HB per the standard) and cold drawn (tighter tolerance, higher as-supplied strength). After machining or forming, parts are quenched in oil from 780–830 °C and tempered at 350–500 °C to reach working hardness of 40–48 HRC with adequate toughness. Unlike true Si-Mn spring steels such as 60Si2Mn, 65Mn trades some elastic limit for easier heat treatment and lower cost — the reason it dominates the mid-market.
- Standard: GB/T 1222 (spring steel); near equivalents: AISI 1566, C67S/CK67 (DIN 17222), SUJ-adjacent Mn grades.
- Supply conditions: hot rolled, annealed (≤ 229 HB), cold drawn, quenched-and-tempered on request.
- Diameter range: 8–120 mm hot rolled; 2–60 mm cold drawn with h9–h11 tolerance.
- Certificates: EN 10204 3.1 with chemistry, hardness, and decarburization depth.
Specifications: Dimensions, Weight and Tolerance
| Parameter | Hot rolled | Cold drawn |
|---|---|---|
| Diameter range | 8–120 mm | 2–60 mm |
| Diameter tolerance | ±0.4–1.0 mm (per GB/T 702) | h9 / h10 / h11 (per GB/T 1803) |
| Standard lengths | 6000 mm (3000–9000 on request) | 3000–6000 mm, cut-to-length ±2 mm |
| Weight per meter | W = 0.00617 × d² kg/m (d in mm): Ø20 = 2.47 kg/m, Ø50 = 15.4 kg/m | |
| Straightness | ≤ 3 mm/m | ≤ 1 mm/m |
| Surface | Mill scale / descaled | Bright, oiled |
| Out-of-roundness | Within diameter tolerance | ≤ 50% of diameter tolerance |
Chemical Composition (GB/T 1222)
| Element | Content |
|---|---|
| Carbon (C) | 0.62–0.70% |
| Manganese (Mn) | 0.90–1.20% |
| Silicon (Si) | 0.17–0.37% |
| Chromium (Cr) | ≤ 0.25% |
| Sulfur (S) | ≤ 0.030% |
| Phosphorus (P) | ≤ 0.030% |
| Nickel (Ni) | ≤ 0.25% |
Mechanical Properties and Heat Treatment
| Condition | Tensile (MPa) | Yield (MPa) | Hardness |
|---|---|---|---|
| Hot rolled (as-rolled) | ≥ 980 | — | ≤ 285 HB |
| Annealed | ≥ 735 | — | ≤ 229 HB |
| Quenched + tempered (sample) | ≥ 1225 | ≥ 980 | 40–48 HRC typical |
| Cold drawn | 1000–1200 typical | — | ≤ 30 HRC typical |
Recommended heat treatment for spring and wear parts: austenitize 780–830 °C, quench in oil (water quenching risks cracking in thin sections), temper 350–500 °C and air cool. Tempering below 250 °C raises hardness toward 55 HRC but leaves insufficient toughness for impact service — for blades and spring washers, stay in the 400–460 °C window. Total decarburization depth on hot rolled bar is limited to 1.0–1.5% of diameter per GB/T 1222; for parts machined all over this is irrelevant, but for bars used as-rolled in spring service, confirm the decarburization value on the certificate.
Manufacturing Standards
- Governing standard: GB/T 1222 (chemistry, hardness, decarburization); bar dimensions to GB/T 702 (hot rolled) and GB/T 3078/3207 (cold drawn).
- Production route: EAF or BOF melting, continuous casting, rolling; annealing in covered pits or continuous furnaces for spheroidized structure.
- Testing per heat/lot: chemistry, tensile, hardness, decarburization, macrostructure (low-power etch) and non-metallic inclusion rating available on request.
- Traceability: heat number on each bundle tag, matching the EN 10204 3.1 certificate.
- Equivalent supply also offered against AISI 1566 / C67S on request, with certificate showing the ordered designation.
Typical Applications
- Agricultural blades: mower knives, harrow discs, tiller tines, rotary blades.
- Spring components: flat springs, spring washers, U-bolts, leaf spring parts.
- Shafts and rollers requiring 40–48 HRC surface hardness after heat treatment.
- Hand tools: scrapers, chisels, garden tool heads.
- Wear parts: guide rails, wear strips, chain pins for medium-abrasion service.
Selection note versus neighbors: choose 65Mn over 1045 when the part is quenched and tempered for hardness above 40 HRC or sees fatigue loading; choose 60Si2Mn over 65Mn when elastic limit and sag resistance at thickness above ~10 mm matter (leaf springs, heavy coil springs); choose 4140/42CrMo when the part needs core strength plus toughness beyond what plain high-carbon steel delivers, or operates above 200 °C.
Quality Assurance and Inspection
Standard QA package: EN 10204 3.1 certificate per heat, hardness test on representative bars, decarburization measurement on hot rolled sizes, and bundle-level traceability. Optional services include spectrometer check at our warehouse before shipment, third-party inspection (SGS/BV/TUV), macro-etch and inclusion rating for fatigue-critical parts, and hardness profiling after your specified Q&T cycle — send us your heat treatment parameters and we will run test coupons and report results before the batch ships. Machinability data and recommended cutting parameters for the annealed condition are available on request for customers running CNC lathes.
Packing and Shipping
Bars are bundled at 1–2 t with steel strapping, end-capped for cold drawn bright bar, and packed in seaworthy export bundles or wooden cases for small-diameter cold drawn stock. VCI paper and plastic wrap protect bright surfaces in ocean transit; each bundle carries heat number, size, grade and net weight tags matching the packing list. Standard lengths of 6 m load efficiently: a 20 ft container takes roughly 25 t of straight-length bar. Documents: invoice, packing list, 3.1 certificates, COO and fumigation-free packing declaration where required.
Surface Condition and Defect Limits
65Mn round bar is supplied with surface condition governed by GB/T 1222 and the applicable bar standard: hot rolled bar may carry mill scale and scattered shallow marks, while cold drawn bar is supplied bright and oiled with no visible laps or seams. For spring applications the surface matters more than appearance suggests — surface decarburization and seams are the two most common origins of fatigue cracks in heat treated parts. Two practical controls: order annealed bar and machine 0.5–1.0 mm off the diameter when the part is fatigue-loaded, and specify a seam-depth limit (commonly 0.2 mm or 1% of diameter) on the PO for hot rolled material used in spring service. Optional eddy current or magnetic inspection of bar surface is available for high-cycle components; ask for it with your order if the part sees repeated loading.
Machining and Heat Treatment Guidance
Machine 65Mn in the annealed condition whenever the part geometry allows it: spheroidized structure at ≤ 229 HB gives predictable tool life with carbide inserts at 120–180 m/min, whereas hot rolled bar at up to 285 HB roughly doubles tool wear and raises cutting forces. Where the bar is used as-rolled and heat treated after forming, expect scale on the surface — plan a shot blast or grinding step before quenching so the quench is uniform and the final hardness is consistent.
- Recommended Q&T: austenitize 780–830 °C, oil quench, temper 350–500 °C; target 40–48 HRC for spring and wear parts.
- Avoid water quenching on sections above about 12 mm — 65Mn’s manganese raises hardenability enough that oil works, and water invites quench cracking on sharp section changes.
- Temper promptly after quenching (within 2–4 hours) to avoid delayed cracking; high-carbon martensite is unforgiving.
- Spring service: after Q&T, a light shot peening step raises fatigue life measurably on leaf-type components.
- Decarburization: for parts used as-rolled in spring service, confirm the certified decarburization depth; machining allowance of 0.5–1.0 mm per side removes it entirely for machined parts.
- Welding is not recommended — 0.62–0.70% carbon requires preheat and post-heat procedures, and the HAZ will crack without them.
When volumes justify it, we also supply 65Mn flat bar and strip coil from the same heats, so customers producing both blade blanks and spring washers can consolidate certification and freight in one shipment — ask about mixed-size consolidation when you request a quotation.
Ordering Checklist
- Grade and standard: 65Mn to GB/T 1222; state if AISI 1566 or C67S documentation is required.
- Diameter and tolerance: hot rolled per GB/T 702, cold drawn h9/h10/h11 per GB/T 1803.
- Condition: hot rolled, annealed (machining), cold drawn, or Q&T to your specified cycle.
- Length: standard 6000 mm or cut-to-length with ±2 mm; state chuck length if for automatics.
- Testing: chemistry and hardness standard; decarburization, macro-etch and inclusion rating on request.
- Certification: EN 10204 3.1 with heat number per bundle.
- Surface and packing: oiled, VCI-wrapped, end-capped for cold drawn.
- Commercial: Incoterm, port, validity, payment terms, lead time, LD clause and rejection remedy.
Why Buy 65Mn From Huaxia-Steel
- Factory-direct supply from audited spring steel mills, one certificate chain per heat.
- Both annealed (machining) and hot rolled (direct Q&T) conditions in stock and to order.
- Cut-to-length with ±2 mm accuracy; small trial quantities accepted alongside bulk orders.
- EN 10204 3.1 certificates with hardness and decarburization data as standard.
- Quotation within 24 hours, FOB/CIF/DDP flexible terms.
Send your diameter, tolerance class, condition and quantity for a same-day quotation — or request a small sample bundle with certificate to run your heat treatment trials before committing production volume.