Carbon Steel Forged Ring — Factory Direct Supplier | Huaxia-Steel
Huaxia-Steel manufactures open-die and rolled carbon steel forged rings from 300 mm to 5,000 mm outside diameter, in weights from 20 kg to 25 t per ring, in grades C45, 1045, 1050, AISI 4140, 4340, S355J2, and Q345B/Q355D. Every ring is forged with a controlled reduction ratio of 3:1 or better, heat treated to your hardness class, UT inspected per ASTM A388, and certified to EN 10204 3.1 (3.2 on request). One factory, one quality system — from ingot to machined, finish-dimensioned ring.
Product Overview
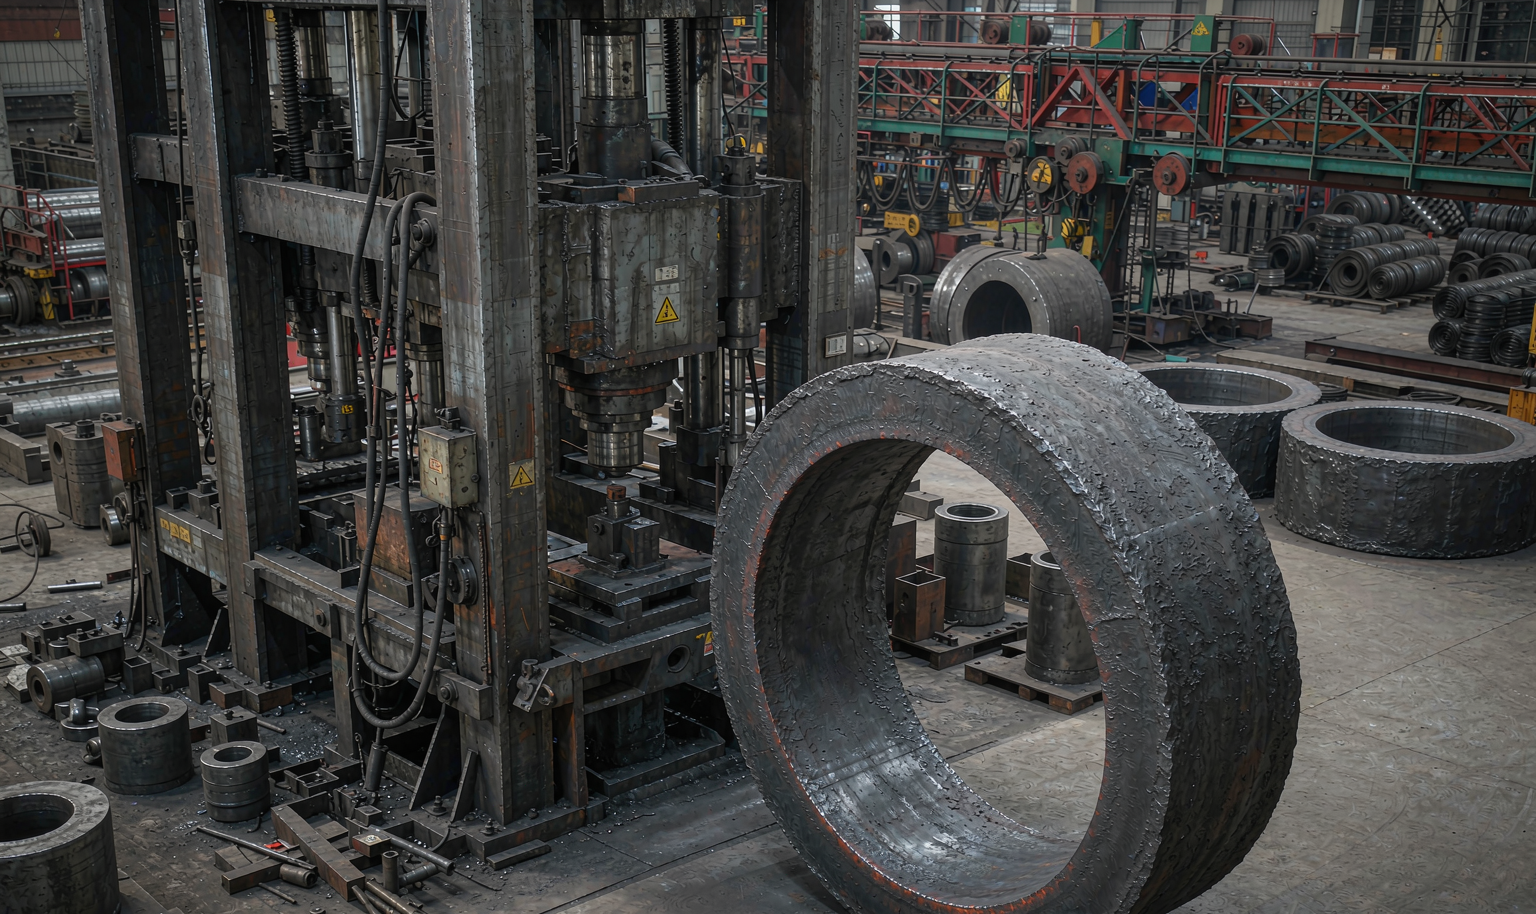
Forged rings are the backbone of rotating and pressure equipment: flanges, bearing housings, gear blanks, pressure vessel shells, slewing rings, and pipe-support collars all start life as a forged ring. Forging breaks the cast structure, closes porosity, and aligns the grain flow circumferentially — giving tangential strength and fatigue life that rolled plate and centrifugal castings cannot match. We produce by two routes: rolled ring forging (mandrel mill) for diameters up to 5,000 mm with tight tolerance and minimal machining stock, and open-die forging for heavy, irregular, or small-lot rings. Supply condition: as-forged, normalized, Q&T, or fully machined to your drawing.
Size Range & Tolerances
| Parameter | Rolled Rings | Open-Die Rings |
|---|---|---|
| OD range | 300–5,000 mm | 300–3,500 mm |
| Wall (radial) thickness | 30–500 mm | 50–600 mm |
| Height (axial) | 30–1,000 mm | 60–1,200 mm |
| Max weight | 12 t | 25 t |
| Machining stock (as-forged) | 5–15 mm per side | 15–40 mm per side |
| Machined tolerance | ISO 2768-m (h9 on request) | ISO 2768-m |
| Roundness (machined) | ≤0.5 mm at 2,000 mm OD | ≤1.0 mm at 2,000 mm OD |
Steel Grades & Heat Treatment
| Grade | Equivalent | Delivery Condition | Typical Hardness |
|---|---|---|---|
| C45 / 1045 | 1.0503 / AISI 1045 | N or Q&T | 160–200 HB / 220–260 HB |
| 1050 / 1053 | AISI 1050 | Q&T | 240–300 HB |
| 4140 / 42CrMo4 | 1.7225 | Q&T | 240–320 HB |
| 4340 / 34CrNiMo6 | 1.6582 | Q&T | 280–360 HB |
| S355J2 | 1.0577 | N (+ impact at -20°C) | 150–190 HB |
| Q345B / Q355D | GB/T 1591 | N or TMCP | 140–180 HB |
Heat treatment is performed in gas-fired and electric furnaces with load-mapped temperature uniformity (±10°C), documented on time-temperature charts included with each certificate. Normalizing, quenching (water/oil/polymer), tempering, and stress-relieving cycles are set per grade, section thickness, and target property class — tell us the environment (temperature, impact, fatigue) and we propose the condition.
Manufacturing Standards
- Forging and delivery per ASTM A668, EN 10250, DIN 7526 practice, or customer-specific forging specifications.
- Ultrasonic testing per ASTM A388 / EN 10228-3 (acceptance class stated on PO); magnetic particle per ASTM E709 for machined surfaces.
- Mechanical testing: tensile, impact (Charpy V at service temperature), hardness mapping, grain size per ASTM E112.
- Certificates: EN 10204 3.1 standard; 3.2 with third-party witness (TÜV, LR, DNV) available.
Applications
- Weld-neck and slip-on flange blanks, anchor and orifice flange rings
- Gear blanks, sprocket rims, and slewing bearing races
- Pressure vessel shells, autoclave rings, and heat exchanger components
- Wind turbine yaw/pitch components and tower flanges
- Bearing housings, cylinder heads, and hydraulic press cylinder collars
- Pipe supports, wear rings, and kiln tyre blanks
Quality Assurance
Each ring carries full heat traceability from ingot/continuous cast source through forging and heat treatment. Standard testing package: chemistry check against grade limits, tensile test on quenched-and-tempered prolongation or sacrificial ring section, 100% UT on the finished ring (report with defect mapping), hardness survey at 4–8 points, and dimensional report. First-article rings for new customers are offered with video inspection calls. Our forging shop runs ISO 9001 and PED-compliant quality systems for pressure-retaining applications.
Packing & Delivery
Rings are shipped individually crated or on steel skids with rust-preventative coating (VCI paper or strippable film), machined faces protected by wooden guards. Forgings up to 12 t ship in flat-rack or break-bulk by arrangement with marine-grade lashing. Lead time: 25–40 days for rolled rings from stock billet, 40–60 days for open-die and Q&T rings including testing; air-freight test coupons ahead of the shipment are available for project-critical schedules.
Request a Forged Ring Quote
Send your OD × ID × height, grade, delivery condition, and testing requirements — engineering-backed quotation within 24 hours, production slots this month.
Contact us: Huaxia-Steel Forging Sales.