SAE 1055 vs 1060 vs 1070 High-Carbon Steel Comparison
When your application demands high strength, excellent wear resistance and the ability to hold a keen edge, the SAE 10xx high-carbon family is where the search begins. SAE 1055, SAE 1060 and SAE 1070 occupy the 0.55% to 0.70% carbon range, a sweet spot for springs, cutting tools, agricultural blades and wear components. This guide compares all three grades head-to-head so procurement teams can match chemistry and heat-treatment response to functional requirements, avoid over-specification and control landed cost.
We analyse chemical composition, mechanical properties, heat-treatment response, formability, weldability, fatigue performance and stock availability. Whether you source from China, India or Europe, the same selection principles apply: pick the lowest carbon grade that meets the engineering target, confirm the delivery condition on the mill certificate and verify hardness on receipt.
1. Chemical Composition Comparison
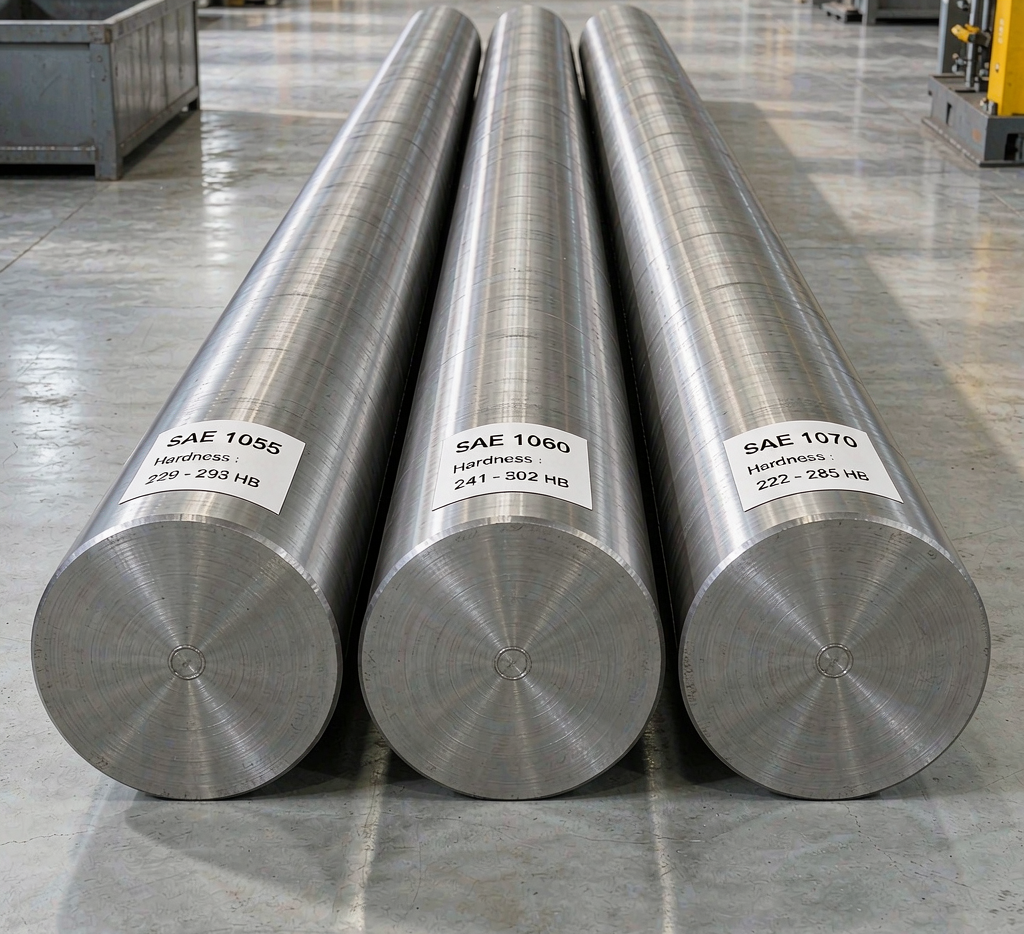
The SAE/AISI 10xx designation uses the last two digits to indicate the mean carbon content in hundredths of a percent. SAE 1055 therefore averages 0.55% C, SAE 1060 averages 0.60% C and SAE 1070 averages 0.70% C. Manganese is held within the same range across all three grades to maintain hardenability without excessive brittleness.
| Element | SAE 1055 (%) | SAE 1060 (%) | SAE 1070 (%) |
|---|---|---|---|
| Carbon (C) | 0.50 – 0.60 | 0.55 – 0.65 | 0.65 – 0.75 |
| Manganese (Mn) | 0.60 – 0.90 | 0.60 – 0.90 | 0.60 – 0.90 |
| Phosphorus (P), max | 0.040 | 0.040 | 0.040 |
| Sulfur (S), max | 0.050 | 0.050 | 0.050 |
| Iron (Fe) | Balance | Balance | Balance |
Although the carbon difference between adjacent grades is only 0.05% to 0.10%, each increment measurably raises the maximum achievable hardness after quenching. SAE 1070 can reach 65 HRC in thin sections, while SAE 1055 tops out around 55 HRC. For buyers, this means the grade choice directly determines whether a part can serve as a spring, a wear plate or a cutting edge.
2. Mechanical Properties Comparison
The values below represent hot-rolled round bar in the as-rolled or normalised condition. Quenched-and-tempered properties are significantly higher and are discussed in Section 3. Always request a mill test certificate with actual mechanical values.
| Property | SAE 1055 | SAE 1060 | SAE 1070 |
|---|---|---|---|
| Tensile strength | 650 – 800 MPa | 700 – 850 MPa | 750 – 950 MPa |
| Yield strength (0.2%) | ≥ 380 MPa | ≥ 420 MPa | ≥ 460 MPa |
| Elongation in 50 mm | ≥ 12% | ≥ 10% | ≥ 8% |
| Reduction of area | ≥ 35% | ≥ 30% | ≥ 25% |
| Hardness (HBW, as-rolled) | 180 – 220 | 200 – 240 | 220 – 270 |
| Impact energy (Charpy V) | ≈ 15 – 25 J | ≈ 10 – 18 J | ≈ 5 – 12 J |
As carbon rises, strength and hardness increase while ductility, toughness and impact energy decrease. SAE 1055 retains enough toughness for moderately impact-loaded parts; SAE 1070 is better suited for static or low-impact, high-wear applications where surface hardness is paramount.
3. Heat Treatment and Hardenability
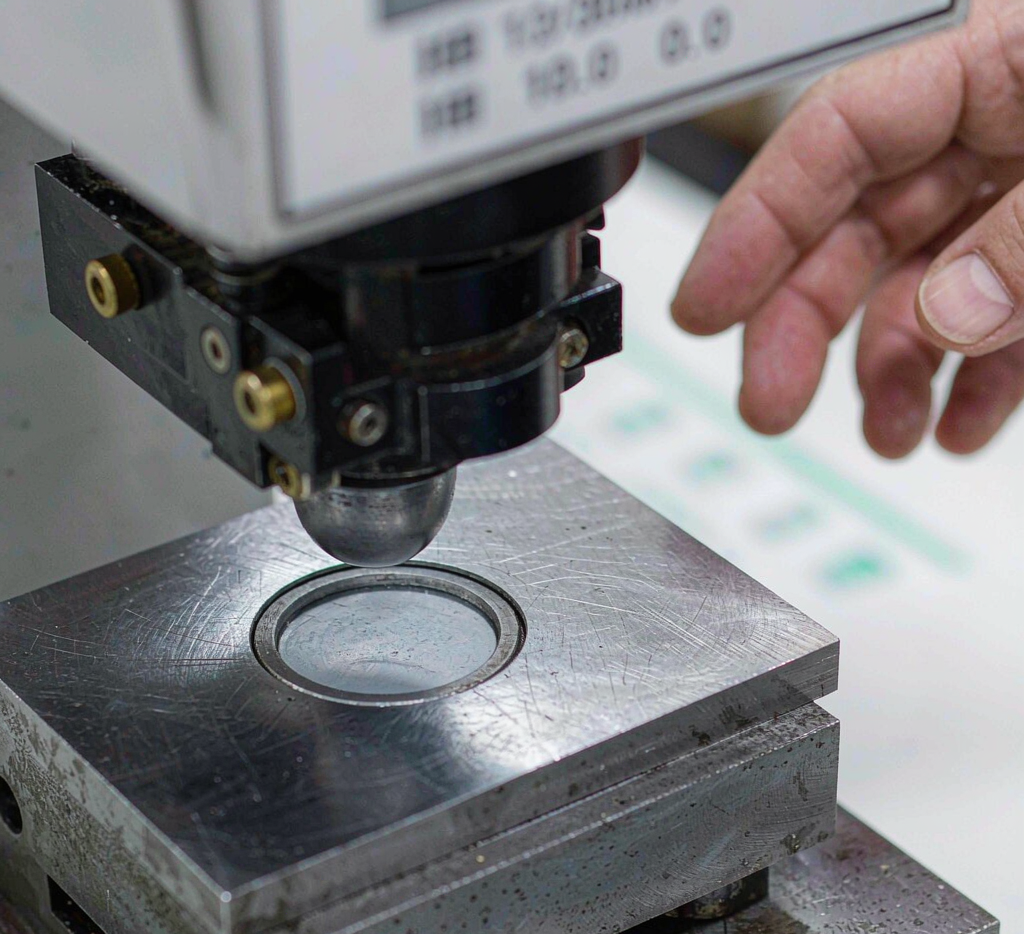
All three grades respond well to normalising, annealing, oil quenching and tempering. Water quenching is possible for thin sections but risks cracking in SAE 1070. The table below shows typical hardness ranges after common heat treatments.
| Condition | SAE 1055 | SAE 1060 | SAE 1070 |
|---|---|---|---|
| Hot-rolled | 180 – 220 HB | 200 – 240 HB | 220 – 270 HB |
| Normalised | 185 – 225 HB | 200 – 245 HB | 225 – 275 HB |
| Annealed | ≤ 170 HB | ≤ 185 HB | ≤ 200 HB |
| Oil-quenched & tempered (200°C) | 45 – 52 HRC | 50 – 57 HRC | 55 – 63 HRC |
| Oil-quenched & tempered (400°C) | 32 – 40 HRC | 38 – 46 HRC | 42 – 50 HRC |
| Induction-hardened surface | up to 58 HRC | up to 62 HRC | up to 65 HRC |
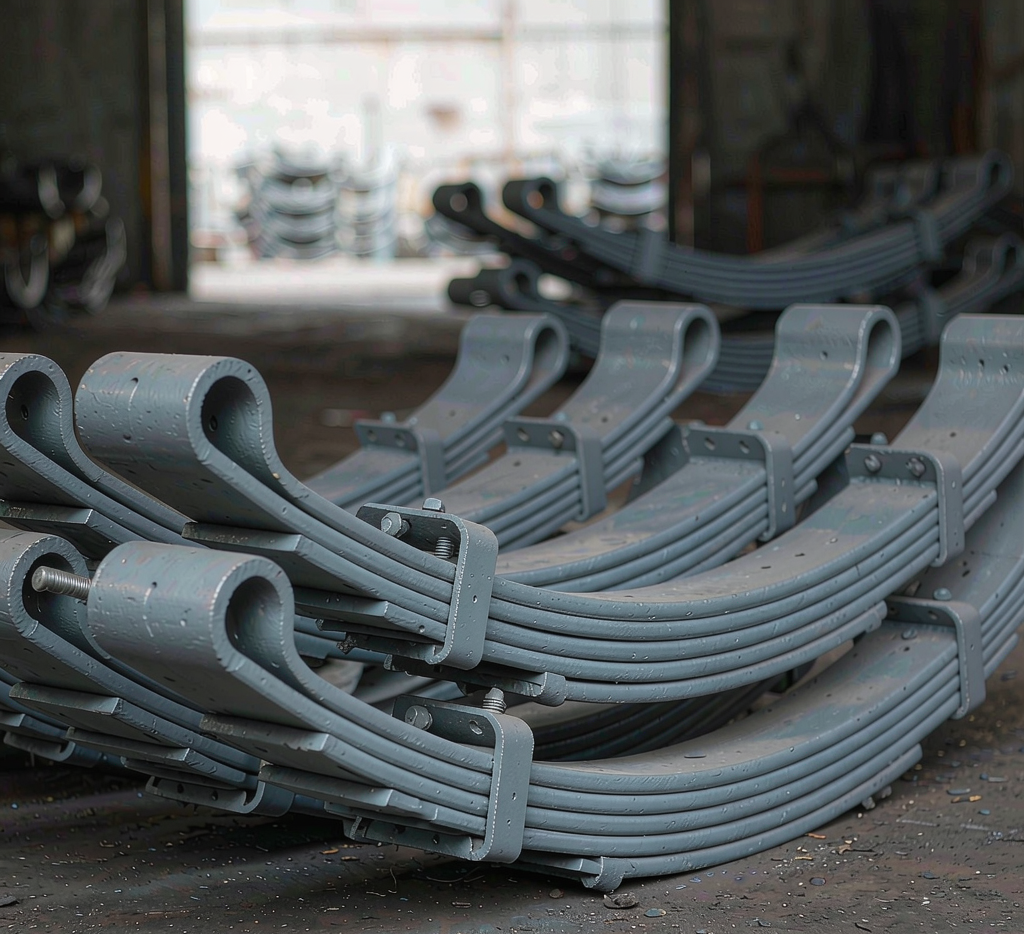
SAE 1060 is the most popular choice for leaf springs and flat springs because it offers the best balance of hardness, toughness and cost. SAE 1070 is preferred for music wire, cutting blades and hand tools where maximum edge retention is critical. SAE 1055 is used for agricultural tillage parts, scraper blades and wear plates where moderate impact is expected.
4. Formability, Machinability and Weldability
In the annealed condition, all three grades can be cold-formed, bent or stamped, though the force required rises sharply with carbon content. SAE 1055 is the most formable of the three and can be cold-headed in some applications. SAE 1070 is essentially limited to light forming and is usually processed in the annealed condition before hardening.
Machinability in the as-rolled condition is approximately 50 – 60% of free-machining steel for SAE 1055, dropping to 45 – 55% for SAE 1060 and 40 – 50% for SAE 1070. Annealing improves machinability by softening the material. Carbide tooling is recommended for production runs.
Weldability is poor across all three grades. SAE 1055 can be welded with pre-heat of 200 – 300°C using low-hydrogen electrodes and post-weld stress relief. SAE 1060 requires pre-heat of 250 – 350°C and careful cooling control. SAE 1070 is generally not recommended for welded fabrication; mechanical fastening or brazing is preferred. For any welding, post-weld normalising or tempering at 550 – 650°C is essential to restore toughness in the heat-affected zone.
5. Fatigue Performance and Spring Properties
The primary reason buyers choose high-carbon steel is fatigue resistance. When quenched and tempered to 42 – 48 HRC, these grades exhibit excellent endurance limits under cyclic loading.
| Property | SAE 1055 (Q&T) | SAE 1060 (Q&T) | SAE 1070 (Q&T) |
|---|---|---|---|
| Endurance limit (rotating bending) | ≈ 320 MPa | ≈ 360 MPa | ≈ 400 MPa |
| Working stress (leaf spring) | 350 – 450 MPa | 400 – 500 MPa | 450 – 550 MPa |
| Modulus of elasticity | 200 GPa | 200 GPa | 200 GPa |
| Sag resistance | Good | Very good | Excellent |
6. Typical Applications
- SAE 1055 — agricultural tillage blades, scraper blades, wear plates, gears, low-stress cutting tools, hand tools, spring washers, retaining rings and general-purpose wear components.
- SAE 1060 — leaf springs, flat springs, coil springs, music wire (lower tensile), saw blades, hand saws, knife blades, axles, shafts and chisels.
- SAE 1070 — music wire (high tensile), piano wire, cutting blades, shear blades, hand tools, springs for high-stress applications, wear strips and high-hardness wear parts.
7. Stock Forms and Availability
Chinese and Indian mills stock all three grades in round bar (6 – 200 mm diameter), flat bar (3 – 60 mm thick, 20 – 200 mm wide), strip (0.5 – 6 mm thick) and wire rod (5.5 – 22 mm). Lead times for standard sizes are 3 – 5 weeks. Non-standard dimensions or forged bars may require 8 – 12 weeks.
| Form | SAE 1055 | SAE 1060 | SAE 1070 |
|---|---|---|---|
| Round bar | 6 – 200 mm | 6 – 180 mm | 6 – 150 mm |
| Flat bar | 3 – 50 mm thick | 3 – 50 mm thick | 2 – 40 mm thick |
| Strip / coil | 0.5 – 6.0 mm | 0.5 – 6.0 mm | 0.3 – 5.0 mm |
| Wire rod | 5.5 – 22 mm | 5.5 – 22 mm | 5.5 – 18 mm |
8. Price Comparison and Sourcing Tips
As a rough guide, SAE 1055 costs about 5% more than SAE 1045 due to tighter specification and lower demand volume. SAE 1060 carries a 10 – 15% premium over SAE 1045. SAE 1070 can be 20 – 25% more expensive due to specialised applications and lower production volume. All three are widely available from Chinese mills with EN 10204 3.1 or 3.2 MTC.
When requesting quotes, always specify: grade, delivery condition (as-rolled, annealed, normalised, Q&T), dimensions, tolerance standard, and required hardness range. A vague specification like “1060 round bar” invites substitution with SAE 1045 or C45, which is cheaper but will not meet the hardness target after heat treatment.
FAQ
Which grade is best for leaf springs?
SAE 1060 is the industry standard for leaf springs because it offers the best combination of hardness, fatigue endurance and toughness after oil quenching and tempering to 42 – 48 HRC.
Can SAE 1070 be welded?
Welding SAE 1070 is not recommended due to its high carbon content. If welding is unavoidable, use 250 – 350°C pre-heat, low-hydrogen electrodes and immediate post-weld tempering at 550 – 650°C. For most applications, mechanical fastening is preferred.
What is the difference between SAE 1055 and AISI 1055?
There is no practical difference. SAE and AISI share the same four-digit numbering system for carbon steels. The chemistry ranges and mechanical properties are identical; the prefix only indicates which organisation published the standard.
Is SAE 1070 the same as 1075?
No. SAE 1070 has a carbon range of 0.65 – 0.75%, while SAE 1075 has 0.70 – 0.80%. The overlap is significant, but 1075 can achieve slightly higher hardness and is more commonly specified for knife blades and cutting tools.
Need High-Carbon Steel Bar or Strip?
Huaxia-Steel supplies SAE 1055, 1060 and 1070 round bar, flat bar, strip and wire rod with full EN 10204 3.1 / 3.2 mill test certificates. We offer annealed, normalised and quenched-and-tempered delivery conditions to your specification. Contact us today for a competitive quote on your high-carbon steel requirements.