Custom pipe bends are one of the most requested fabrication services in carbon steel procurement. A bend can replace an elbow plus two welds, cut leak points, and improve flow — but only if the bend radius, ovality and wall thinning stay within specification. This guide walks through the four main bending methods used in Chinese pipe fabrication plants, how to specify a bend correctly, and which tolerances to inspect before accepting shipment.
Why Bend Instead of Weld Fittings?
A 90° bend made from one continuous pipe offers three concrete advantages over an elbow-plus-welds solution:
Fewer welds, fewer defects: each circumferential weld is a potential leak path requiring NDT. Eliminating two welds per direction change reduces inspection cost and long-term maintenance.
Better flow: a smooth bend has a lower friction coefficient than a butt-weld elbow, reducing pressure drop in slurry, powder and high-velocity gas lines.
Lower cost at volume: for repetitive bends (handrails, boiler panels, structural tubing), bending is faster and cheaper than fitting and welding individual elbows.
The trade-off: bending needs the right equipment and process control. Poor bending produces ovality, wrinkles, wall thinning and springback errors — all of which are avoidable with the methods below.
Method 1: Rotary Draw Bending (Cold)
Rotary draw bending is the workhorse for small to medium diameters (typically 1/2″ to 8″, OD up to ~168 mm). The pipe is clamped to a rotating form die and drawn around it, with a pressure die holding the straight leg and — critically — a mandrel inside the pipe supporting the wall during the bend.
Best for: tight, repeatable radii (1D to 3D), thin-wall tubes, handrails, boiler and heat-exchanger tubes, automotive and machinery piping.
Quality level: with a mandrel, ovality can be held to ≤5% and often ≤3%; wrinkling is essentially eliminated.
Limits: tooling is size-specific — each diameter/wall/radius combination needs a die set, so it suits batch production, not one-off large bends.
For thicker-wall pipe where collapse risk is low, compression or three-roll bending shapes the pipe without internal support. This is common for structural tube, conduit and thick-wall process pipe where a generous radius is acceptable.
Best for: thick walls, larger radii (≥3D), schedules 40–80 pipe in 2″–12″ range.
Quality: expect ovality 5–8%; some wrinkling on the inner radius is possible if the setup is aggressive.
Advantage: no size-specific mandrel tooling, so it is economical for small quantities and large mixed orders.
Method 3: Induction Bending (Hot)
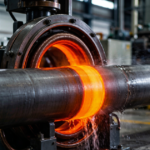
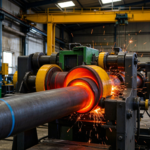
Induction bending is the premium method for large diameters (6″ to 60″+). A narrow band of the pipe is heated to 850–1,100 °C by an induction coil while the pipe is pushed slowly through; water cooling right behind the coil freezes the bend immediately. Because only a 20–30 mm band is hot, the rest of the pipe stays dimensionally untouched.
Best for: large OD pipeline bends, power plant and petrochemical headers, any radius from 3D to 10D+
Quality: ovality typically ≤2–3%, minimal wall thinning (under ~5%), no internal tooling needed regardless of size.
Metallurgy: reputable shops document heating temperature, travel speed and quench rate; post-bend heat treatment (normalizing or tempering) is applied for grades like A106 Gr.B or X65 when required by the piping spec (e.g., ASME B31.3/B31.8).
Induction bends cost more per piece than cold bends but beat welded large elbows on total installed cost once NDT and fit-up savings are counted.
Method 4: Hot Manual / Sand Bending
The traditional method — pipe packed with sand, heated in a furnace, bent over a template — survives only for one-off repairs and ornamental work. It offers poor repeatability and wall-thickness control, so specify it only when no machine access exists. For any export order, prefer methods 1–3 with documented parameters.
A minimum-radius rule of thumb: cold rotary draw bending needs at least 1.5D–2D with mandrel; below that, expect wall thinning beyond 10% and severe ovality. Induction bending comfortably handles 3D–10D, and 3D is the usual minimum for large pipeline bends. If a drawing shows a radius tighter than these limits, flag it with your fabricator before the order is cut — retrofitting bends is far more expensive than adjusting the design.
Material Selection for Bending
Seamless pipe (A106 Gr.B, A179, A192) bends best: uniform wall, no weld seam, consistent chemistry. This is the default for pressure piping bends.
ERW pipe (A53 Gr.B, A135) bends acceptably with the seam positioned at the neutral axis (45° from the bend plane) for cold bending; induction bending erases most seam concerns since the seam is fully re-heated and normalized locally — some specs require the seam to be radio-graphed before bending.
Avoid full-hard or cold-drawn-hard condition for tight cold bends; specify annealed or normalized condition when the bending radius is under 3D.
Grades above X60/X70 or P-series alloy steels usually require induction bending with post-weld/post-bend heat treatment — confirm with the mill’s procedure qualification records (PQR).
Quality Control Checklist Before Shipment
Verify bend radius and angle on a template or CMM — first article inspection for every new tooling setup.
Measure ovality at apex with calipers or a go/no-go ring gauge; record values in the inspection report.
Ultrasonic thickness check on the extrados of the bend for wall thinning, especially on schedule-standard pipe used at design pressure.
Visual check inner radius for wrinkles, and dye-penetrant or MPI on bends for high-pressure service.
Heat treatment records for hot bends — temperature charts or furnace data sheets tied to heat numbers.
Protective packaging: bent ends are vulnerable; require end caps and bundled crating so bends do not deform in transit.
How Bending Affects Price
Indicative FOB China pricing for custom bends (material included, ex-mill):
Rotary draw bend, ≤4″, 2D radius: US $2–8 per bend (tooling amortized over batch).
Roller/compression bend, 6″–12″: US $15–60 per bend.
Induction bend, 16″–36″, 5D: US $200–900 per bend, rising sharply with diameter and grade.
Two cost drivers dominate: tooling (one-time per size for rotary draw) and post-bend heat treatment (roughly 20–40% added cost on hot bends). If your project needs hundreds of identical bends, tooling amortization is trivial; for ten bends of an odd size, roller bending or a welded elbow may still win on total cost. Ask your supplier to quote both options with and without HT.
Buyer FAQ: Carbon Steel Pipe Bending
1. What is the tightest bend radius possible for carbon steel pipe?
With mandrel rotary draw bending, 1.5D is the practical minimum for most walls; 2D is safer for schedule 40. Induction bending typically starts at 3D. Below these radii, ovality and thinning usually exceed accepted piping code limits.
2. Does bending weaken the pipe?
Yes, slightly at the extrados: wall thinning of 5–10% is normal and accepted by ASME B31.3 provided minimum wall is maintained. Cold bending also work-hardens the bend area, which is generally beneficial for strength but reduces ductility; hot induction bends may need heat treatment to restore toughness.
3. Can ERW pipe be bent, or must it be seamless?
ERW bends fine with correct seam orientation and radius; many specs simply require the seam at 45° from the bend plane. For critical service or tight radii, seamless is preferred. Always state the pipe manufacturing process in your RFQ.
4. How do I control ovality on thin-wall tubes?
Use a mandrel (plug, ball or cable type) matched to the radius, increase the wiper die pressure, and if ovality still exceeds 3–5%, consider packed or induction bending. Mandrel type and lubrication are the two biggest levers.
5. What documents should come with custom bends?
At minimum: EN 10204 3.1 MTC for the parent pipe, a bend inspection report (angle, radius, ovality, wall thickness), heat treatment charts where applicable, and photos of first-article checks. For pipeline work, add procedure qualification records for the bending operation.
Conclusion
Successful pipe bending procurement comes down to three habits: specify radius and ovality explicitly (never just “90° bend”), match the method to diameter and wall (rotary draw for small tight bends, induction for large OD), and audit the QC data — ovality readings and thickness checks tell you more than any certificate. Suppliers who can produce those numbers on request are the ones worth shortlisting.
Need custom carbon steel bends? Huaxia-Steel supplies bent pipe from 1/2″ to 60″ with rotary draw, roller and induction processes, full dimensional reports and EN 10204 3.1 certificates. Send your bend schedule for a factory quote within 24 hours.
If you require further information about our metal sheet products or architectural projects, please don’t hesitate to leave your contact details and message here.
Our team of experts will respond within 24 hours to continue the discussion and provide you with any additional information you requires.