A36 vs 1018 Carbon Steel: Key Differences Explained
Buyers who source both structural steel and machined parts from Chinese or Indian mills keep asking the same question: A36 or 1018 — which grade do I actually need? The two are often quoted at nearly the same price, they look identical after rolling, and both are called “mild steel”. Yet they are produced to different standards, tested differently, and behave very differently once you put them on a lathe or weld them into a structure. In this guide we compare A36 vs 1018 carbon steel across chemistry, mechanical properties, formability, weldability, machinability and cost, and finish with a clear selection checklist you can paste straight into your RFQ.
What Is ASTM A36 Steel?
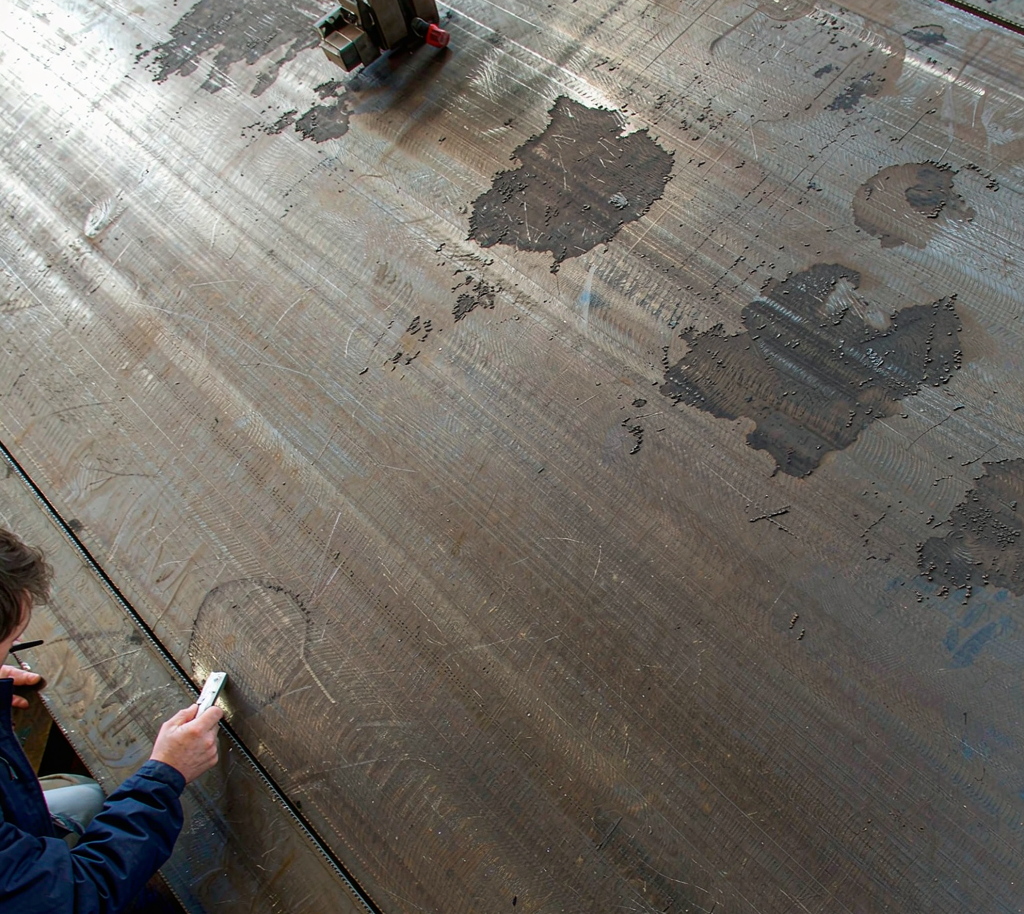
A36 is the workhorse structural carbon steel of North America, governed by ASTM A36/A36M. It is produced mainly as plates, wide-flange beams, angles, channels and bars for buildings, bridges, machinery bases and general fabrication. A36 is a killed steel with guaranteed minimum yield strength of 250 MPa (36 ksi) and tensile strength between 400 and 550 MPa (58–80 ksi). Because the standard covers structural shapes of many thicknesses, the carbon limit scales with thickness: up to 20 mm you may see C up to 0.25%, while thicker plates allow up to 0.29% with corresponding manganese adjustments.
Key points about A36 that matter to buyers:
Governed by ASTM A36/A36M; equivalent designations include GB Q235B, JIS SS400 and EN S235JR, though none is a perfect one-to-one match.
Chemistry limits on sulfur and phosphorus are wider than for cold-heading grades.
Charpy impact testing is not mandatory unless supplementary requirement S5 is invoked.
Supplied hot rolled, typically with mill scale surface.
What Is AISI/SAE 1018 Steel?
1018 is a low-carbon steel defined by the SAE-AISI numbering system and usually purchased to ASTM A108 (cold finished bars) or A29/A29M (general requirements for hot wrought bars). Its chemistry is deliberately narrow: carbon 0.15–0.20% and manganese 0.60–0.90%. That narrow window is the whole point — 1018 is engineered for consistent cold forming, machining and carburizing rather than for guaranteed structural strength. In the mill system it is a “composition-based” grade: the melt chemistry defines the grade, whereas A36 is a “property-based” grade where mechanical minimums define acceptance.
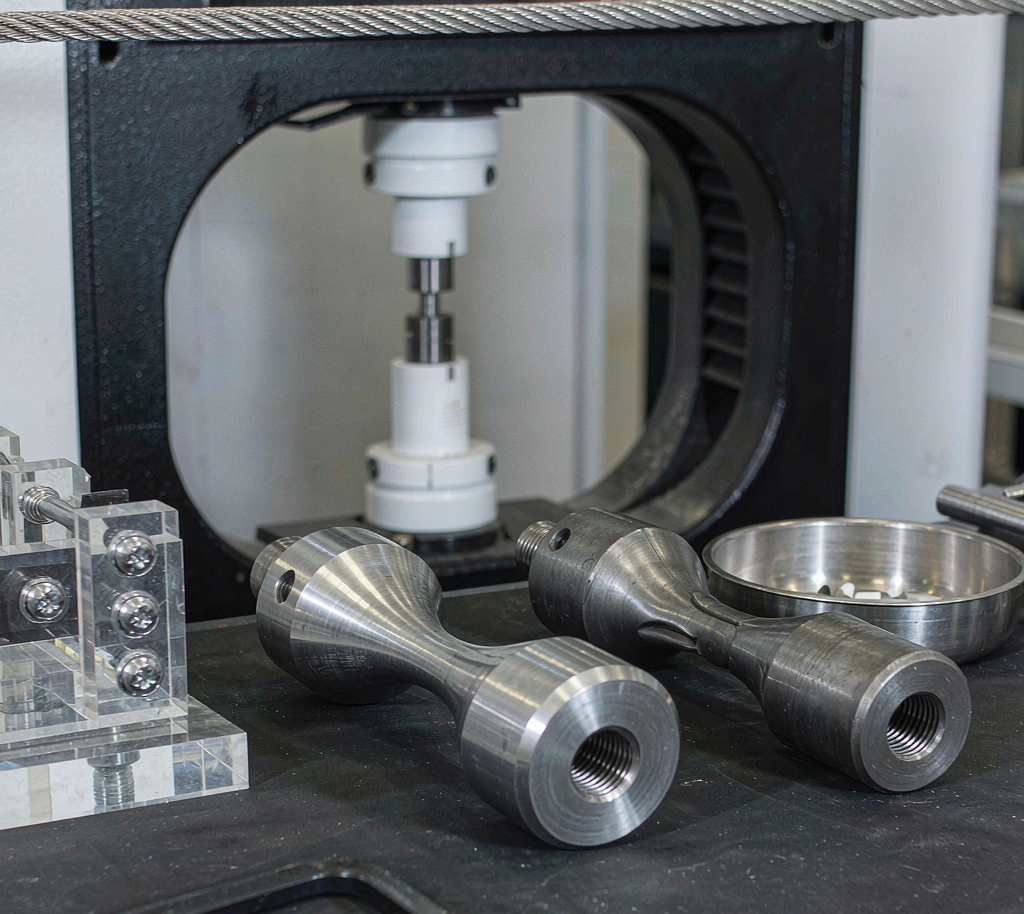
Typical 1018 properties: hot rolled tensile strength around 400 MPa with yield near 220 MPa; cold drawn tensile around 440–490 MPa with yield 370–415 MPa and elongation of 15–20%. Because the standard does not guarantee structural minimums in the same way A36 does, using 1018 bar in a load-bearing structural role requires the engineer to apply appropriate safety factors.
Chemical Composition Comparison
The table below compares typical chemistry limits. Note how A36 allows more carbon in thick sections while 1018’s window stays tight regardless of section size.
Element
A36 (≤20 mm)
A36 (thick plate)
1018 (A29/A108)
Carbon (C)
≤ 0.25%
≤ 0.29%
0.15–0.20%
Manganese (Mn)
—
0.80–1.20%
0.60–0.90%
Phosphorus (P)
≤ 0.04%
≤ 0.04%
≤ 0.04%
Sulfur (S)
≤ 0.05%
≤ 0.05%
≤ 0.05%
Silicon (Si)
0.15–0.40%
0.15–0.40%
—
In practice both grades melt within overlapping windows, and a single heat at a Chinese mill can even dual-certify. The difference is the guarantee written on the mill test certificate: A36 guarantees yield and tensile minimums; 1018 guarantees a carbon window that makes downstream processing predictable.
Mechanical Properties: A36 vs 1018 Side by Side
Property
A36 (hot rolled plate)
1018 (hot rolled)
1018 (cold drawn)
Yield strength
≥ 250 MPa (36 ksi)
~220 MPa
≥ 370 MPa typical
Tensile strength
400–550 MPa
~400 MPa
440–490 MPa
Elongation (50 mm)
≥ 20%
~25%
15–20%
Hardness (HB)
120–150
~126
126–160
Charpy V-notch
Optional (S5)
Not standard
Not standard
Three practical takeaways: first, only A36 gives you a code-recognized 250 MPa yield minimum for structural design. Second, cold drawn 1018 actually out-yields hot rolled A36 in bar form, which is why 1018 works fine for shafts and pins. Third, if your drawing calls out impact toughness at low temperature, neither grade automatically satisfies it — you must order Charpy testing as a supplement.
Weldability and Formability Compared
Both grades weld well with common processes (SMAW, GMAW, FCAW) and both compute a low carbon equivalent — typically around 0.28–0.35 CEV — so no preheat is normally needed for sections under 25 mm. Differences appear at the edges of the envelope. A36 in thick plates, with carbon approaching 0.29% and Mn up to 1.20%, can push CEV toward 0.43 and deserves a modest 50–100 °C preheat on restrained joints. 1018’s tighter, lower carbon window keeps CEV below 0.35 across all bar sizes, making it very forgiving for automatic welding of small parts.
For cold forming, 1018 is the better choice: its lower and narrower carbon band gives excellent behavior in bending, swaging, cold heading and roll forming, with less springback variation between heats. A36 plates bend acceptably down to inside radii of about 1.5t when the bending line is perpendicular to the rolling direction, but wide variations between heats mean fabricators should qualify bend tests per heat rather than assume.
Machinability: Where 1018 Clearly Wins
On the standard scale where AISI 1212 equals 100%, 1018 rates roughly 78% while A36-type structural steel rates around 60–65%. The reason is sulfur and inclusion control plus consistent chemistry: 1018 machines to a better finish, tolerates higher cutting speeds, and produces more predictable chip breaking on CNC lathes. For high-volume turned parts — bushings, spacers, shafts, pins, fittings — this difference directly converts into cycle time and tool cost. This is precisely why turning houses buy 1018 and rarely accept A36 bar as a substitute.
Surface quality reinforces the gap: cold drawn 1018 arrives with a smooth, bright finish typically achieving 32 µin Ra or better, ready for many applications without further finishing. Hot rolled A36 with mill scale needs descaling and usually machining before any precision use.
Typical Applications for Each Grade
A36: structural frames, base plates, bridge components, storage tanks, construction equipment, transmission towers, ship building blocks, brackets and gussets in welded assemblies. Anywhere a building code or construction standard references “structural mild steel”, A36 or its regional equivalent is expected.
1018: CNC turned and milled parts, shafts, studs, dowel pins, spacers, hydraulic fittings, key stock, cold headed fasteners, chain links, and carburized gears or cams where a hard case over a soft core is wanted. If the part goes on a lathe before it goes into service, 1018 is usually the economical answer.
Price and Availability in Export Markets
In Chinese and Indian export quotes, both grades sit within roughly 3–8% of each other for small lots, with 1018 cold drawn bars commanding the premium for the drawing operation itself. A36 plates are commodity items with deep stock availability in 6–100 mm; 1018 is stocked mainly in bar form from 3 to 100 mm diameter. Lead times are similar (stock sizes ship in 7–15 days; odd sizes 20–35 days). Beware of “conversion” quotes where a mill offers Q235B as A36 or 20# pipe steel as 1018 — each substitution shifts one property you may care about, so require the equivalent-standard table on the MTC.
Which One Should You Order? A 5-Question Checklist
Is the part structural and welded into a frame? Order A36 (or S235JR/Q235B per your code).
Is the part machined on a lathe or mill in volume? Order 1018 cold drawn.
Do you need guaranteed yield strength on the MTC? A36 — 1018’s cert lists chemistry, not structural minimums.
Do you need tight, repeatable cold forming? 1018’s narrow carbon window wins.
Do you need a hard case over a soft core? 1018 carburizes well; A36 is not intended for case hardening.
When in doubt for mixed lots, some buyers take A36 for the welded structure and 1018 for the machined spacers that bolt into it — sourcing both from one factory simplifies traceability and consolidates freight.
Frequently Asked Questions
Can I substitute 1018 for A36 in a welded frame?
Not automatically. 1018 hot rolled bar has no guaranteed 250 MPa yield minimum, so a code-compliant structural design cannot assume it. For non-code, lightly loaded fixtures the substitution is usually fine, but the responsible engineer should approve it and the MTC must show the actual chemistry.
Is Q235B a true equivalent of A36?
For most export fabrication work, yes: Q235B offers 235 MPa yield and comparable tensile, and mills routinely issue A36-equivalent certificates after adding the ASTM impact or tensile supplements. Confirm with your end client whether they accept dual-certified material.
Does 1018 rust faster than A36?
No meaningful difference — both are plain carbon steels with similar corrosion rates. Cold drawn 1018’s bright surface may show rust spots slightly sooner because there is no protective mill scale, so oil film or wrapping matters more than grade selection.
Which grade is cheaper for the same weight?
Hot rolled 1018 and A36 price within a few percent of each other in most export markets; the real cost difference appears in machining. A part designed in 1018 can cut total finished cost 10–20% versus A36 once tooling life and cycle time are counted.
Heat Treatment and Hardness Potential
Neither grade is designed to be through-hardened, but they behave differently when heat is involved. 1018 responds well to carburizing: pack, gas or vacuum carburizing at 900–925 °C followed by oil quench and temper produces a 55–62 HRC case over a tough 90–110 HRB core — the classic recipe for pinions, cams and wear bushings. Carbonitriding is another common route for small 1018 parts. A36, with its wider chemistry band and mill-scale surface, is rarely case hardened; attempts produce inconsistent case depths between heats because carbon and manganese vary plate to plate.
Stress relieving is practical for both: 1018 cold drawn bars can be stress relieved at 500–550 °C to reduce distortion in machining, and A36 weldments are routinely post-weld stress relieved at 590–620 °C when code or service conditions require it. Neither grade is intended for quench-and-temper; if you need 30 HRC through the section, step up to 1045 or 4140 instead of fighting a mild steel.
Size Availability and Surface Condition
Form
A36
1018
Plate
3–200 mm, widths to 3,000 mm
Rare (available to special order)
Structural shapes
Beams, channels, angles, HSS
Not produced
Hot rolled bar
6–100 mm round/flat/square
3–100 mm round/flat/hex
Cold drawn bar
Uncommon
3–80 mm, h9–h11, bright finish
Surface finish
Mill scale, as-rolled
Hot rolled scale or bright cold drawn
This availability table drives a lot of real-world decisions: if your bill of materials mixes plates, beams and bars, a single A36 supply chain covers all of it, while 1018 exists only in bar territory. Conversely, a CNC parts program that needs only 12–40 mm bright bar consolidates perfectly on 1018.
Reading the Mill Test Certificate: Grade-Specific Checks
For A36, verify four lines on the MTC: yield strength at or above 250 MPa in the relevant thickness, tensile within the 400–550 MPa band, carbon within the thickness-based limit, and — if you specified it — Charpy results at the agreed temperature. Watch for certificates quoting “typical” instead of actual heat results; a proper EN 10204 3.1 or ASTM-style certificate shows the real ladle analysis and the actual test piece results with specimen orientation.
For 1018, the audit is chemistry-centric: carbon must sit inside 0.15–0.20% — a heat at 0.23% C will machine differently and may crack in severe cold heading, even though it “looks like 1018” everywhere else. Cold drawn bar buyers should also check straightness, OD tolerance class and hardness range on the cert or inspection report.
Cost Optimization Tips for Mixed Orders
Consolidate heats where possible: if some parts tolerate either grade, assign the tolerant parts to the grade already on order to avoid a second heat minimum.
Buy 1018 in the largest practical bar and turn down: for small shafts, machining from 30 mm bar is often cheaper than buying many small diameters once quantity discounts and freight per tonne are counted.
Specify tolerances you need, no more: h11 cold drawn costs less than h9; asking for precision across the board inflates quotes 5–10%.
Ask for dual certificates: Q235B/SS400/A36 dual-certified plates sometimes price below single-standard A36 while satisfying your documents.
Three Real RFQ Scenarios and the Right Answer
Scenario
Recommended grade
Reasoning
Welded machine base frame, 12 mm plate plus bolted spacers
A36 plate + 1018 spacer stock
Structure gets code-recognized yield; machined spacers get chip-friendly steel
500 machined pins per week on automatic lathes
1018 cold drawn
Cycle time and surface finish outweigh the small material premium
Galvanized outdoor bracket, cut and folded from 8 mm sheet
A36 / Q235B
Formability at 8 mm is fine, and availability in sheet sizes is far better than 1018
These three cases cover the majority of mixed orders we see, and they illustrate the practical rule: let the process decide, not the price list. Where a part is welded into a load path, A36-type steel protects your certification. Where a part is cut by tools, 1018 protects your margins.
Five Purchasing Mistakes to Avoid
Ordering 1018 bar for a welded structural frame because it was cheaper on the day — no guaranteed yield strength, so the cert will not support the design.
Ordering A36 for CNC turning to save 4% on material — tool life, surface finish and cycle time erase the saving within one shift.
Accepting “equivalent” chemistry without a table — insist the MTC lists the equivalent standard and the actual values behind it.
Forgetting thickness-based carbon limits — A36 chemistry changes with plate thickness; a 40 mm plate cert looked at through a 12 mm lens hides real values.
Ignoring surface condition in the quote — hot rolled with scale versus cold drawn bright differ in downstream cleaning, straightening and machining allowance costs.
Avoid those five and the A36-versus-1018 decision becomes a two-minute line item instead of a recurring production problem. When your RFQ covers several part families, send us the full bill of materials: our engineers routinely split a single order across both grades so every component gets the material it was designed for, shipped in one container with one set of certificates.
How Mills Price the Two Grades
Understanding the price structure helps you judge whether a quote is fair. Both grades start from the same billet and scrap basket, so base steel cost is nearly identical — typically within 2–3% at the mill gate. What separates the landed price is processing: 1018 cold drawn bar adds drawing, straightening and peeling (roughly 8–12% over hot rolled), tighter chemistry control adds a small premium, and small-diameter bright bar adds inspection and packing labour. On the A36 side, plate pricing rises steeply with thickness above 50 mm because of slower rolling and higher reject rates, and the price of dual-certified Q235B/A36 plate reflects the extra testing.
Freight also favours consolidation: a 20 ft container loading 22–25 tonnes of mixed A36 plate plus 1018 bar spreads ocean freight over the whole order, whereas two small separate shipments of 8 tonnes each lose roughly 15–20% of the freight efficiency. Buyers running 3–5 containers a year routinely save more from consolidation than from grade-switching decisions.
Storage and Handling on Arrival
Steel arrives in the container dry on the bill of lading but wet in reality: condensation during ocean transit (“container rain”) is the number one cause of avoidable surface rust. Open containers in a covered area, wipe bundles, and apply a thin oil film if material will sit more than a week — especially for cold drawn 1018, whose bright surface shows rust within days. Stack bars on timber dunnage with at least 100 mm ground clearance, separate heats for traceability, and rotate stock first-in first-out. For A36 plate, keep mill scale intact until fabrication; it is a surprisingly effective temporary corrosion barrier and removing it early invites flash rusting.
Source A36 and 1018 From One Verified Factory
Huaxia-Steel supplies both A36 structural plates/shapes and cold drawn 1018 bars from audited partner mills, with EN 10204 3.1 mill test certificates, third-party inspection (SGS/BV/TUV) on request, and export packing to any port. Send us your drawing or RFQ list and our engineers will confirm the right grade, size tolerance and delivery terms within 24 hours.
If you require further information about our metal sheet products or architectural projects, please don’t hesitate to leave your contact details and message here.
Our team of experts will respond within 24 hours to continue the discussion and provide you with any additional information you requires.