ASTM A131 Shipbuilding Steel: Grades, Normalizing and How to Order
Marine structures demand steel that can absorb impact at low temperature without brittle fracture, because a hull or offshore module sees repeated dynamic loading in cold, corrosive seawater. ASTM A131 is the US specification most buyers meet when they order ABS-classed plate, and it defines a family of hull structural grades from ordinary A to cryogenic E. This guide walks through the grades, the heat-treatment rules and the ordering details that prevent a costly rejection at the shipyard or the class surveyor’s desk.
Buying marine plate is less about the steel chemistry and more about the paperwork: the class approval, the impact test temperature, and the mill test certificate. A cheap plate that lacks the right stamp or was not normalized will be rejected at the block assembly stage, where removing and replacing it costs far more than the material. The sections below show exactly what to write so the plate arrives correct.
What ASTM A131 Covers
A131 specifies carbon steel plates, shapes and bars for the construction of ships and marine structures, intended to be certified by a recognised classification society (ABS, BV, DNV, LR, CCS). It is the material backing for the familiar “ABS Grade A / B / D / E” plate stamps you see in a yard. The standard sets chemistry limits, mechanical properties and impact requirements but leaves the class approval — the actual society stamp — to the certifying body.
The Four Ordinary Strength Grades
| Grade | Min yield (MPa) | Impact test temp | Typical use |
|---|---|---|---|
| A | 235 | No impact required | Warm-climate deck, non-critical |
| B | 235 | 0 °C | General hull, temperate |
| D | 235 | −20 °C | Hull in cold water |
| E | 235 | −40 °C | Ice-going / arctic zones |
All four share the same 235 MPa minimum yield; the difference is the charpy impact temperature. As you move from A to E you are buying tougher, low-temperature-resistant plate — essential for bow sections, ice belts and anything exposed to freezing spray. Grade A, with no impact requirement, is only safe in warm waters and non-critical structure; specifying it for a North Atlantic hull is a serious error.
Higher Strength Grades (AH/DH/EH 32, 36, 40)
For larger vessels, A131 also provides higher-strength grades with yield up to 390 MPa (EH40). These let designers thin the plate and save weight while keeping strength, at a higher material cost. The same A/B/D/E toughness logic applies, just at higher strength levels — so an AH36 plate is high-strength with 0 °C impact, and an EH40 is high-strength with −40 °C impact.
Normalizing and Controlled Rolling
Grade D and E plates, and most higher-strength plates, are supplied normalized or thermo-mechanically controlled-rolled to guarantee a fine, uniform grain that delivers the required impact values. Always state the required condition on the purchase order — a non-normalized Grade E may fail the −40 °C impact test and be rejected. TMCP (thermo-mechanical control process) rolling achieves the same toughness with lower carbon equivalent, which also improves weldability.
Controlled rolling also reduces the risk of lamellar tearing in thick assemblies, because the through-thickness properties are more consistent. For junction regions and bracket connections where welding is heavy, ask the mill about Z-quality (through-thickness) testing even if the base spec does not require it — it is cheap insurance against a teardown.
Impact Testing and Acceptance
Charpy V-notch impact tests are taken transverse to rolling at the specified temperature. Acceptance is typically an average of 34 J (some rules 27 J) with limited single-specimen shortfall. Require the mill to report both average and individual values on the MTC so the yard can file them with class. A certificate that only prints the average can hide one failing specimen that would fail the survey.
| Checkpoint | What to verify | Common failure |
|---|---|---|
| Class approval | ABS/BV/DNV/LR/CCS stamp | Wrong society for the build |
| Impact temp | Matches grade | Grade E tested at −20 °C |
| Rolling condition | Normalized if required | As-rolled supplied |
| Ultrasonic | Per A578 / EN 10160 if specified | Not requested, later rejected |
Surface, Dimensional and UT Requirements
Marine plate is usually ordered with ultrasonic testing to detect laminations, especially for thick hull longitudinals and deck plates. Specify the UT standard (ASTM A578 or EN 10160) and acceptance level. Edges should be sheared or flame-cut clean, and flatness must meet the class rule for the thickness. Surface discontinuities beyond the class limit must be repaired by approved grinding or welding.
Common Procurement Mistakes
- Ordering Grade A for a cold-water hull — it has no impact requirement.
- Forgetting to request normalizing on D/E plates.
- Mixing class societies between plates in one block.
- Omitting UT when the rule or detail requires it.
How to Write the Purchase Order
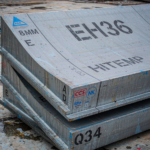
- State standard and grade: e.g. “ASTM A131 Grade EH36, normalized”.
- State class society and rule version (ABS 2024 etc.).
- Give dimensions, quantity, and tolerance (e.g. EN 10029 Class B).
- Require MTC to EN 10204 3.1 with impact values.
- Specify UT standard and acceptance level if applicable.
Attach a marked-up plate plan where possible, showing which grade goes in which zone. Shipyards coordinate plate by zone, and a clear plan prevents a Grade B plate being cut for an ice-belt location. The small effort of zoning the order saves rework and keeps the class file clean.
Plate Thickness and Tolerances
Marine plate thickness follows the class rule and standards such as EN 10029; minus tolerances are tight because the plate is often the designed section with no extra corrosion allowance on the strength side. Specify the tolerance class and confirm the mill can hold it on the thickness you order — thick plates are harder to roll to a tight minus than thin ones, and a wide tolerance can push you into a heavier nominal size than your calculation assumed.
Traceability and MTC Details
For classed work the MTC must tie each plate to its heat and to the class approval. Require the certificate to list chemistry, tensile, impact values at the correct temperature, and the rolling condition. Keep the MTC with the plate through cutting and assembly so the surveyor can verify any piece on demand; a missing certificate can stop a block from being signed off even when the steel is perfect.
Working With Your Fabricator
Give the fabricator the grade, the zone and the welding procedure at the same time, because the preheat and heat-input limits follow from the carbon equivalent of the plate. A high-strength EH grade may need controlled heat input that changes the weld sequence; sharing the spec early avoids a weld that passes visually but fails the procedure qualification.
Budgeting for Marine Plate
Price marine plate by combining base steel, the class approval fee, normalizing or TMCP rolling, UT and the MTC workflow — not just the per-tonne steel number. Higher grades and normalized condition cost more up front but reduce weight and rework, and a correct first-time inspection is worth more than a discount that triggers a rejection at the block stage.
FAQ
Is A131 the same as ABS Grade A?
A131 is the ASTM material spec; “ABS Grade A” is the classification stamp. A plate is ordered to A131 and certified by ABS — the two go together, one is the material, the other the approval.
When do I need Grade E?
When the structure operates at or below −40 °C, such as ice-belt plating, arctic modules or equipment exposed to freezing spray. Grade D (−20 °C) covers most cold-water hulls.
Can I use A36 instead of A131?
Not for classed hulls. A36 lacks the required impact testing and class approval. A131 is the correct spec for ship and offshore structural plate.
Normalized or as-rolled?
For Grade D/E and higher-strength grades, normalized or TMCP rolling is normally required to meet impact values. Confirm on the order or expect rejection at inspection.
Plate Edge Preparation
For welded marine structure the plate edge matters as much as the face. Edges are sheared, sawn or flame-cut and may be machined or ground to a profile before welding. Specify the edge preparation (square, single-V, double-V, J) so the yard cuts to the weld procedure rather than grinding on site, which is slower and harder to control.
For thick plates the heat of flame cutting can harden the edge; where the rule requires it, the edge is ground or heat-treated to restore toughness. State any edge-softening requirement on the order so the mill or the processor includes it and the surveyor sees it done.
Z-Quality and Through-Thickness
In thick, highly restrained joints, stresses act through the plate thickness and can tear laminations. Z-quality plate is made and tested for through-thickness reduction of area (commonly a minimum of 15% or 25% RA). For bracket connections and heavy splice plates, ask for Z-quality even when the base A131 grade does not demand it; it is cheap insurance against a lamellar tear that forces a teardown.
Welding Consumables Matching
Match the electrode or wire to the plate grade and the design temperature. For Grade D/E and higher-strength grades, use low-hydrogen consumables and control heat input so the heat-affected zone keeps its toughness. The MTC tells you the plate chemistry; the welding procedure tells you the consumable and the parameters — keep both documents together through fabrication.
Preheat and Interpass Temperature
Higher carbon equivalent and low temperature call for preheat to avoid hydrogen cracking. The procedure specifies the preheat and the maximum interpass temperature; both depend on the plate grade and thickness. Share the grade with the fabricator at order time so the weld sequence and the heating gear are planned, not discovered when the first joint is laid.
Storage and Rust Prevention
Marine plate stored uncovered will surface-rust and may need blasting before use, adding cost and delaying the job. Keep plates dry and separated, and for long outdoor storage consider a temporary coating. Rust that exceeds the class limit must be removed by approved grinding or blasting, so prevention is cheaper than remediation.
Cutting Methods
Plasma, laser and oxy-fuel cutting are all used for marine plate; the choice follows thickness and the edge quality needed. Laser gives the cleanest edge for thin plate, oxy-fuel is economic for thick sections, and plasma sits in between. Tell the processor the edge tolerance you need so they pick the method that meets it without overpaying for capability you do not use.
Inspection and Survey
Class surveyors check identity, dimensions, surface and the MTC at incoming and at key fabrication stages. Have the certificate, the UT report and the heat records ready and legible; a missing document can stop a sign-off even when the steel is correct. Build the inspection pack as the plate moves through the yard, not at the end.
Case Study: Ice-Belt Upgrade
A common upgrade replaces ordinary-strength belt plating with Grade E (−40 °C) on a vessel moving into colder trade. The change is not just the steel grade but the normalization, the impact testing and the class stamp, all of which must appear on the new MTC. Getting the specification right at reorder avoids a rejection when the upgraded plate is surveyed against the original class rule.
Mill Order Template
A clean order reads: standard and grade, normalizing or TMCP condition, class society and rule, dimensions and quantity, tolerance class, impact temperature, UT standard and acceptance, and the MTC type. With those fields filled, the mill can confirm immediately whether it can meet the spec, and the surveyor can verify the plate without a follow-up request for missing data.
Common Reject Reasons
The usual rejections are wrong impact temperature, missing or wrong class stamp, no UT when required, and surface defects beyond the class limit. All four are caught at the order stage if you state the condition and the society clearly, which is why the template above prevents most of the costliest failures.
Class Society Differences
ABS, DNV, BV, LR and CCS apply the same A131 chemistry but differ in rule versions, UT acceptance and stamp format. Always name the society and the rule edition on the order; a plate certificated to the wrong society is rejected even if the steel is identical, because the surveyor validates against the specified rule.
Plate Marking and Traceability
Every plate should carry a legible heat number, grade, class stamp and UT mark at the mill, and those marks must survive cutting and handling so the surveyor can trace any piece back to its MTC. Where the rule requires it, the marks are transferred to the cut parts by the fabricator. Lost traceability is treated as a quality gap, so confirm the marking scheme on the order.
Acceptance Sampling
For large orders, agree an inspection and test plan that says how many plates are checked and to what. A statistical sample is normal, but critical zones may call for 100% UT. Define the sample size and the acceptance number up front so a borderline lot is judged by the plan, not by whoever happens to inspect it that day.
Cold Weather Erection
Low-temperature erection adds risk: weld hydrogen cracking is more likely and the steel is less forgiving of impact. Keep the grade matched to the temperature, preheat as the procedure requires, and store plates dry so surface moisture does not add hydrogen at the arc. Cold-weather work is where a correct A131 specification pays for itself in avoided delays.
Welder Qualification
Only qualified welders should weld classed plate; the welder performance qualification matches the process, the position and the grade, so the person at the arc is proven for that exact joint. Using an unqualified welder on marine plate is a direct route to a survey rejection and a torn-out weld.
For Grade D/E and higher-strength plates, low-hydrogen consumables and controlled parameters are part of the qualification, not an optional extra. The WPQ and the welding procedure specification must agree on the grade and the conditions, or the joint is not certified even if it looks sound.
Keep the WPQ on file beside the MTC; the surveyor checks the welder, the procedure and the plate together, and a missing qualification stops the sign-off. Treat the three documents as one package from the start of fabrication rather than gathering them at the end.
Non-Destructive Testing On Site
After welding, magnetic particle or ultrasonic testing checks the joints against the procedure; a visual check alone misses subsurface flaws that later grow into failures. The NDT method follows the rule and the joint type, and it is written into the inspection plan before welding begins.
For thick plates, ultrasonic testing is the usual method because it sees into the section; for surface cracks, magnetic particle or dye penetrant is faster. Match the method to the defect you expect, and record the result against the joint so any later issue is traceable to the inspection that passed it.
NDT is not a final gate but part of the quality loop; when a defect is found, the response — repair, re-test, record — is itself documented. A clean NDT trail is what lets the surveyor accept a welded assembly without opening it up, which saves both time and risk on the job.
Get a Quote from Huaxia-Steel
Factory-direct carbon steel with MTC, third-party inspection, and fast export shipping. Tell us your grade, size, quantity and destination — we return a firm quote within 24 hours.