Carbon steel hardness testing is the fastest, cheapest and most frequently specified check on any steel purchase order — yet it is also where most buyer disputes originate, because hardness numbers mean different things in different scales. A mill certificate that says “200 HB” and a fabricator’s reading of “22 HRC” can both be correct and describe different measurements of the same bar. This guide explains the three principal hardness test methods used on carbon steel — Brinell (HBW), Rockwell (HRC/HRB) and Vickers (HV) — how to convert between them, how hardness relates to tensile strength, and how to write hardness requirements into your PO so the certificate you receive matches the check you will perform on arrival.
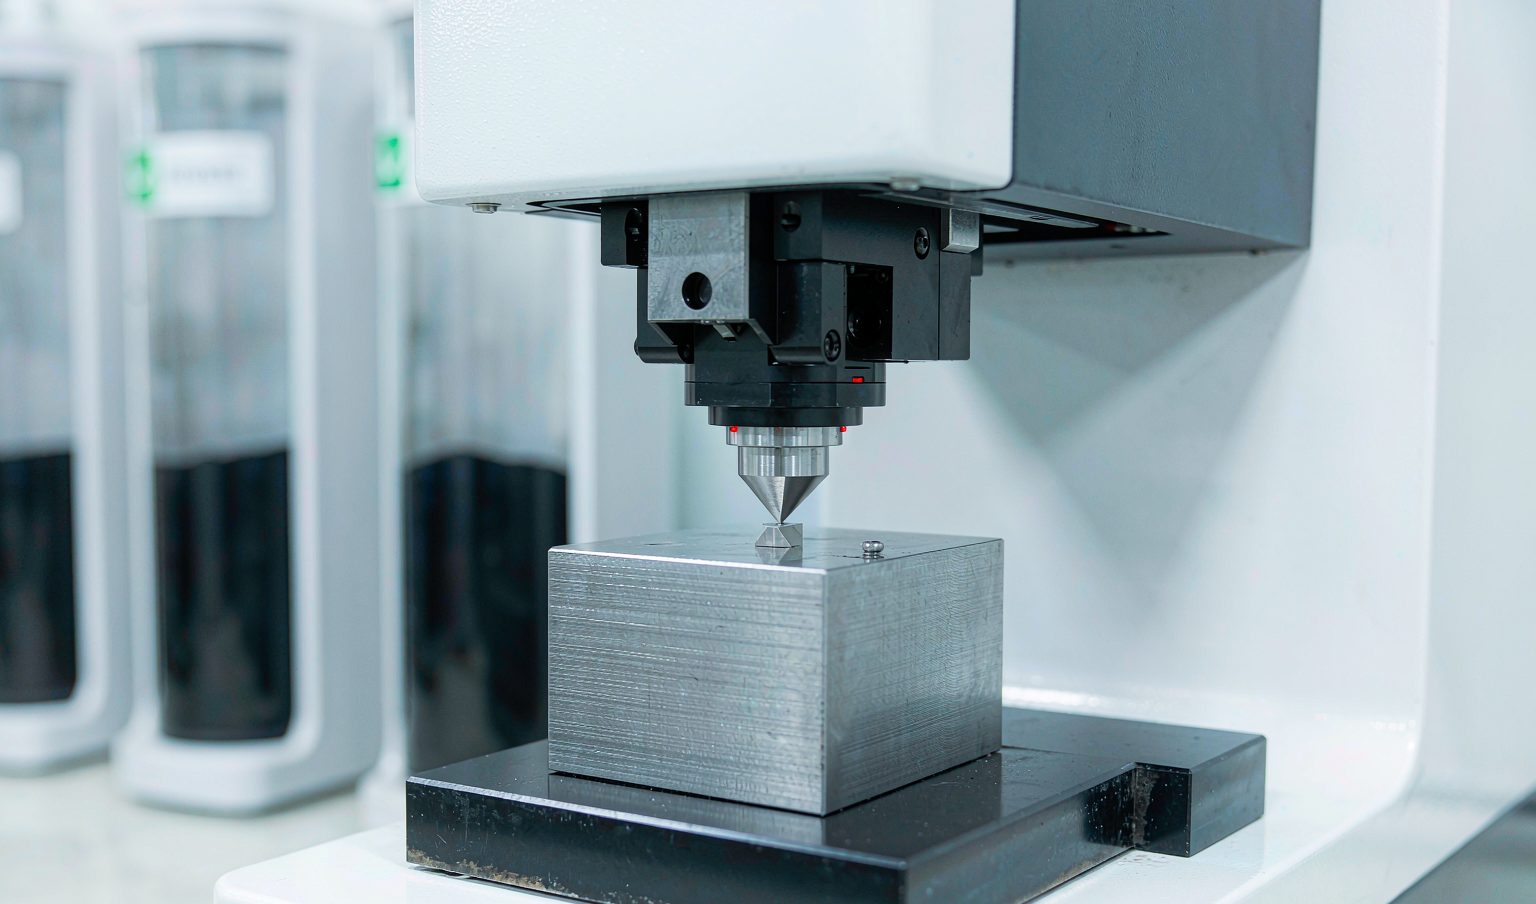
Why Hardness Matters in Carbon Steel Procurement
Hardness is resistance to localized plastic deformation — practically, resistance to indentation. For a buyer it serves three purposes. First, it is a fast proxy for strength: for carbon steels, tensile strength in MPa tracks Brinell hardness at roughly 3.3–3.6 × HB, so a single hardness reading verifies the heat treatment state of an entire shipment in seconds. Second, hardness predicts machinability and wear behavior: a bar at 302 HB will chew through tooling specified for 200 HB material. Third, hardness is the acceptance criterion written into almost every component drawing — so verifying it protects you from the most common mill mix-ups: untempered material, missing heat treatment, or the wrong grade entirely.
Hardness testing is governed by ASTM E10 (Brinell), ASTM E18 (Rockwell), ASTM E92/E384 (Vickers) and ISO 6506/6507/6508 equivalents. Test method standards define the equipment, procedure and validity rules; product standards (ASTM A29, EN 10083, JIS G4051) define which scale and limit values apply to each grade and condition.
Brinell Hardness (HBW): The Workhorse for Bar and Plate
The Brinell test presses a 10 mm tungsten carbide ball into the surface with a 3000 kgf load for 10–15 seconds and measures the indentation diameter optically. The resulting HBW number averages over a relatively large indentation — which is exactly why it is the standard method for hot rolled bar, plate and forgings. Coarse microstructures, decarburized skins and surface irregularities that would corrupt a Rockwell reading are absorbed into a meaningful average.
- Best for: hot rolled and forged carbon steel bar, plate, large weldments, castings — anywhere the surface is not finely finished.
- Typical range on carbon steel: 120 HB (hot rolled low carbon) to 500+ HB (hardened); above ~650 HB the ball itself deforms and readings lose validity.
- Limitations: large indentation (not suitable for finished machined surfaces), slower than Rockwell, requires optical measurement of the impression.
- Rule of thumb: material thinner than about 8× the indentation depth, or bar under 25 mm diameter in hardened condition, should not be Brinell tested on the full section.
Rockwell Hardness (HRC/HRB): Fast and Non-Destructive Enough for Finished Parts
Rockwell measures indentation depth under load and reads the number directly from the machine — no optical measurement, no polishing, seconds per test. Two scales dominate carbon steel work. HRB uses a 1/16 inch ball at 100 kgf and covers roughly 100–260 HB (annealed and hot rolled low/medium carbon steel). HRC uses a diamond cone at 150 kgf and covers roughly 240–900 HV equivalents (hardened and tempered steel, from ~20 HRC upward). Because the test leaves only a small mark, HRC is the standard scale for finished and semi-finished components: machined shafts, gears, Q+T bars and case-hardened parts.
Practical cautions: the surface must be clean and reasonably flat (a curved bar surface skews HRC readings low; grind a flat or use a correction factor), the test needs adequate support thickness (roughly 10× indentation depth), and readings should be spaced at least 3× indentation diameter apart. A common certificate dispute arises when a buyer checks HRC on an as-rolled decarburized skin — the reading is 3–5 points low through no fault of the steel. Specify where the test is taken, or accept light surface grinding before testing.
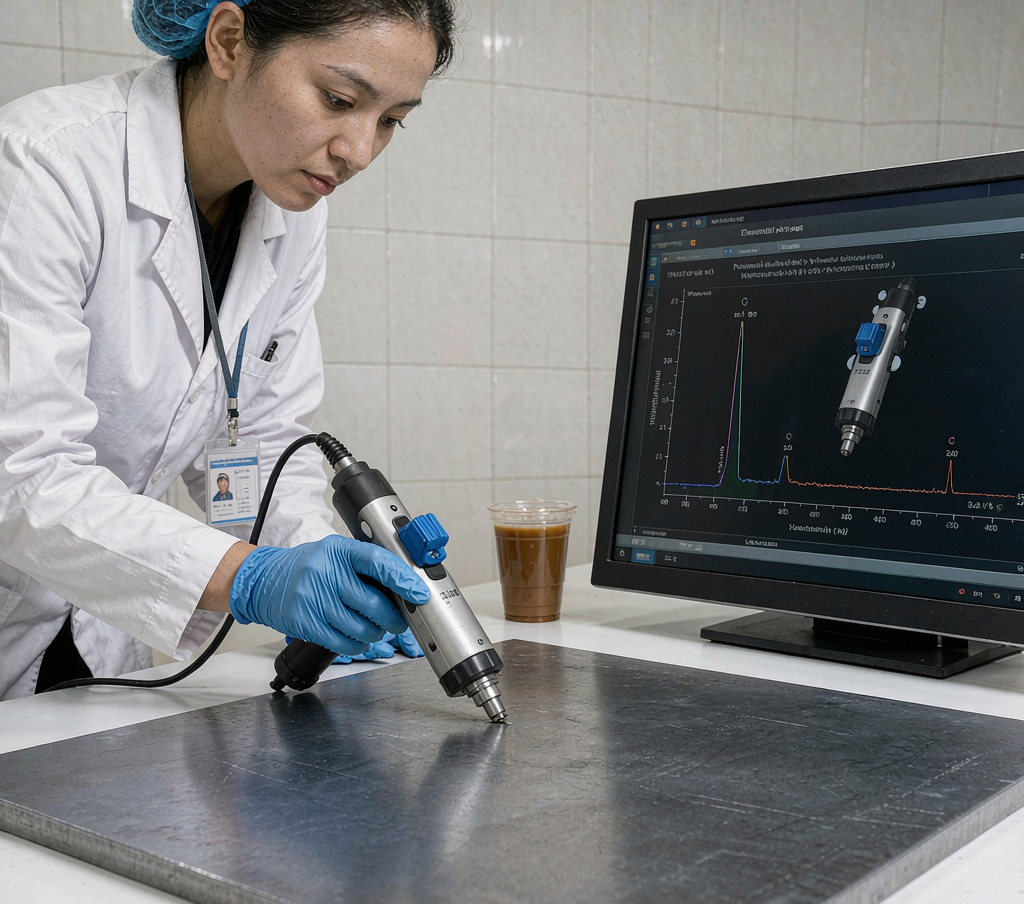
Vickers Hardness (HV): The Precision and Microhardness Scale
Vickers presses a 136° diamond pyramid into the surface and measures the diagonal of the resulting square indentation. The scale is continuous from soft annealed steel to hardened cases (approximately 5 to 1500 HV), which is its great advantage: one scale spans everything. On carbon steel procurement, Vickers appears in three situations: microhardness traverses across carburized or induction-hardened cases (case depth verification), hardness testing of thin sections where Brinell would punch through, and referee testing when two methods disagree. For bulk bar and plate buying, Vickers is less common simply because each reading takes longer than Rockwell.
Hardness Conversion Table for Carbon Steel
Conversion between scales is approximate — it depends on steel type and condition — but the following table (based on ASTM E140 for steels) covers the range buyers actually encounter.
| Brinell HBW | Rockwell HRB | Rockwell HRC | Vickers HV | Approx. tensile (MPa) |
|---|---|---|---|---|
| 120 | 70 | — | 125 | 410 |
| 150 | 80 | — | 158 | 500 |
| 180 | 89 | — | 190 | 610 |
| 200 | 93 | — | 210 | 670 |
| 220 | 97 | — | 232 | 740 |
| 240 | 100 | 20 | 253 | 800 |
| 260 | — | 24 | 273 | 870 |
| 285 | — | 29 | 299 | 950 |
| 320 | — | 33 | 336 | 1080 |
| 350 | — | 37 | 368 | 1180 |
| 400 | — | 42 | 421 | 1350 |
| 450 | — | 47 | 474 | 1520 |
| 500 | — | 51 | 527 | 1690 |
Use conversions for cross-checking, never as contractual values. If your drawing says 28–32 HRC and the mill certificate says 285 HB, that is the same condition — but write the acceptance in the scale the drawing uses to keep third-party inspections unambiguous.
Hardness vs Tensile Strength: What the Relationship Buys You
For carbon and low alloy steels, tensile strength ≈ 3.3–3.45 × HBW across the 150–500 HB range. This correlation lets a hardness test stand in for a tensile test in several practical cases: spot-verifying that a Q+T bar really is in the 28–32 HRC condition the certificate claims; screening incoming material before committing machining hours; and catching a grade substitution (1045 sold as 4140, for example — the soft bar reveals it instantly). It does not replace the tensile test for certificate purposes — yield, elongation and reduction of area require the full test — but as a tripwire it is unmatched for cost and speed.
Portable Hardness Testing: Leeb and UCI for On-Site Checks
When receiving inspection happens in a warehouse rather than a laboratory, portable testers are the practical choice. Leeb (rebound) testers ASTM A956 convert impact velocity loss to an HL value and display converted HB/HRC/HV — fast and effective on heavy bar and plate, but sensitive to surface condition and mass (thin sections give false soft readings). UCI (ultrasonic contact impedance) testers read like a bench Rockwell and suit smaller or fixed parts. For third-party pre-shipment inspection on carbon steel orders, Leeb hardness checks at defined points per heat, cross-checked against the mill certificate, are the standard package — and they routinely catch the untempered bar before it ships.
How to Write Hardness Requirements Into Your Purchase Order
- Name the scale: “28–32 HRC” not “hardness 285.” Mixed scales invite disputes and conversion arguments.
- Define test location: mid-radius of the bar cross-section, or at the surface for case-hardened parts. Surface decarburization is not a defect if the spec tests the core.
- Reference the method standard: ASTM E18 for HRC, E10 for HBW — this locks in procedure, not just number.
- State sampling frequency: per heat, or per X pieces per bundle. Per-heat testing is the mill default; more frequent sampling costs more.
- Require the scale on the certificate: EN 10204 3.1 certificates should list hardness alongside tensile results; if hardness is missing, ask for it explicitly at PO stage.
- Agree on arrival-inspection rights: who tests, with what instrument, and what happens on a borderline reading (typically re-test and average per the method standard’s rules).
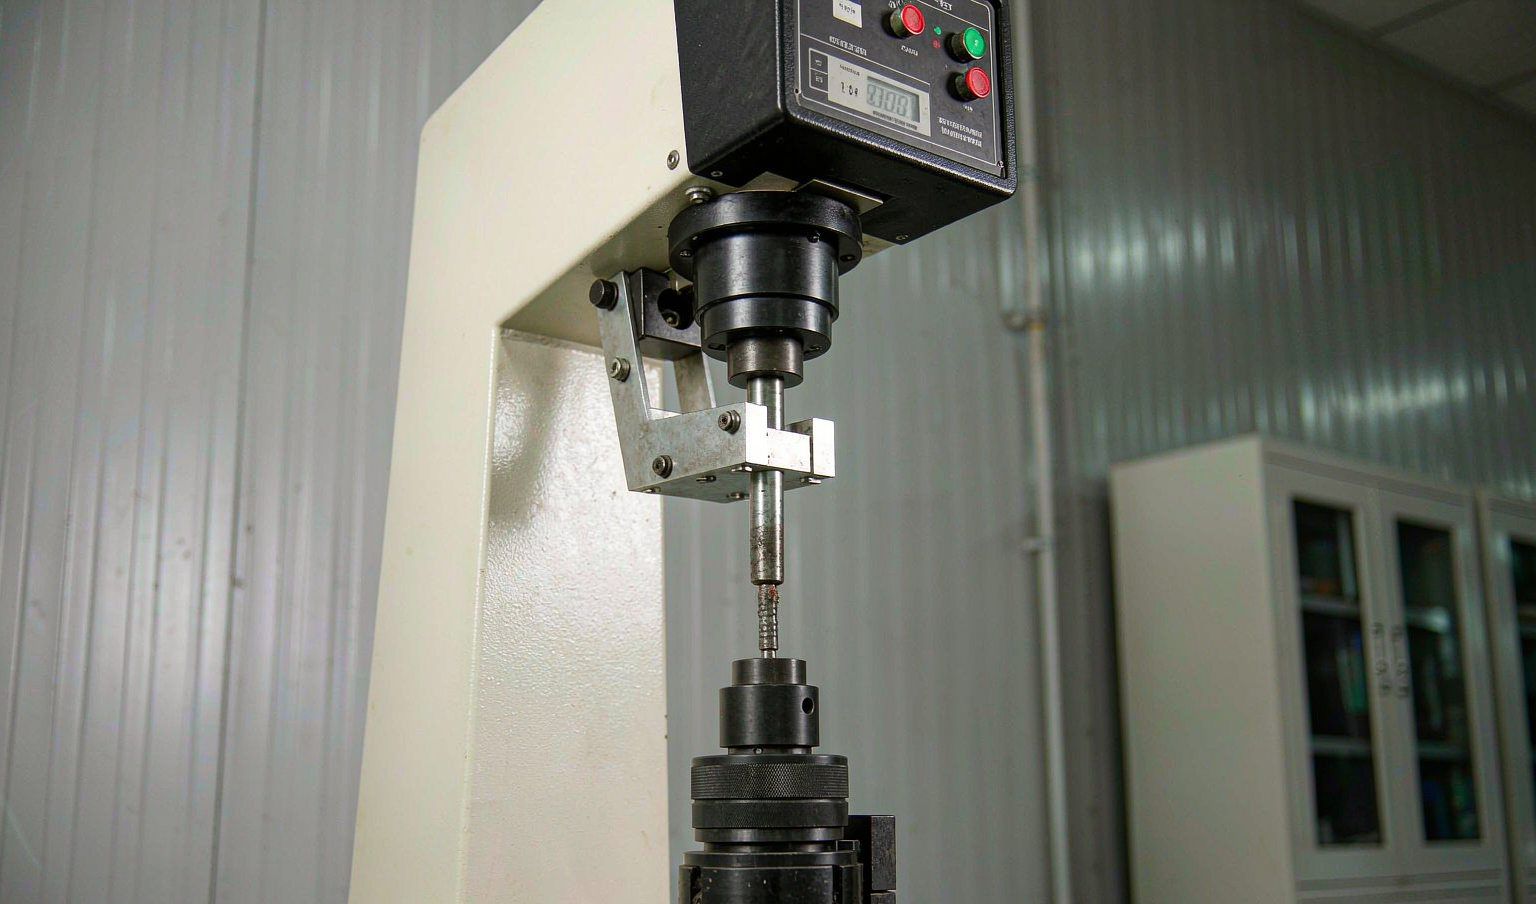
Sampling Plans for Incoming Hardness Inspection
How many pieces to test on arrival is a trade-off between confidence and cost. A practical tiered plan used by many importers: test one piece per heat on all heats (a few minutes with a portable tester), expand to 10 % of pieces in any bundle that reads outside specification, and hold the full bundle pending a bench re-test if any two readings disagree by more than 2 HRC or 20 HB. For critical components — shafting that will be induction hardened, bars destined for CNC production lines — a first-piece destructive check (sectioning and mid-radius hardness traverse) on each heat is cheap insurance against the one failure mode hardness checks on the surface cannot see: decarburized core sections from improper bar processing.
Record everything against bundle numbers, not just heat numbers. When a claim follows months later, the difference between “one bundle was soft” and “heat X read 10 points low on three dates” determines whether the mill accepts responsibility. Photographs of the indentation with a gauge reading visible, dated, form the evidence chain — and cost nothing to capture.
What Hardness Predicts — and What It Does Not
Hardness correlates strongly with tensile strength, moderately with machinability and wear resistance, and poorly with toughness, fatigue and formability. Machining shops know the relationship as a rule of thumb: every +10 HB above 200 costs roughly 5–8 % of tool life on carbon steel, which is why a “200 HB max” clause on machining stock protects both parties. Wear resistance in unlubricated sliding tracks hardness almost linearly; in abrasive service it tracks hardness to the 1.5 power. But two steels at identical hardness can differ by 5× in impact energy — hardness says nothing about the tempering state’s toughness, so a brittle untempered martensitic bar and a properly tempered bar at the same HRC are indistinguishable to a hardness test alone. This is precisely why certificates pair hardness with Charpy or elongation data: each property catches what the other misses.
For formability, the practical conversion matters in both directions: steel below about 150 HB bends and forms freely, 150–200 HB forms with generous radii, and above 220 HB cold forming invites cracking — one more reason to check hardness on material sold as “bendable” or “cold forming quality.”
A Typical Dispute: How Hardness Data Resolves It
A real pattern we see several times a year: a buyer receives S45C bright bar certified at 200 HB, machines it, and reports finished parts failing a 22–28 HRC drawing requirement. The mill’s certificate and the buyer’s bench readings disagree. In most cases the resolution comes from controlling the test variables rather than from either side being wrong: the buyer tested on the as-drawn surface with a portable Leeb (reads 2–4 points low), the certificate’s value came from a ground cross-section with a bench Rockwell. Agreed protocol — bench HRC on a ground flat at mid-radius, three indents averaged — reconciles the readings to within a point in the overwhelming majority of cases. The lesson for procurement: specify the test protocol, instrument type and surface preparation in the PO inspection clause, and disputes become rare before they become expensive.
Hardness Bands by Grade and Condition: A Buyer’s Reference
Writing a hardness band into the PO requires knowing what the mill can actually guarantee. The bands below reflect common export-mill practice for bar and plate in standard conditions — they are realistic acceptance windows, not theoretical limits.
| Grade / condition | Typical hardness band | Notes |
|---|---|---|
| S235JR / A36 / Q235 hot rolled | 120 – 160 HB | Structural, as-rolled |
| 1045 / C45 / S45C hot rolled | 163 – 207 HB | Machining stock |
| 1045 / C45 cold drawn | 180 – 230 HB | Work-hardened bright bar |
| C45 / S45C Q+T | 217 – 255 HB | Shafts, gears |
| 4140 / 42CrMo4 annealed | ≤ 217 HB | For machining then re-HT |
| 4140 / 42CrMo4 Q+T standard | 28 – 32 HRC (277–302 HB) | The “4140 HT” stock condition |
| 4140 Q+T high strength | 34 – 38 HRC | Restricted toughness trade-off |
| SAE 1141 / 12L14 cold drawn | 170 – 220 HB | Free-machining grades |
| Q+T plate (A516 Cl70, S355) | per standard tables | Usually verified by tensile, hardness spot |
Two cautions on using these bands. First, cold drawn bar hardness varies along the bar by 5–10 HB because the drawing process does not; set bands wide enough to absorb that reality or accept per-bundle testing protocols. Second, hardened-and-tempered bands narrower than 4 HRC (e.g. “30–32 HRC exactly”) are process-control fantasies at mill scale — 28–32 or 30–34 HRC is what a competent Q+T line delivers consistently. Unrealistic bands do not buy quality; they buy discrepancies.
Instrument Calibration: The Silent Source of Bad Data
A hardness number is only as good as the machine behind it, and both portable and bench testers drift in ways that produce systematic errors nobody notices until two parties compare readings. Bench Rockwell and Brinell machines require daily verification against calibrated reference blocks per ASTM E18/E10 — not the machine’s own display, but an actual indent on a certified block within its validity dates. Portable Leeb testers need verification on a test block of comparable hardness and mass to the parts being measured; a tester verified on a 60 HRC block says nothing about its accuracy at 200 HB. UCI probes drift with wear on the Vickers tip and require scheduled verification too. For importers running their own receiving checks, the discipline that pays: log every verification with block serial number and date, rotate test blocks before they exceed their certified indent limit, and keep one designated “dispute instrument” under tighter control for referee measurements. Fifteen minutes of calibration housekeeping per week eliminates the majority of hardness arguments that otherwise end in claims meetings.
Frequently Asked Questions
What is the normal hardness of mild steel? Hot rolled low carbon steel (S235JR, A36, Q235) typically measures 120–160 HB, roughly 65–80 HRB. Cold drawn versions rise by 10–20 HB from work hardening. Any bar “mild steel” reading above ~180 HB deserves a chemistry check.
Can I convert HB to HRC reliably? Within the overlap range (roughly 240 HB / 20 HRC and up), ASTM E140 conversion is good to 1–2 points and fine for verification. Below 20 HRC use HRB instead — HRC is simply not accurate on soft steel, and converted values below its range are meaningless.
Why is my HRC reading low on hot rolled bar? Decarburization. Hot rolled and forged surfaces lose 0.1–0.4 mm of carbon during processing; the soft skin reads 3–5 HRC low even when the core is correct. Grind the surface flat before testing, or test a sectioned cross-section.
Does hardness testing damage the material? Negligibly. A Brinell impression is a few millimeters; Rockwell and Vickers marks are smaller still. On machined surfaces the marks are ground out easily. This is why hardness — unlike tensile testing — can be performed on production parts without scrapping them.
What hardness should heat-treated 4140 be? The standard Q+T delivery is 28–32 HRC (285–300 HB, ~1000 MPa tensile). Hardened-and-tempered for maximum wear resistance can run 42–48 HRC; surface-hardened via induction reaches 55 HRC+ on the case while the core stays at 28–32 HRC.
Order Carbon Steel With Hardness You Can Verify
Huaxia-Steel supplies carbon and alloy steel bar, plate and pipe with hardness values specified, tested and certified per your requirements — ASTM E10/E18 procedures, EN 10204 3.1 certificates, and third-party inspection (SGS, TUV, BV) welcome before shipment.
Send us your grade, condition and hardness requirement for a factory direct quotation.