Carbon Steel Machining Tips: Feeds, Speeds and Tool Choice
Carbon steel is one of the most machined metals in the world, yet shops still struggle with built-up edge, chatter, and inconsistent tool life. The reason is usually not the material itself but the gap between the grade being cut and the cutting parameters being used. Low-carbon steels behave very differently from medium-carbon or high-carbon grades.
This article gives practical carbon steel machining tips for turning, milling, drilling, and tapping. Use it to pick starting feeds and speeds, choose the right insert geometry, and reduce scrap when machining Chinese-imported carbon steel bar and plate.
1. Match the Grade to the Process
Carbon content changes machinability more than most buyers realize:
- Low carbon (C ≤ 0.25%) – C10E, C15E, 1018, 1020. Soft, gummy, prone to built-up edge (BUE). Needs sharp tools and adequate chip clearance.
- Medium carbon (0.25–0.60%) – C45, 1045, S45C, S50C. Good balance of strength and machinability. Add sulphur for free-machining variants.
- High carbon (0.60–1.0%) – C60, 65Mn, 1095. Harder, more abrasive, shorter tool life. Lower speeds and tougher inserts are required.
2. Starting Cutting Speeds (Vc, m/min)
| Operation | Low carbon | Medium carbon | High carbon |
|---|---|---|---|
| Turning with carbide | 250–350 | 200–280 | 120–180 |
| Milling with carbide | 180–260 | 150–220 | 90–140 |
| Drilling HSS | 25–35 | 20–30 | 12–20 |
| Tapping HSS | 10–15 | 8–12 | 5–8 |
Reduce speeds by 20–30% for interrupted cuts, long overhangs, or older machines. Increase only after confirming stable chip formation and acceptable tool wear.
3. Feed Rates and Chip Load
Feed per tooth in milling should start at 0.1–0.18 mm for medium-carbon steel and 0.12–0.22 mm for low-carbon steel. In turning, a feed of 0.15–0.3 mm/rev works for roughing; finish passes drop to 0.05–0.12 mm/rev. Too low a feed increases rubbing and heat; too high a feed overloads the tool edge.
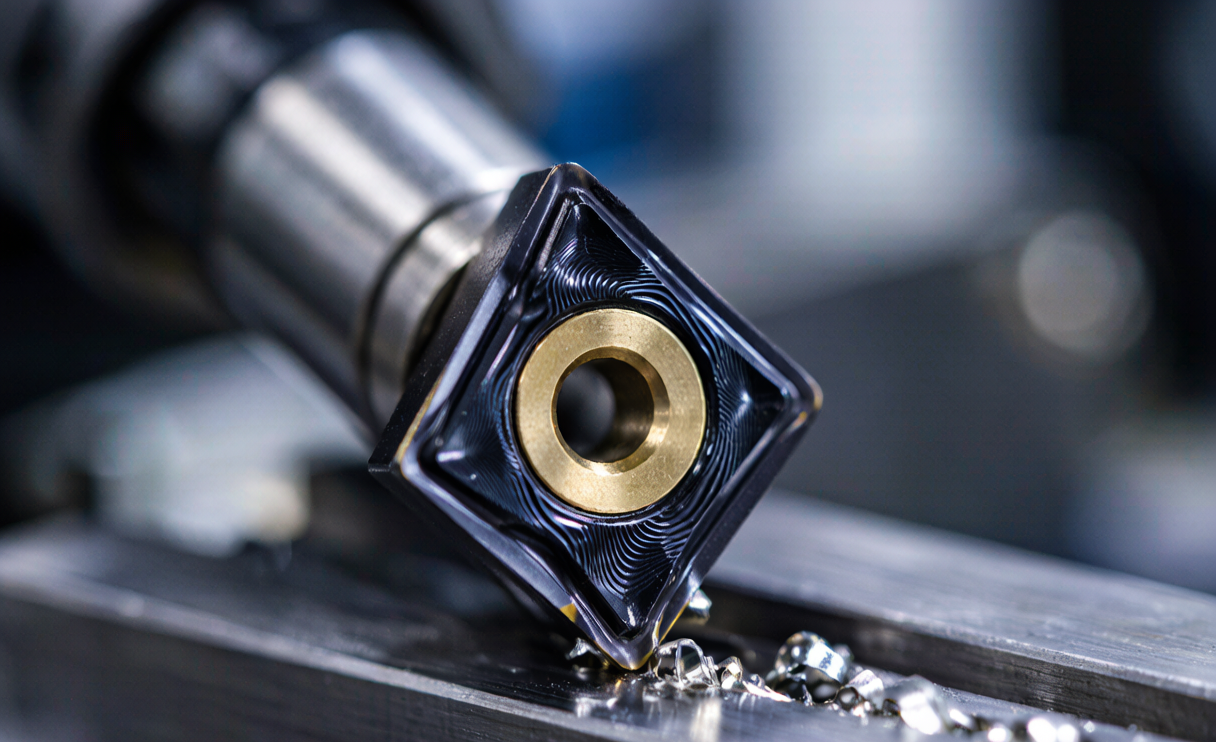
4. Insert and Tool Geometry
- Geometry: Use positive rake inserts for low-carbon steel to reduce BUE. Use slightly negative or neutral rake for harder grades to protect the edge.
- Coating: PVD-coated carbide (TiAlN, TiSiN) handles the heat in medium and high-carbon steel. Uncoated or TiN-coated carbide is fine for low-carbon work.
- Edge prep: A light hone (0.02–0.04 mm) prevents micro-chipping without increasing cutting pressure.
5. Coolant and Lubrication
Water-soluble cutting fluid at 6–10% concentration is standard for most carbon steel machining. For high-carbon or free-machining grades, oil-based fluids can improve surface finish and tool life. Flood coolant is preferred; mist only when flood is impossible.
6. Workholding and Vibration Control
Medium- and high-carbon steels produce higher cutting forces. Use short overhangs, rigid toolholders, and stable fixtures. Chatter is usually a rigidity problem, not a speed problem. If chatter appears, reduce depth of cut before reducing speed.
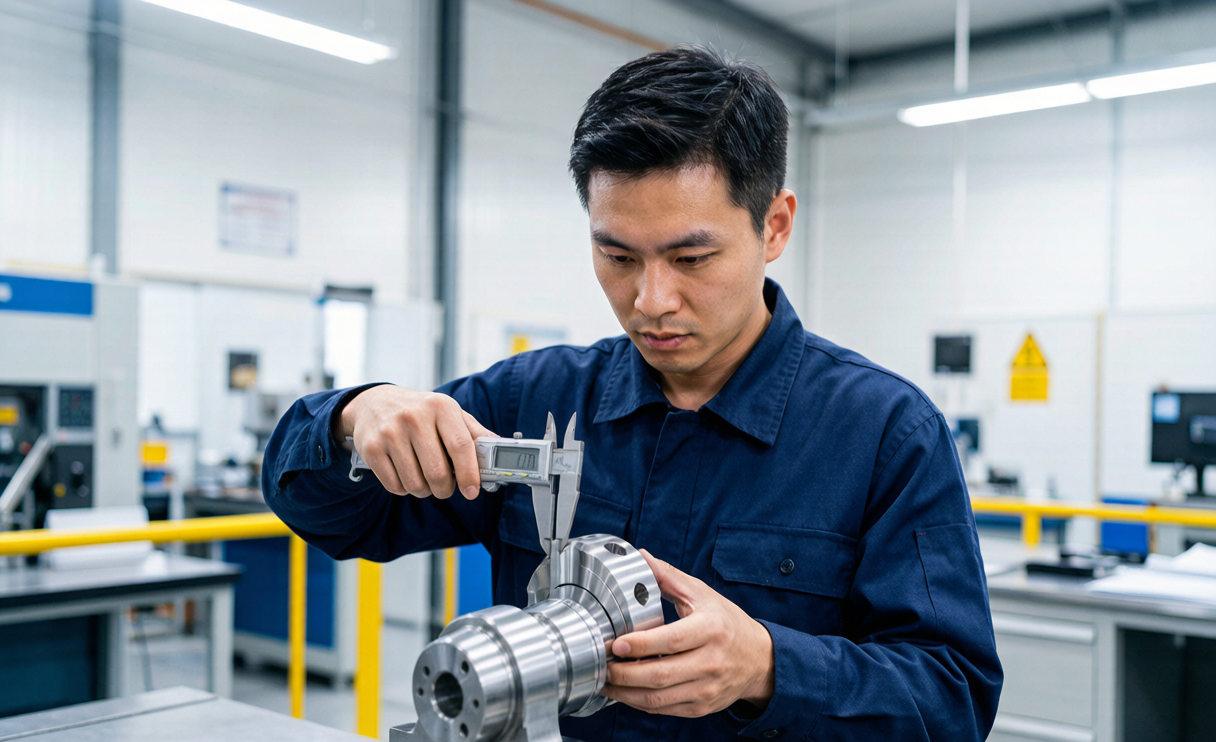
7. Quality Checks After Machining
- Measure dimensions after the part has cooled to room temperature.
- Inspect surface finish with a roughness gauge or comparison sample.
- Check for burrs and sharp edges, especially on cross-holes and slots.
- Verify hardness if the material certificate is unavailable.
FAQ
Why does my 1018 steel weld itself to the insert?
That is built-up edge. Increase cutting speed, use a sharper positive-rake insert, or apply more coolant.
Can I machine normalized C45 without annealing?
Yes. Normalized C45 machines well. Only hardened or quenched-and-tempered conditions require annealing or lower speeds.
What coolant concentration is best for carbon steel?
Start at 8% water-soluble oil and adjust based on rust prevention and sump life.
Do Chinese carbon steel bars machine consistently?
Reputable mills produce consistent chemistry and hardness. Always request a mill test certificate and verify sulfur content for free-machining grades.
Conclusion
Successful carbon steel machining starts with matching the grade to the cutting parameters. Low-carbon steels need sharp tools and chip control; medium-carbon steels offer a wide productive window; high-carbon steels demand lower speeds and tougher inserts. Use the tables above as starting points and refine based on your machine, tool, and surface-finish target.
Looking for machinable carbon steel bar or plate? Huaxia-Steel supplies 1018, 1045, S45C, S50C, and C45 with mill certificates and tight tolerances for CNC shops worldwide.
Related Images