Carbon Steel Pipe Hydrostatic Testing: Pressure, Time and Acceptance
Hydrostatic testing is the most common final validation for carbon steel pipe used in pressure service, fluid transport, and structural applications. Every buyer expects pipes to hold pressure, but few specify exactly how the test should be performed, how long the pressure must be held, and what leakage or deformation is acceptable. A poorly specified hydrotest is a common source of disputes: the supplier runs a 5-second pressure check and ships, while the end user expected a full ASTM or API hold time with calibrated gauges. This guide explains hydrostatic testing for carbon steel pipe in plain terms — pressure calculation, hold time, acceptance criteria, equipment, common failure modes, and what to write on the purchase order.
1. What Hydrostatic Testing Actually Proves
A hydrostatic test pressurizes the pipe with water to a level above the normal operating pressure and holds it for a defined time. The test does two things. First, it reveals gross defects — longitudinal seams, wall-thin areas, cracks, or defective welds — that cannot withstand the test pressure. Second, it demonstrates that the pipe assembly, including threaded or welded end connections, does not leak at the test pressure. It is a proof test, not a fatigue test or a corrosion test; it does not predict long-term behavior under cyclic loading.
2. How to Calculate Hydrostatic Test Pressure
The test pressure depends on the pipe specification, the specified minimum yield strength (SMYS), the wall thickness, and the outside diameter. The two most common formulas are the standard-specified pressure and the Barlow-derived pressure used in pipeline codes. For mill testing of individual pipes, the standard usually states a simple pressure value or a formula. For example, ASTM A53 and A106 use a test pressure of at least 60% of the specified minimum yield strength, applied based on the wall thickness.
| Specification | Test pressure basis | Hold time |
|---|---|---|
| ASTM A53 seamless/ERW | ≥ 60% of SMYS, min 700 psi unless waived | ≥ 5 seconds per standard, longer by agreement |
| ASTM A106 seamless | ≥ 60% of SMYS, min 700 psi unless waived | ≥ 5 seconds standard; 10–60 s common |
| API 5L line pipe | Standard pressure per size/grade, or hydrostatic design pressure × 1.25 | ≥ 10 seconds per pipe |
| EN 10216-2 P235GH | Test pressure = 20 MPa × t/D or per order | ≥ 5 seconds at test pressure |
| JIS G3454 STPG370 | Per standard table or 2.0 MPa minimum | ≥ 5 seconds |
The Barlow formula for thin-wall pipe is a useful sanity check: P = 2 × S × t / D, where P is the test pressure, S is the allowable stress (often 60% of yield for hydrotest), t is the nominal wall thickness, and D is the outside diameter. For example, a 6-inch Sch 40 A106 Gr B pipe with 7.11 mm wall, 168.3 mm OD, and SMYS of 240 MPa would have a theoretical test pressure near 60 MPa. The actual mill test pressure may be rounded down to the mill’s standard table, so always request the test pressure in writing.
3. Hold Time, Inspection, and Acceptance Criteria
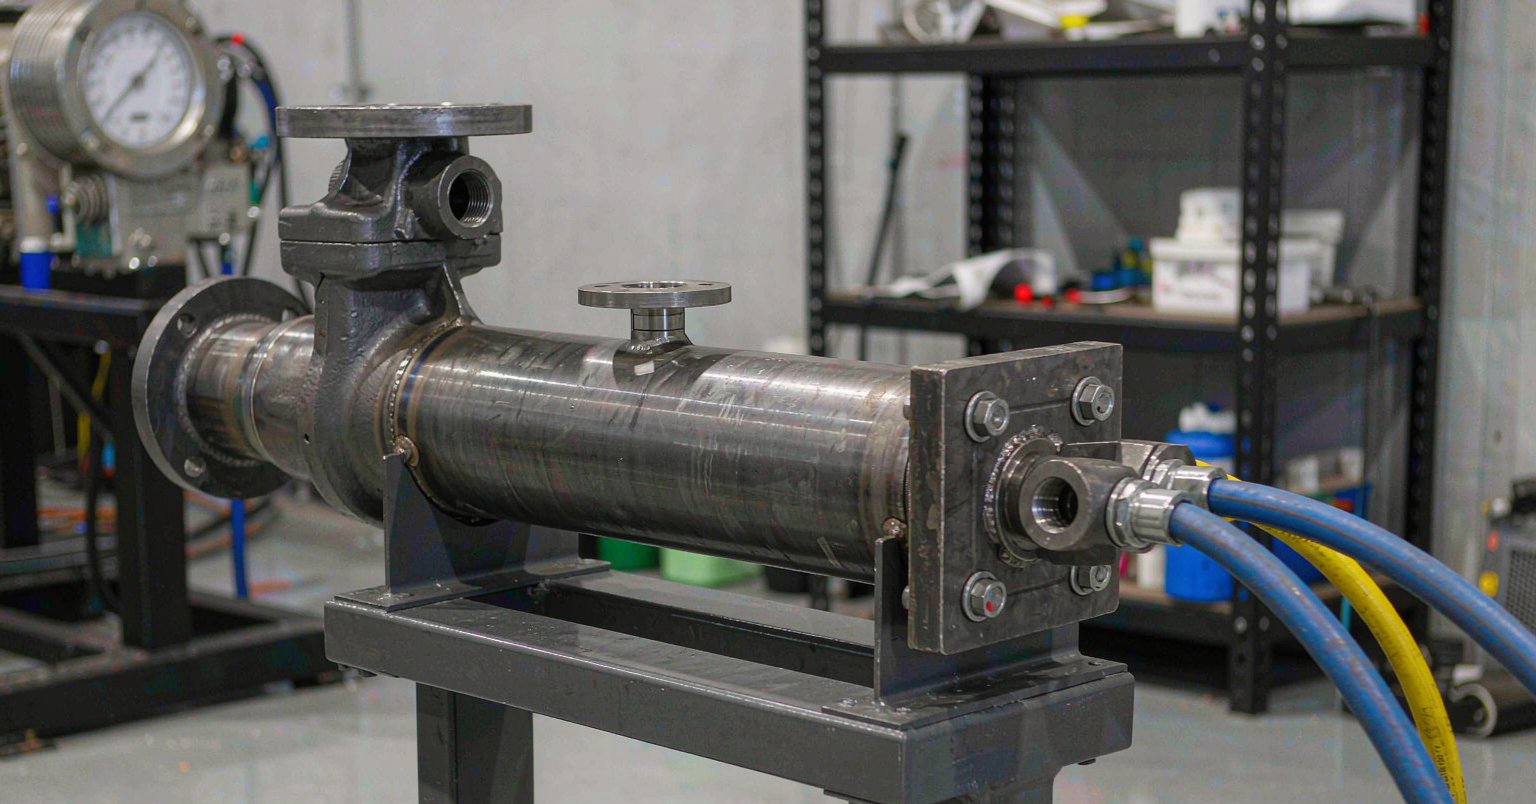
The standard minimum hold time is often only 5 seconds at pressure, which is enough to detect a catastrophic leak but not enough to observe slow weeping or stress relaxation. For critical service, buyers commonly specify 10 seconds, 30 seconds, or even several minutes. The pressure must remain stable within the gauge tolerance for the full hold time, with no visible leakage from the body, weld seams, or end connections.
4. Equipment and Calibration Requirements
A reliable hydrostatic test requires a pressure source, calibrated pressure gauge, calibrated relief valve, filled and vented pipe, and properly designed end caps. The most common source of false passes is an oversized or uncalibrated gauge. A gauge with 5% accuracy may mask a 3% pressure drop that indicates a leak. Best practice is to use two gauges — a master gauge and a field gauge — and to record both readings. Pressure gauges should be calibrated to national standards with current calibration stickers traceable to the certificate.
The test fluid should be clean water at a controlled temperature. Cold water in a warm pipe contracts during the test and can create the appearance of a pressure drop; hot water expands and can over-pressurize. Many specifications limit the water temperature to 5–50°C. After testing, pipes should be drained and dried to prevent internal corrosion, especially if they will be stored for more than a few days before shipment.
5. Common Failure Modes and What They Mean
| Failure sign | Likely cause | Disposition |
|---|---|---|
| Leak at longitudinal seam | Incomplete fusion, undercut, or wall-thin area in ERW or SAW pipe | Reject or repair per specification |
| Leak at threaded end | Poor thread cut, damaged thread, or insufficient thread engagement | Rework threads or replace pipe |
| Leak at girth weld of fabricated spool | Welding defect, hydrogen cracking, or fit-up issue | Repair weld with qualified WPS/PQR |
| Bulging or permanent expansion | Wall thickness below nominal or test pressure too high | Measure wall, verify D/t ratio, reduce pressure |
| General weeping through wall | Porous material, severe corrosion, or pinholes | Reject lot |
| Pressure drop without visible leak | Seal leak, trapped air, or thermal contraction | Re-vent, re-test, inspect seals |
6. Documentation Buyers Should Demand
A test certificate should not simply say “hydrotest passed”. At minimum, the certificate or report must include the test date, pipe heat and piece numbers, outside diameter and wall thickness, test pressure, hold time, gauge calibration reference, test medium temperature, and the inspector’s signature. For pressure equipment going into regulated service, the report should reference the applicable standard (ASTM, API, EN, or ASME) and include any customer-specified acceptance criteria. Without these details, the certificate is just a piece of paper.
Can the hydrotest pressure damage a good pipe?
If the pressure is within the specified test range and the pipe meets the nominal wall, no. Hydrotest pressure is designed to stay below the yield point of a sound pipe. However, if the wall is significantly below nominal or if the pipe has a large defect, the test may cause local yielding or rupture. That is the purpose of the test — to find the defect before the pipe leaves the mill.
Is air testing ever acceptable instead of water?
Air testing is rarely acceptable for carbon steel pressure pipe because compressed gas stores much more energy than water and can cause violent rupture. It is sometimes used for very small-diameter instrument tubing or for leak detection at low pressure after hydrostatic testing, but never as the primary proof test for process pipe.
What hold time should I specify on the purchase order?
For normal commercial pipe, specify 10 seconds at the standard test pressure. For critical service, specify 30 seconds to 2 minutes. Do not rely on the 5-second minimum in ASTM A53/A106 for high-value or safety-critical applications; the incremental cost is negligible and the quality signal is much stronger.
Do used or reconditioned pipes need a hydrotest?
Yes. Any pipe that has been cut, threaded, re-beveled, or repaired should be retested before reuse in pressure service. Cutting and threading can introduce stress risers and expose subsurface defects that were not present at the original test.
7. Specifying Hydrostatic Testing on Your Purchase Order
Order pipe with certified hydrostatic testing
Huaxia-Steel supplies ASTM A53, A106, API 5L, and EN carbon steel pipe with 100% hydrostatic testing, full test certificates, and customizable hold times. Request a quote with your pressure and test requirements.