Induction Hardening Carbon Steel: Process, Case Depth, Costs
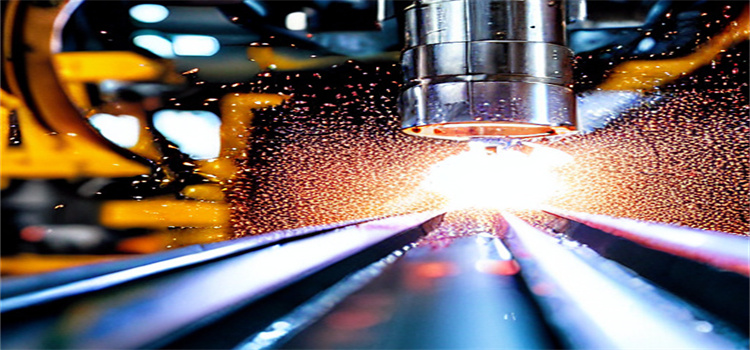
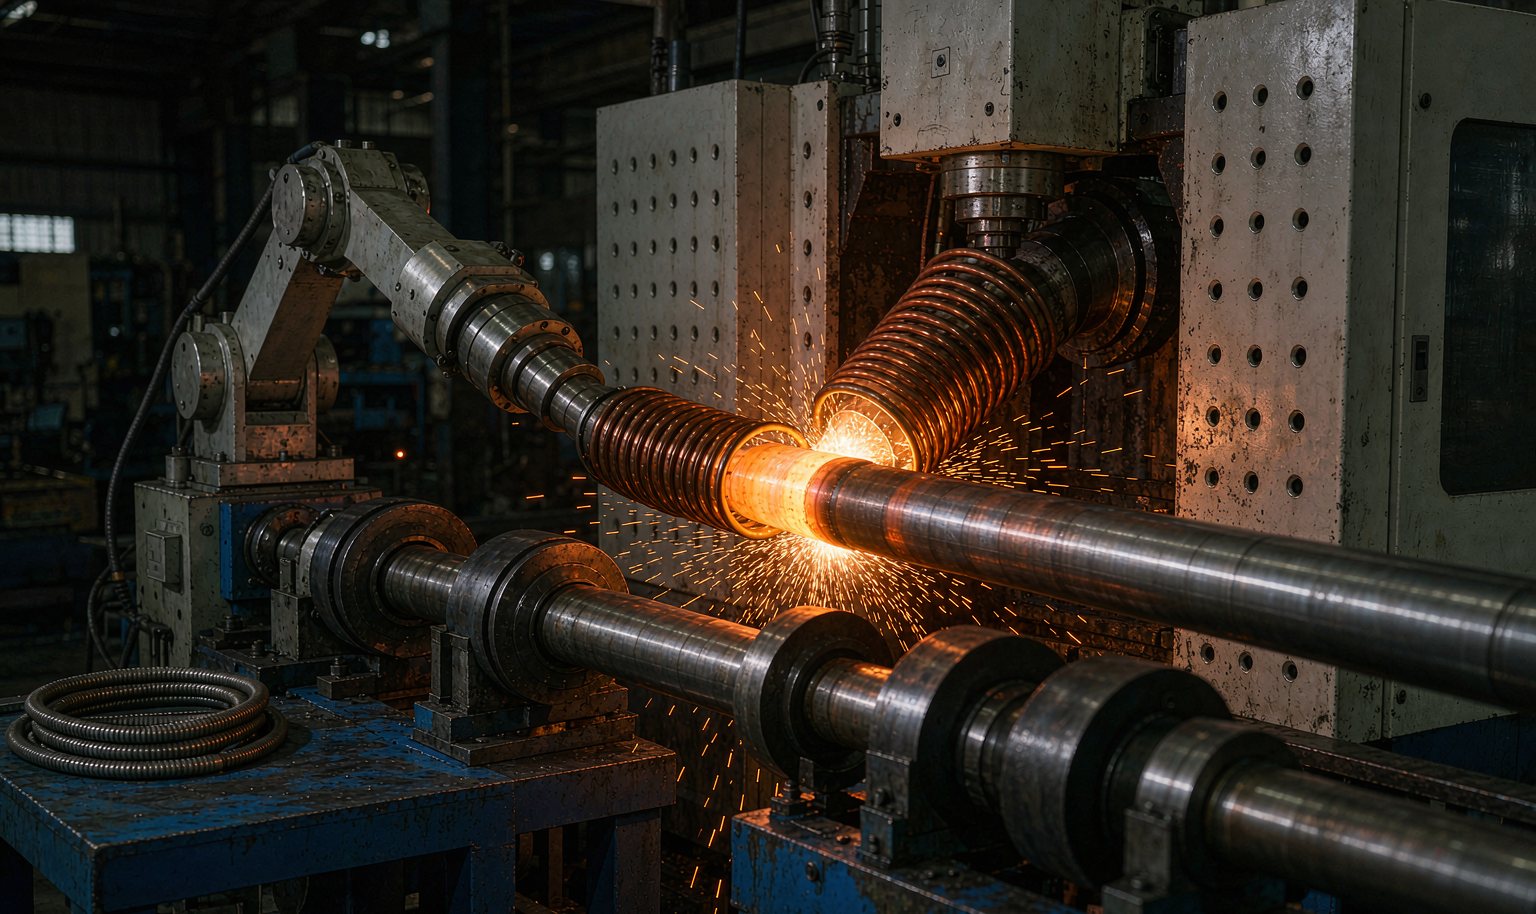
Induction hardening is the fastest, most controllable way to give a carbon steel part a hard, wear-resistant surface while keeping the core tough. Instead of heating the whole component in a furnace, an induction coil heats only the surface layer to austenitizing temperature in seconds, and a quench ring hardens it immediately. The result: surface hardness of 55–60 HRC on 1045, 4140, or C45 steel, with the case depth tuned from 0.5 mm to 6 mm. This guide explains how the process works, which steels respond best, how to specify case depth, what it costs, and the mistakes that cause field failures.
1. How Induction Hardening Works
The physics explains why the process is so efficient: only the surface layer ever reaches austenite, so energy consumption can be 60–90% lower than carburizing or through-hardening for the same part, cycle time drops from hours to seconds, and the core microstructure — and therefore the part’s toughness — is untouched.
2. Which Carbon Steels Respond Best
| Grade | Surface HRC (typ.) | Best Use | Notes |
|---|---|---|---|
| AISI 1045 / S45C / C45 | 55–58 | Shafts, spindles, pins | The volume grade; cheap and predictable |
| AISI 1050 / S50C | 57–60 | Wear rails, sprockets | Slightly higher hardness, more crack risk |
| AISI 4140 / 42CrMo4 | 56–60 | Heavy-duty shafts, gears | Deeper effective case at same cycle |
| AISI 4130 / 25CrMo4 | 52–56 | Welded-then-hardened parts | Lower max hardness, better toughness |
| 1045 induction + core Q&T | 55–60 skin | High-duty transmission shafts | Combine through-hardening + induction for top fatigue life |
| C40 / C45E (EN) | 54–58 | European-spec shafting | C45E for tighter S control |
The rule of thumb: the steel needs at least ~0.35% carbon to reach 55 HRC by induction hardening. Medium-carbon grades (0.40–0.50% C) are the sweet spot. Low-carbon steels (1018, A36) cannot induction harden usefully — their carbon content simply cannot form hard martensite, which is why those parts get carburized instead. Steels above 0.55% C reach very high hardness but quench-crack risk climbs steeply; if you must use them, polymer quench and rigorous pre-inspection are mandatory.
3. Specifying Case Depth Correctly
Case depth is where specifications go wrong most often, because there are two different definitions and suppliers quote whichever flatters them. Total case depth measures from the surface to where the microstructure matches the core. Effective case depth (ECD) measures to a defined hardness limit — conventionally the depth at which hardness drops to 50 HRC (or the “HRC 50” criterion per SAE J423). A shaft with 2.0 mm total case depth may have only 1.1–1.3 mm effective case depth.
4. The Fatigue Bonus: Compressive Residual Stress
Beyond wear resistance, induction hardening buys a major fatigue improvement. The martensitic transformation expands the surface layer by roughly 1–4%, but the tough core resists that expansion — the outcome is a compressive residual stress field of 400–800 MPa at the surface, exactly where bending and torsional stresses peak on a rotating shaft. Field data on transmission shafts routinely show fatigue life improvements of 2–5× versus the same part through-hardened to the same surface hardness. This is why heavily loaded shafts often get the combination treatment: Q&T the whole part for core strength, then induction harden the bearing journals and splines for surface durability.
5. Typical Distortion, Tolerances, and Post-Processing
| Item | Typical Value | Buyer Action |
|---|---|---|
| Roundness change after hardening | 0.02–0.10 mm on shafts ≤ 50 mm | Leave grind stock 0.3–0.5 mm on hardened diameters |
| Length change (scan-hardened shafts) | 0.05–0.3 mm per meter | Machine to size after hardening on tight-length parts |
| Straightness (press-corrected) | ≤ 0.05 mm/m achievable | Specify post-harden straightening + stress relief |
| Final surface finish | Ground Ra 0.4–0.8 µm | Order hardened + ground for bearing seats |
| Decarburization risk | Near zero (seconds at temperature) | Superior to furnace hardening on finish-machined parts |
Because heating is so fast, induction hardening is the preferred route for parts that are already finish-machined to near-size: there is no scale, no furnace-atmosphere decarb, and distortion stays small enough to correct with a light grind. The standard manufacturing sequence is: machine to within 0.3–0.5 mm of final size → induction harden specified journals → temper 170–220°C → straighten if needed → finish grind hardened surfaces → magnetic particle inspect (MPI) the critical areas.
6. Cost Drivers and Practical Economics
7. Common Failure Modes and How to Avoid Them
8. FAQ
Induction hardening vs carburizing — which should I choose?
If the steel is medium/high carbon, choose induction: faster, cheaper, less distortion, deeper cases available. Carburize low-carbon steels (8620, 1018) or when you need case hardening on a part with complex geometry that a coil cannot follow. Carburizing gives better control on gears with tight case-depth maps; induction wins on shafts, pins, and rollers.
Can I induction harden a part after welding?
Yes, and it is a common sequence — weld first, then locally harden. Keep the hardening pattern away from the weld HAZ, or the HAZ’s coarse grain may quench-crack. Post-weld stress relief before hardening is cheap insurance.
How deep can induction hardening go?
Practical effective case depths run 0.5 mm to about 6 mm. Beyond that, power and quench control get difficult and through-hardening or flame hardening becomes more economical. Most shaft specifications land between 1 and 3 mm ECD.
Does induction hardening affect corrosion resistance?
No meaningful effect — the case is still carbon steel. If the part needs corrosion protection, apply coating or plating after hardening and grinding, since heat from hardening would destroy most coatings.
What inspection documents should a supplier provide?
EN 10204 3.1 for the base material, a heat-treatment record (power, scan speed, quench medium), hardness traverse plot on the first article, and MPI results on critical lots. For high-volume safety parts, add a defined AQL sampling plan for surface hardness and case depth.
Source Induction-Hardening-Ready Bar and Shafts
Huaxia-Steel supplies 1045, S45C, C45, and 4140 bar in peeled, cold-drawn, and Q&T conditions — ideal feedstock for induction hardening, with EN 10204 3.1 certs and cut-to-length service.
Request a quote: Contact Huaxia-Steel.