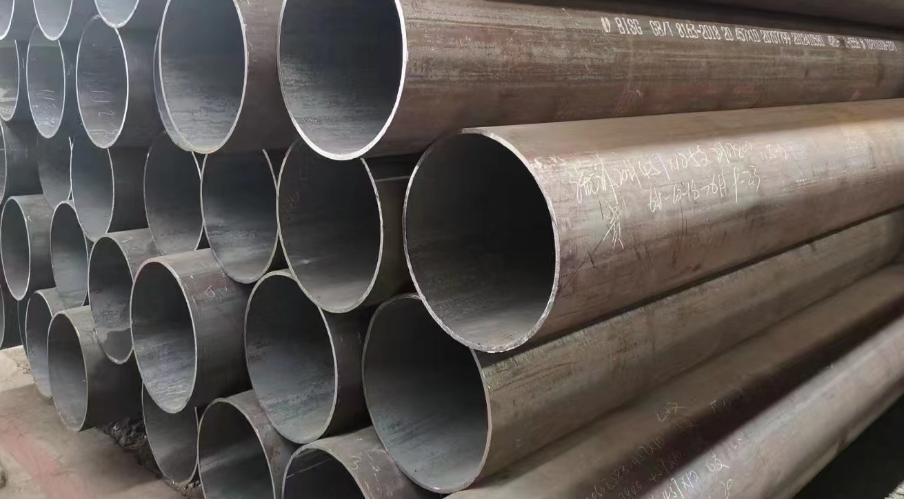
1215 free machining steel bar is the switch-over grade for high-volume turning shops that have hit the wall with 1018: a resulfurized, rephosphorized carbon steel to AISI/SAE 1215 (usually ordered to ASTM A29/A108) whose sulfur and phosphorus additions break chips, reduce cutting force and roughly double tool life on automatic lathes and CNC turning centers. It is not a structural grade — that is the trade-off — but where cycle time per part is the cost driver, 1215 pays for itself on the first shift. Huaxia-Steel supplies 1215 round bar from audited partner mills in cold drawn condition, with EN 10204 3.1 certificates, hex and square sections, and cut-to-length service for repeat production runs.
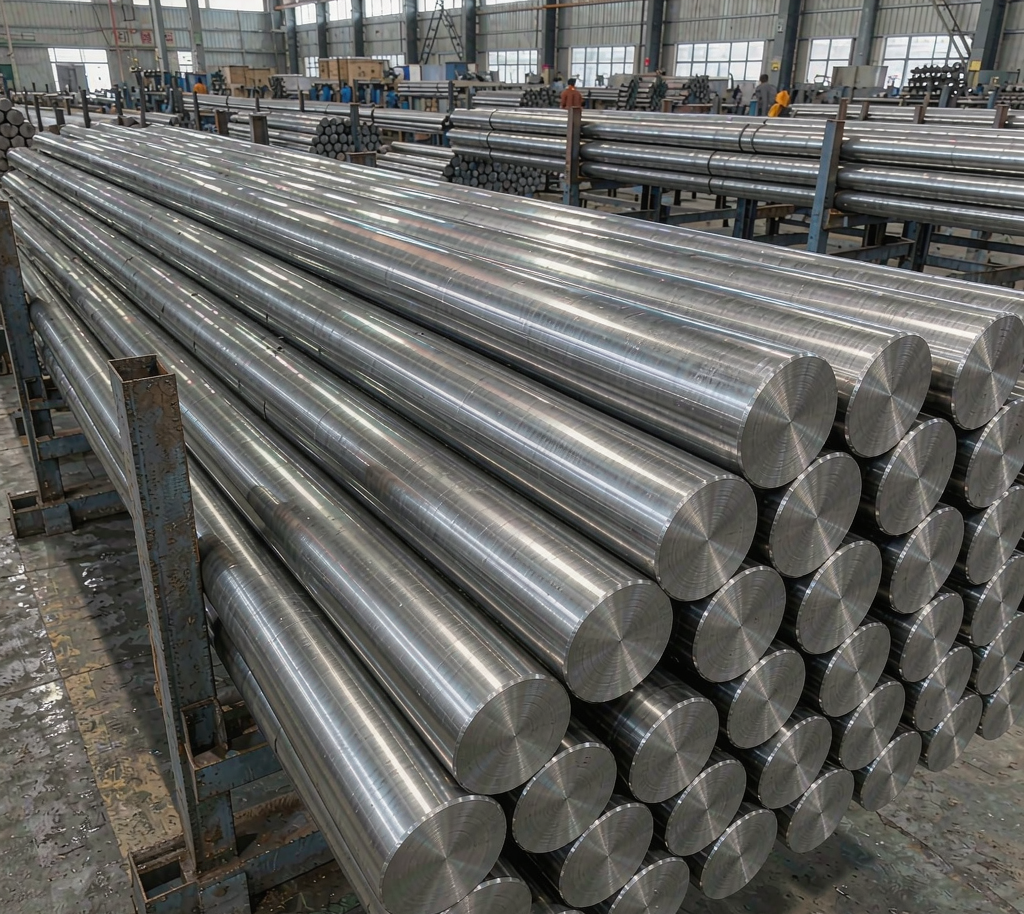
Product Overview
1215 is a plain-carbon free machining steel with carbon held low (≤ 0.09%) and sulfur raised to 0.26–0.35% with phosphorus to 0.04–0.09%. The manganese sulfides formed during solidification act as internal chip breakers and solid lubricants at the tool-chip interface. The practical result: better surface finish, tighter diameter control across long runs, and feed rates typically 20–40% higher than 1018 for the same tool life. Cold drawn 1215 also delivers a bright, scale-free surface with h9–h11 tolerance, so parts that would otherwise need turning-all-over can be machined from a single critical feature and finished. The grade is intended for machined hardware — fasteners, fittings, couplings, bushings — not for welded or load-critical structural components, since the sulfur stringers reduce transverse ductility and weldability.
- Designation: AISI/SAE 1215; supplied to ASTM A29/A29M (hot wrought) or A108 (cold finished bars).
- Near equivalents: 11SMn30 / 9SMn28 (EN 10087), SUM22 (JIS), Y15 (GB/T 8731).
- Conditions: cold drawn (most common), hot rolled, and turned-and-polished on request.
- Sections: round 3–80 mm, hex 6–60 mm A/F, square 6–50 mm.
- Certificates: EN 10204 3.1 with chemistry per heat and mechanical data per lot.
Specifications: Dimensions, Weight and Tolerance
| Parameter | Cold drawn round | Hot rolled round |
|---|---|---|
| Diameter range | 3–80 mm | 16–120 mm |
| Tolerance class | h9 / h10 / h11 (per GB/T 1803 or ASTM A108) | ±0.4–1.0 mm (per GB/T 702) |
| Straightness | ≤ 1 mm/m | ≤ 3 mm/m |
| Surface finish | Bright, Ra ≤ 1.6 µm typical | Mill scale |
| Standard length | 3000–6000 mm, cut-to-length ±2 mm | 6000 mm |
| Weight per meter | W = 0.00617 × d² kg/m (d in mm): Ø25 = 3.86 kg/m, Ø50 = 15.4 kg/m | |
| Out-of-roundness | ≤ 50% of diameter tolerance | Within diameter tolerance |
Chemical Composition (AISI 1215)
| Element | Content | Role |
|---|---|---|
| Carbon (C) | ≤ 0.09% | Low carbon keeps the core soft and ductile |
| Manganese (Mn) | 0.75–1.05% | Combines with sulfur into MnS inclusions |
| Sulfur (S) | 0.26–0.35% | Chip breaking, lower cutting force |
| Phosphorus (P) | 0.04–0.09% | Improves finish on light cuts |
| Silicon (Si) | ≤ 0.10% | Kept low to avoid tool abrasion |
| Lead (Pb) | 0.15–0.35% (12L14 variant) | Extra lubricity; not in 1215 |
1215 vs 12L14: both are free machining grades, but 12L14 contains 0.15–0.35% lead, which further improves machinability and gives slightly better surface finish at very high speeds. Lead-free 1215 is chosen where RoHS/ELV restrictions or environmental documentation make lead unacceptable — increasingly the default for European and automotive-adjacent supply chains. Machinability rating is ~135% vs 100% for 1212 and ~160% for 12L14, using 1212 as the 100% reference in the AISI rating system (note: ratings are indexed to 1212, so a 1215 figure of 135 means 35% better than the 1212 benchmark, not 35% better than 1018).
Mechanical Properties
| Property | Cold drawn | Hot rolled |
|---|---|---|
| Tensile strength | ≥ 540 MPa | ≥ 400 MPa |
| Yield strength | ≥ 415 MPa | ≥ 280 MPa typical |
| Elongation (50 mm) | ≥ 10% | ≥ 22% |
| Hardness | 163–190 HB typical | 120–145 HB typical |
| Machinability rating | ~135% (AISI scale, 1212 = 100%) | |
Cold drawing raises strength and improves tolerance but reduces ductility — the elongation minimum of 10% in cold drawn 1215 is roughly half that of hot rolled. For parts that will be crimped, swaged or heavily cold formed after machining, order hot rolled or a low-carbon alternative and accept the slower cutting speeds.
Manufacturing Standards
- ASTM A29/A29M: general requirements for hot wrought carbon and alloy steel bars (chemistry, test methods).
- ASTM A108: standard for cold finished carbon steel bars, covering dimensional tolerance and finish.
- GB/T 8731 (Y15) and EN 10087 (11SMn30) equivalents available for customers quoting Chinese or European drawings.
- Production route: BOF/EAF melting with controlled sulfur addition, continuous casting, hot rolling, then pickling, drawing and straightening for cold finished.
- Traceability: heat number per bundle tag, matched to the EN 10204 3.1 certificate.
Typical Applications
- Lathe-turned hardware: nuts, bolts, standoffs, spacers, pins, studs.
- Hydraulic and pneumatic fittings, adapters, couplings and hose nipples.
- Bushings, collars, sleeves and shaft spacers machined from bar.
- Electrical and appliance components where finish matters more than strength.
- High-volume screw machine parts on multi-spindle automatics.
Not suitable for: welded assemblies (sulfur causes porosity and hot cracking), high-fatigue shafts, structural load parts, and anything requiring heat treatment to high hardness — 1215’s low carbon cannot be quenched to usable hardness. For those, specify 1045, 4140 or 12L14 with a lead-compliant waiver.
Quality Assurance and Inspection
Standard QA package: EN 10204 3.1 certificate with heat chemistry and mechanical test results, diameter and straightness verification against the ordered tolerance class, surface inspection of bright bar for draw marks and laps, and bundle-level traceability. Optional services: spectrometer re-verification at our warehouse, third-party inspection (SGS/BV/TUV), chip-break-free surface finish measurement, and trial bars cut to your machine’s chuck length for a run-off before bulk shipment. Because free machining performance is a process property, we recommend a first-article trial on any new diameter — ask for a 50–100 kg sample with certificate.
Packing and Shipping
Cold drawn bright bar is end-capped, bundled at 1–2 t with steel strapping, wrapped in VCI paper and plastic film, and shipped in containers on wooden skids or in seaworthy wooden cases for small diameters and hex/square sections. Each bundle carries heat number, size, grade and net weight tags matching the packing list; a 20 ft container typically loads 24–26 t. Documents: commercial invoice, packing list, 3.1 certificates, COO on request, and a lead-free declaration confirming 1215 contains no added lead — useful documentation for RoHS and ELV compliance files.
Corrosion Protection and Storage
1215 has no corrosion advantage over mild steel and, because the manganese sulfide inclusions sit at the surface, bright bar can show fine surface staining sooner than low-sulfur grades in humid conditions. Cold drawn bar ships oiled and VCI-wrapped for export; keep the wrapping intact until the bars are staged at the machine, store indoors with timber or rubber separation from the floor, and re-oil long stock that will sit more than a few weeks. Parts machined from 1215 are normally protected like any carbon steel part — oil, phosphate, zinc plating or black oxide depending on the application. Note that zinc plating on high-sulfur steel occasionally shows uneven coverage on complex geometry; a brief cyanide-free activation step in the plating line handles it, so inform your plater that the substrate is a free machining grade.
Machining Parameters and Tooling Tips
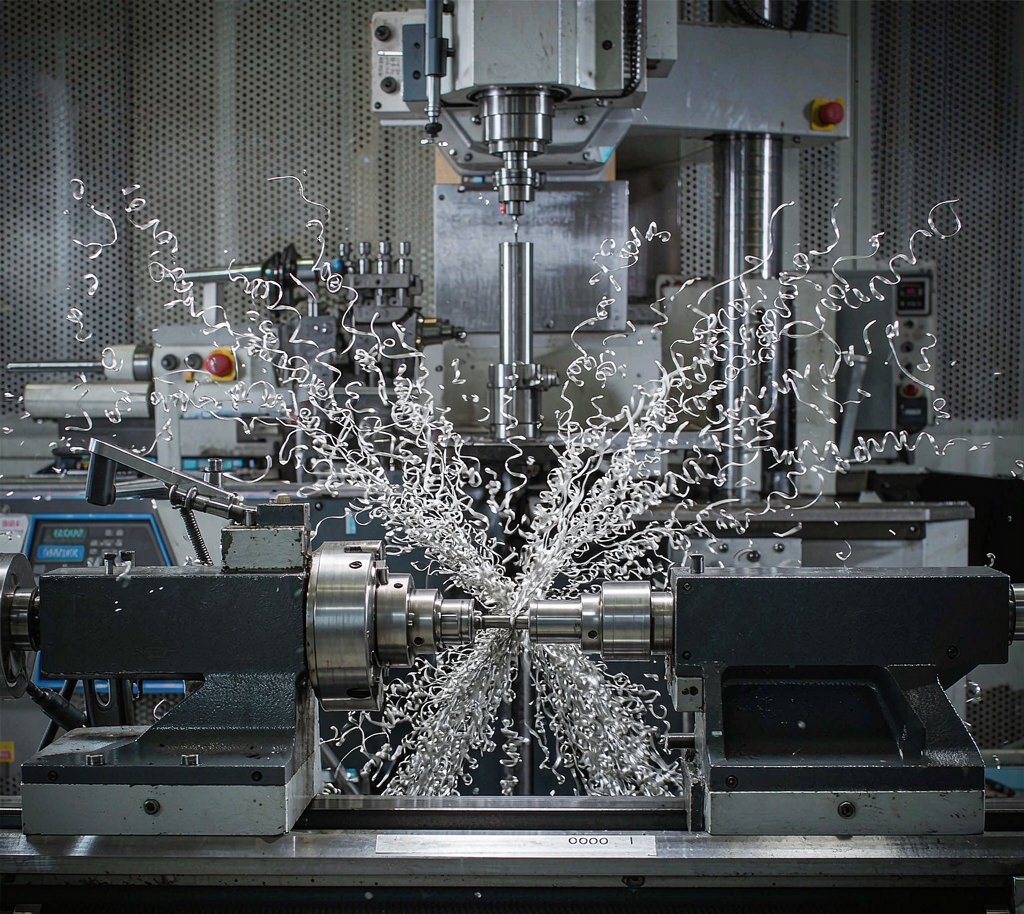
1215 is forgiving, but the free machining benefit only appears at the right speeds and with the right chip control. Starting parameters for carbide turning on cold drawn 1215: cutting speed 180–260 m/min, feed 0.10–0.25 mm/rev, depth of cut up to 3 mm, with sharp positive-rake geometry and no chip breaker needed for most operations — the MnS inclusions break the chip for you. On high-speed automatics, 12L14 runs faster still, but 1215 reaches roughly 85% of that output with no lead-handling documentation. For drilling and tapping, 1215 gives excellent tap life and clean threads; expect 20–35% higher feed than 1018 at the same tool wear.
- Use sharp tools: a worn edge smears rather than cuts the sulfide stringers and degrades finish.
- Coolant is about chip evacuation and heat, not lubrication — the sulfides already lubricate; flood coolant keeps dimensional control tight on long runs.
- Surface finish of Ra 0.8–1.6 µm is routine on finishing passes without polishing.
- Threading and knurling are where 1215 shines: clean root geometry, no built-up edge.
- Welding: avoid. The 0.26–0.35% sulfur causes porosity and solidification cracking; specify 1018 or 12L14 with post-weld qualification if welding is unavoidable.
- Heat treatment: not applicable for hardening; the low carbon ceiling means case hardening (carburizing) is the only thermal route to a hard surface, and it is rarely worth it on a grade chosen for machining speed.
Ordering Checklist
- Grade and standard: AISI/SAE 1215 to ASTM A29 (hot wrought) or A108 (cold finished); state EN 10087 11SMn30 or GB/T 8731 Y15 if quoting to those documents.
- Section and size: round, hex or square with the exact across-flats or diameter.
- Tolerance class: h9 / h10 / h11 for cold drawn; state the class — do not assume.
- Condition: cold drawn (standard), hot rolled, or turned-and-polished for special finishes.
- Length: 3000–6000 mm or cut-to-length to your chuck specification at ±2 mm.
- Certification: EN 10204 3.1 with heat chemistry and mechanical results; lead-free declaration if required for RoHS/ELV files.
- Packing: VCI, end caps, wooden cases for small sizes.
- Commercial: Incoterm, port, validity, payment terms, lead time and rejection remedy.
Why Buy 1215 From Huaxia-Steel
- Factory-direct pricing from audited free machining steel mills, one certificate chain per heat.
- Cold drawn round, hex and square, cut to length with ±2 mm accuracy.
- Lead-free composition documented for RoHS/ELV supply chains.
- EN 10204 3.1 certificates with full chemistry and mechanical data as standard.
- Quotation within 24 hours, FOB/CIF/DDP flexible terms, small trial quantities accepted.
Send your diameter, section, tolerance class and monthly volume for a same-day quotation — or request a sample bundle with certificate to run a machining trial on your own machines before committing production volume.