Carbon Steel Anchor Bolts — Factory Direct Supplier | Huaxia-Steel
Huaxia-Steel manufactures carbon steel anchor bolts from M12 to M72 (½" to 2¾") in L-type, J-type, straight-with-plate and threaded-rod-with-nut configurations, certified to ASTM F1554 Grades 36, 55 and 105, with EN 10204 3.1 certificates and full lot traceability. Anchor bolts are the structural connection between steel columns and concrete foundations — their failure mode is embedment pullout or thread stripping, not shank breakage — so we control thread geometry, galvanizing thickness and material certification as strictly as the steel grade itself.
Product Overview
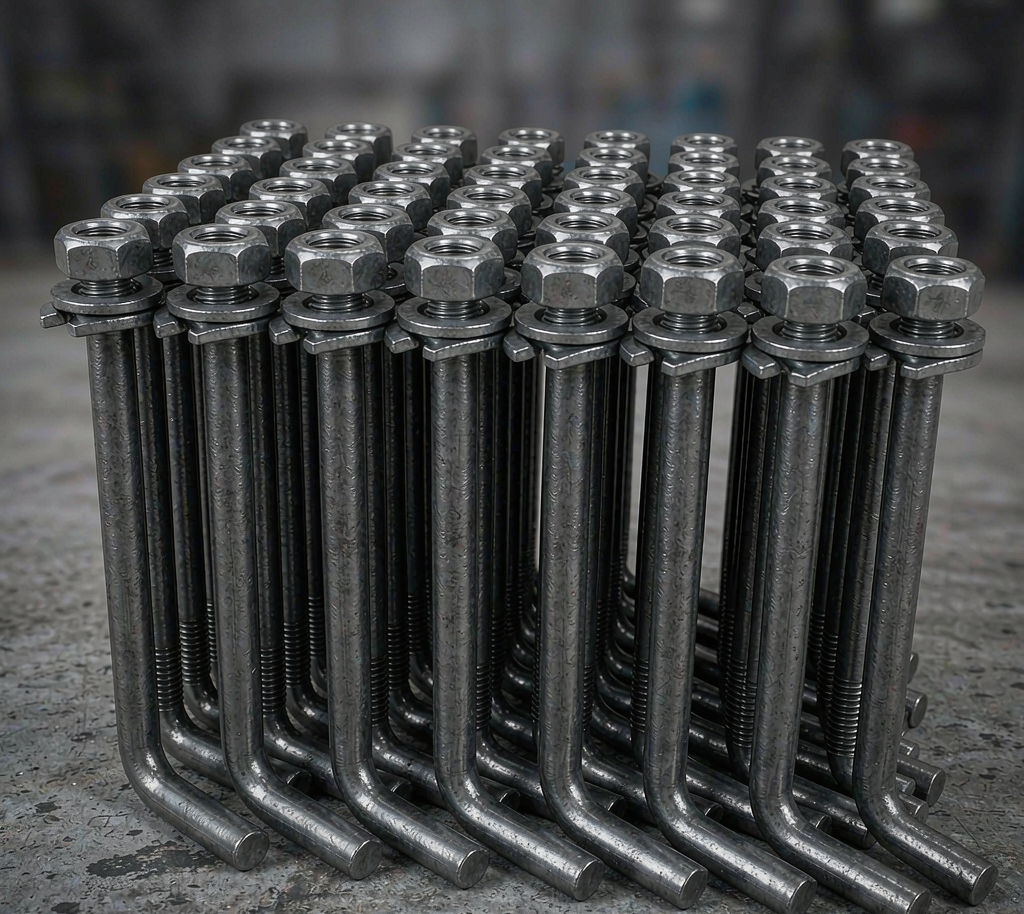
Our anchor bolt line covers the four configurations most specified on structural drawings: bent-bar L and J anchors cast into concrete; straight rods with a hex nut and washer at the embedded end for template-set installations; and headed studs for moment connections. Bars are hot-rolled or cold-drawn depending on grade, threads are rolled (not cut) for superior fatigue life and galvanizing adhesion, and every bolt ships with matched heavy hex nuts and washers. Projects requiring templates, double-nut levelling sets or shop-welded anchor plates are quoted and fabricated to your detail drawings.
Specifications
| Parameter | Details |
|---|---|
| Diameter range | M12–M72 metric; ½"–2¾" imperial |
| Length range | 300 mm to 6,000 mm single-piece |
| Grades | ASTM F1554 Gr 36 / Gr 55 / Gr 105; A36; S235JR/JR0; Q355B on request |
| Configurations | L-hook, J-hook, straight + heavy hex nut & washer, headed, template sets |
| Threads | Rolled UNC 2A / 8UN per ASME B1.1, or metric 6g per ISO 965; rolled before galvanizing |
| Coatings | Hot-dip galvanized per ASTM A153 Class C; mechanical galvanizing; plain/black oiled |
| Nuts & washers | A563 DH heavy hex; F436 hardened washers, galvanized as matched sets |
| Certification | EN 10204 3.1 MTC with chemistry, tensile and (Gr 55) bend test |
Reference Dimensions and Weights
| Size | Hook length L (typical) | Weight per 100 mm shank | Nut size (heavy hex) |
|---|---|---|---|
| M16 | 64 mm | 0.158 kg | M24 |
| M24 | 96 mm | 0.355 kg | M36 |
| M36 | 144 mm | 0.799 kg | M55 |
| M48 | 192 mm | 1.42 kg | M73 |
Embedment length, hook projection and thread length follow your structural drawings; where drawings are silent we default to 25 × diameter embedment for L/J hooks and project 3 × diameter plus 2 nut heights of thread above the leveling nut. Tolerances on projection (the dimension that drives steel erection) are held to ±5 mm; we recommend stating tighter projection tolerance on the PO if your anchor bolt templates demand it.
Available Grades and Materials
- F1554 Gr 36: 250 MPa yield, weldable — the standard for cast-in bent anchors.
- F1554 Gr 55: 380 MPa yield, bend-tested, supplied straight with nuts — today’s most-specified grade.
- F1554 Gr 105: 720 MPa yield quenched-and-tempered for high-uplift towers and cranes.
- S235JR / Q355B: for projects designed to ISO/Eurocode materials with CE marking needs.
Manufacturing Standards and Quality Assurance
Bolts are produced from billet-sourced bar with heat traceability from melt to shipment. Threads are rolled after straightening and before any coating; galvanized sets are spun and cooled to avoid thread flooding, and each nut is provided overtapped per A563 to preserve fit. QA per lot includes tensile testing to failure, hardness, thread gauge verification (GO/NO-GO), and bend testing for Gr 55. Certificates quote chemistry, yield, tensile, elongation and reduction of area, and galvanized lots include coating-thickness reports per ASME B1.20.3-style gauging practice for galvanized threads.
Applications
- Steel building and warehouse column base plates
- Transmission line and telecom towers (Gr 105 uplift connections)
- Crane rails, machine skids and equipment foundations
- Bridgeworks, light poles, sign structures and solar tracker arrays
Installation Notes: Templates, Projection and Torque
Anchor bolt problems on site almost always trace to three controllable items. First, use setting templates: bolts placed individually drift beyond the ±5 mm projection tolerance and the base plate holes will not drop over them — a template holding both projection and bolt-circle spacing eliminates the majority of erection delays. Second, protect the threads during the concrete pour with caps or tape; galvanized threads caked with grout damage nut fit and coating integrity at the same time. Third, torque to the project specification after the grout is placed and re-check at final tightening: a double-nut arrangement (levelling nut under the base plate plus top nut) lets the crew set elevation precisely before grouting. If your drawings show slip-critical or cyclically loaded connections, ask us for the recommended torque values for each diameter and grade — torque scales with grade, so a Gr 105 bolt is not tightened like a Gr 36 bolt of the same size.
Packaging and Delivery
Anchor bolts are bundled by size and mark with galvanized sets bagged with their nuts and washers, each bundle tagged to your drawing mark numbers for site sorting. Threads are protected with caps or tape; long bolts ship straightened on steel-reinforced pallets to prevent transit bends. Stock F1554 Gr 55 sizes ship in 5–7 days; project quantities and special marks run 15–25 days with template fabrication included.
Request an Anchor Bolt Quote
Send your anchor bolt schedule or drawing marks to [email protected] — we quote with grade, coating and template options itemized, and ship matched nut/washer sets on every order.