Carbon Steel Eccentric Reducer — Factory Direct Supplier | Huaxia-Steel
Huaxia-Steel supplies carbon steel butt-weld eccentric reducers from 1/2" × 3/8" up to 48" × 24", in SCH 10 through SCH 160 and STD/XS/XXS walls, manufactured from ASTM A234 WPB seamless and welded pipe per ASME B16.9, with EN 10204 3.1 certification on every delivery. The eccentric reducer’s offset profile — one straight side, one sloped side — keeps pipe racks at a constant elevation and prevents gas pockets at pump suctions, which is why it is the default choice on horizontal lines that change diameter. All fittings are bevel-prepared per ASME B16.25 for immediate field fit-up.
Product Overview
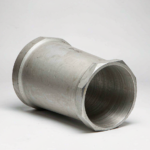
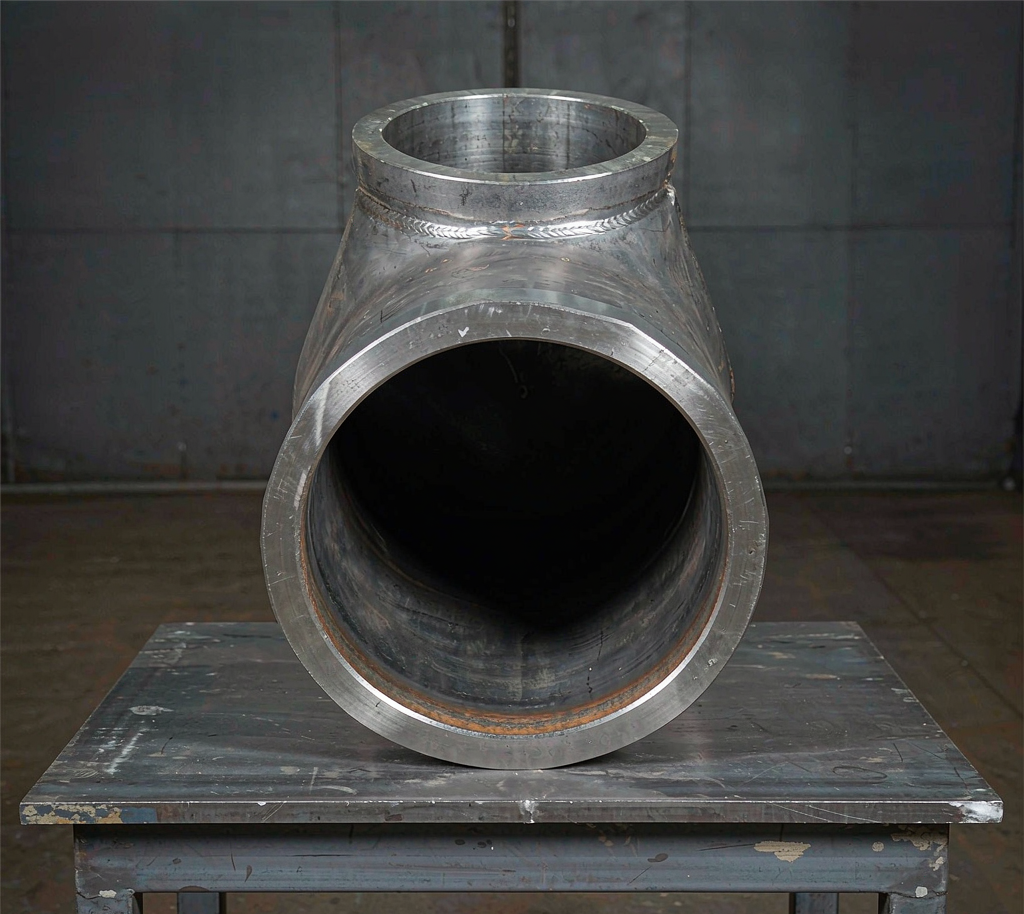
Where a concentric reducer changes size symmetrically, an eccentric reducer shifts one side of the flow path to stay flush with the adjacent pipe. Laid with the flat side up on pump suction lines, it prevents the air accumulation that causes pump cavitation; laid flat-side-down under pipe racks, it keeps support steel and racks level while the pipe diameter changes. Our eccentric reducers are hot-formed from seamless shell or pressed from plate and welded (seam position documented), then calibrated, beveled and marked per B16.9. Equal-wall matching with the connecting pipe, smooth internal transition and tight ovality tolerances are what separate a B16.9 fitting from a commodity pressing — and that is exactly what our inspection program certifies.
Specifications
| Parameter | Details |
|---|---|
| Size range | 1/2" × 3/8" to 48" × 24" (DN15×DN10 to DN1200×DN600) |
| Wall schedule | SCH 10/20/30/40/80/120/160, STD, XS, XXS |
| Manufacture | Seamless (hot-formed) or welded (plate-formed, seam per B16.9 rules) |
| Grades | ASTM A234 WPB (standard); A420 WPL6 (low temp); A860 WPHY 52/60 (line pipe) |
| Standard | ASME B16.9 dimensions and tolerances; bevel per ASME B16.25; MSS SP-75 for WPHY grades |
| End preparation | 37.5° bevel, 1.6–2.2 mm root face; special bevels on request |
| Testing | Hydroproof on request; surface MT; UT on heavy walls; EN 10204 3.1 MTC standard |
| Marking | Grade, size × wall, heat number, B16.9, manufacturer symbol — paint or low-stress stamp |
Reference Dimensions and Weights
| Size (OD × OD) | Length H (mm) | Offset E (mm) | Weight STD (kg) |
|---|---|---|---|
| 2" × 1" (60.3 × 33.4) | 51 | 13.4 | 0.8 |
| 4" × 2" (114.3 × 60.3) | 102 | 27.0 | 3.2 |
| 6" × 4" (168.3 × 114.3) | 140 | 27.0 | 6.4 |
| 10" × 8" (273 × 219.1) | 178 | 27.0 | 16.2 |
| 16" × 12" (406.4 × 323.9) | 241 | 27.0 | 38.0 |
| 24" × 16" (610 × 406.4) | 305 | 27.0 | 86.0 |
ASME B16.9 tolerances that matter most on site: ±1.6 mm on outside diameter at the bevel for small sizes scaling to ±4 mm at 48"; ±2.5 mm on overall length H through 24"; and a 1 % maximum ovality at the weld ends. The offset dimension E grows with the reduction ratio — confirm E against your rack geometry when large reductions are specified, and tell us the flat-side-up or flat-side-down orientation your piping design assumes.
Available Grades and Materials
- ASTM A234 WPB: the standard carbon steel grade for B16.9 fittings, ambient service.
- ASTM A420 WPL6: Charpy-tested to −46 °C for low-temperature installations.
- ASTM A860 WPHY 52/60: high-yield fittings matching API 5L X52/X60 pipelines (MSS SP-75).
- Anti-corrosion: FBE, 3LPE and shop primer coating coordinated with your pipeline spec.
Manufacturing Standards and Quality Assurance
Seamless reducers are formed by hot pushing or pressing over a mandrel at 850–1,000 °C, then normalized; welded reducers are die-formed from plate with the longitudinal seam radiographed or UT-tested per the material specification. Every fitting passes dimensional gauging (OD at ends, length, offset, ovality), visual and surface inspection, and hardness per heat. For heavy walls we perform straight-beam UT of the transition zone. Each shipment includes an EN 10204 3.1 certificate; 3.2 with third-party witness (SGS/BV/TUV) and hydroproof or PMI extensions are quoted on request for export projects.
Applications
- Pump suction lines (flat side up) to prevent air locking and cavitation
- Pipe rack headers (flat side down) to keep constant support elevation
- Refinery and petrochemical process headers, manifolds and tie-ins
- Power plant feedwater and condensate systems, HVAC main lines
Orientation Checklist for Designers and Installers
Before releasing the fitting purchase, confirm three orientation decisions. Pump suction: eccentric reducer flat side up, so entrained gas does not collect at the high point above the impeller; the exception is suction-from-below service where flat side down avoids a sludge trap. Pipe racks and sleepers: flat side down so the pipe bottom stays at a constant elevation and standard support heights apply. Instrument take-offs: keep the reducer orientation consistent with the sampling or drain points on the upstream drawings, because flipping the fitting changes the position of the low point where condensate collects. Marking the required orientation on the purchase order also speeds receiving inspection — our packers can ship flat-side-up fittings tagged and boxed together so crews grab the right part without second-guessing the drawing on site.
Packaging and Delivery
Fittings are bevel-protected with plastic caps or ring guards, packed in plywood or steel-framed crates with separation battens, and tagged per item with heat numbers for receiving reconciliation. Common sizes (A234 WPB, STD/XS) ship from stock in 5–7 days; large-bore or specialty grades run 20–35 days. Containerized mixed loads — reducers with elbows, tees and flanges — are consolidated with a single packing list and inspection report.
Request an Eccentric Reducer Quote
Send size × wall, grade and orientation note to [email protected] — B16.9 dimensional sheets, MTC samples and mill-direct pricing returned within 24 hours.