4130 vs 4140 Steel: Which Alloy Should You Specify?
4130 and 4140 are the two most requested low-alloy steels in export RFQs, and they get confused constantly — partly because their names look similar, and partly because traders sometimes quote one while delivering the other. They are not interchangeable, though: the 0.20% extra carbon in 4140 changes hardenability, achievable strength, weldability, and cost. This guide compares 4130 vs 4140 across chemistry, mechanical properties, heat treatment response, weldability, machining, applications, and price, so you can specify the right grade the first time.
1. Quick Answer: When to Use Each Grade
2. Chemical Composition Compared
| Element | 4130 (%) | 4140 (%) |
|---|---|---|
| Carbon | 0.28–0.33 | 0.38–0.43 |
| Manganese | 0.40–0.60 | 0.75–1.00 |
| Silicon | 0.15–0.35 | 0.15–0.35 |
| Chromium | 0.80–1.10 | 0.80–1.10 |
| Molybdenum | 0.15–0.25 | 0.15–0.25 |
| Phosphorus max | 0.035 | 0.035 |
| Sulfur max | 0.040 | 0.040 |
Notice that manganese also differs — 4140 carries 0.75–1.00% Mn against 0.40–0.60% in 4130. Combined with the higher carbon, this pushes 4140’s carbon equivalent (CEV) to roughly 0.75–0.85 versus 0.55–0.65 for 4130, which is the metallurgical reason 4140 demands preheat and low-hydrogen practice when welded while 4130 tolerates a milder procedure. The chromium and molybdenum additions in both grades do the same jobs: Cr lifts hardenability and adds a measure of wear and oxidation resistance; Mo refines grain, suppresses temper embrittlement, and maintains strength at moderately elevated temperature.
3. Mechanical Properties: What the Extra Carbon Buys
| Condition | Property | 4130 (typ.) | 4140 (typ.) |
|---|---|---|---|
| Normalized | Tensile strength | 670–700 MPa | 950–1020 MPa |
| Normalized | Yield strength | 435–450 MPa | 655–680 MPa |
| Q&T (moderate temper) | Tensile strength | 850–1000 MPa | 1000–1200 MPa |
| Q&T (low temper) | Tensile strength max | ~1200 MPa | 1400–1600+ MPa |
| Q&T typical delivery | Hardness | 22–28 HRC | 28–32 HRC (up to 38) |
| Water-quench surface | Max hardness | 50–53 HRC | 55–58 HRC |
| Elongation (Q&T) | A5d | 15–20% | 12–15% |
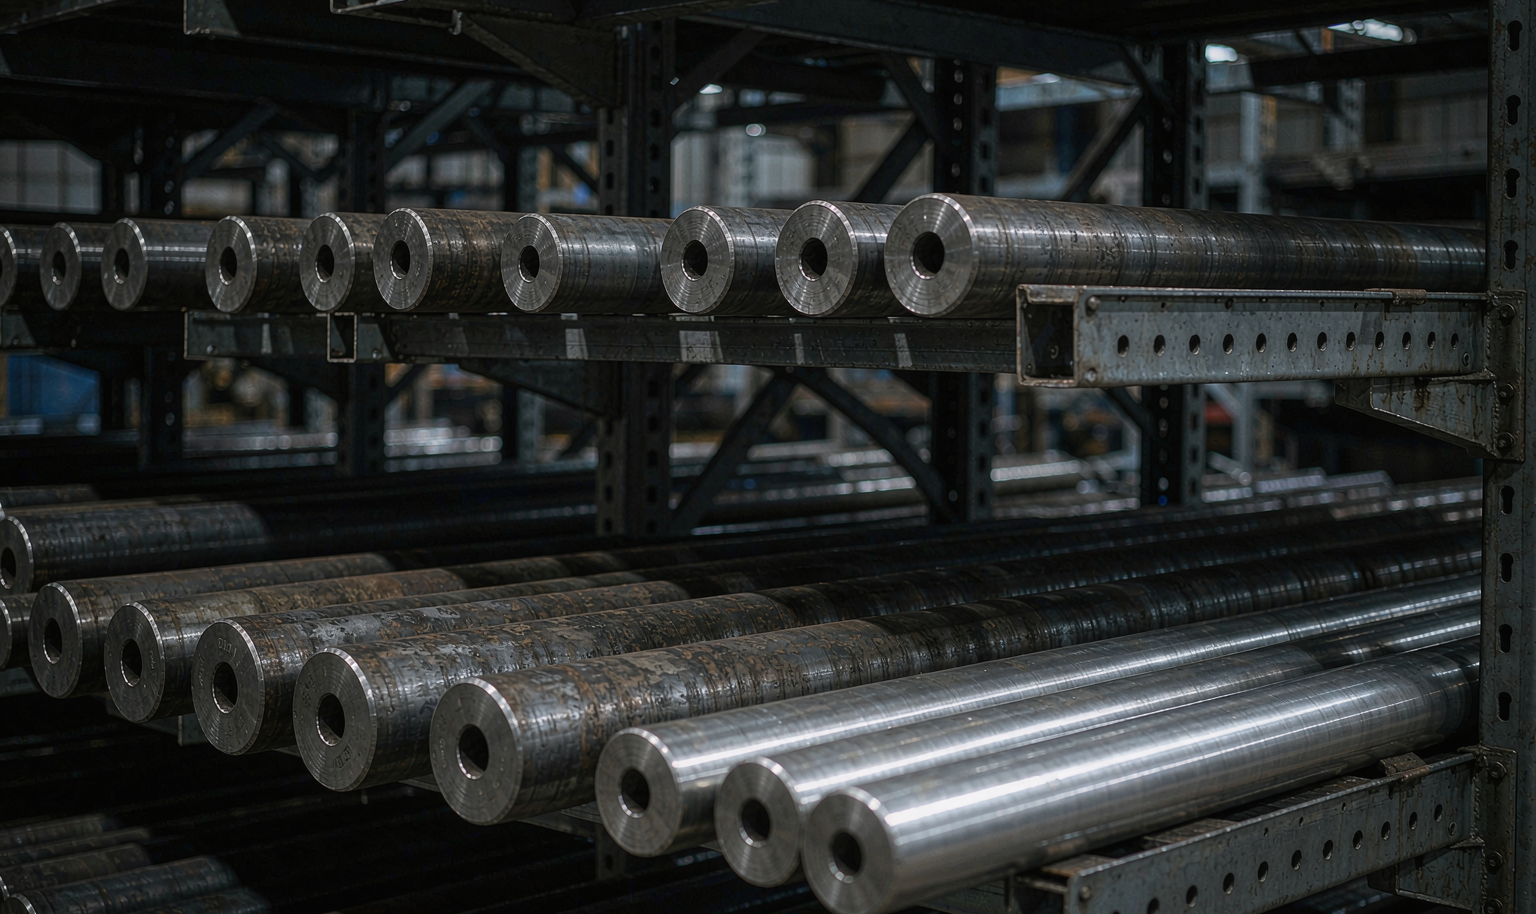
Two practical takeaways. First, 4140 out-performs 4130 in every strength metric — tensile, yield, fatigue limit — typically by 20–35%, and it holds those properties through thicker sections thanks to superior hardenability. As a rule of thumb, 4130 through-hardens reliably to about 50 mm in oil; 4140 does the same to about 80–100 mm, and both grades lose core hardenability quickly beyond those limits (where induction hardening or case carburizing strategies take over). Second, 4130 keeps more ductility and impact toughness at any given strength level, which is exactly why the aerospace and motorsport industries default to 4130 tubing for welded structural frames.
4. Heat Treatment Response
Austenitizing: 4130 soaks at 840–870°C; 4140 at 830–850°C. Soak times follow the standard 1 h per 25 mm of section plus 20–30 min. Quenching: both are oil-quenched as standard; water quenching raises cracking risk, especially in 4140 sections with sharp geometry or above ~40 mm. Tempering: this is where the grades really separate. 4130 tempers at 400–650°C to land in the 850–1000 MPa band; 4140 tempers at 540–680°C for the familiar 28–32 HRC delivery condition, or lower (200–450°C) when 45+ HRC is required — always avoiding the 250–400°C temper embrittlement trough where possible for high-toughness parts.
Buyer checkpoint: put the required hardness band, tempering temperature range, and maximum section size on the purchase order. A mill that Q&Ts 4140 at 620°C and delivers 26 HRC has met “Q&T 4140” as written in many vague RFQs — but may be 4 HRC below what your gear design assumed. Precision on the PO costs nothing; ambiguity costs a re-heat-treatment cycle plus four weeks of freight.
5. Weldability: The Biggest Practical Difference
4130 welds with a controlled procedure: preheat 200–260°C for sections above ~20 mm, low-hydrogen fillers (E8018-B2, ER80S-B2), slow cool, and post-weld stress relief at 600–650°C where practical. Thin-wall 4130 tubing is routinely TIG-welded without dramatic precautions — hence its dominance in roll cages and aircraft frames.
4140 is a reluctant welding steel. With CEV approaching 0.80, it demands preheat of 260–320°C, interpass temperature control, hydrogen-baked electrodes, immediate post-weld hydrogen release at 200–250°C, and a full stress relief or re-temper. Even then, weld-zone hardness mismatch and HAZ softening make welded 4140 joints inferior to the parent metal. Industry practice: if the design can be changed, move welded joints to 4130 or to a mechanical connection and keep 4140 for the machined, through-hardened members.
6. Machinability and Cost
| Factor | 4130 | 4140 |
|---|---|---|
| Machinability rating (B1112 = 100%) | ~65–70% | ~55–60% |
| Carbide turning speed (as-rolled) | 900–1100 SFM | 800–950 SFM |
| Best machining condition | Normalized or annealed | Annealed (≤ 217 HB) or pre-hardened |
| Relative material price | 1.0 (baseline) | 1.05–1.15 |
| Availability in export market | Good (bar/tube/plate) | Excellent (bar/plate/forgings) |
Price difference between the two grades is small — typically 5–15% — so the decision should almost never be driven by cost. If anything, the cost multiplier comes from processing: 4140 Q&T adds heat-treatment and straightening charges, and either grade in peeled, ground, or polished delivery adds 10–30% over hot-rolled. A common money-saving approach on machined parts is ordering 4140 in pre-hardened (28–32 HRC) condition and machining directly, skipping the quench-and-temper cycle and its distortion risk entirely.
7. Typical Applications Compared
| Application | Better Grade | Why |
|---|---|---|
| Aircraft/motorsport structural tubing | 4130 | Weldable, tough, high strength-to-weight in thin walls |
| Roll cages & chassis | 4130 | TIG-weldable, ductile at moderate strength |
| Transmissions shafts & gears | 4140 | Deep hardening, high fatigue limit |
| High-tensile bolts (Class 10.9–12.9) | 4140 | Achieves required strength in larger sections |
| Dies, tooling plates, clamps | 4140 | Wear resistance, 28–32 HRC delivery |
| Welded hydraulic cylinders (barrel ends) | 4130 | Weld-zone integrity |
| Axle shafts & pinions | 4140 | Core strength under torsional fatigue |
| Drill collars / downhole tools | 4140 (or 4145H) | Heavy section hardenability |
8. FAQ
Can 4130 be substituted for 4140 in a pinch?
Only if the design has adequate safety margin at 4130’s lower strength — never acceptable for certified high-strength parts. Substituting in the other direction (4140 for 4130) is usually overkill but creates welding problems. Insist on the specified grade whenever certification is involved.
Which grade is easier to induction harden?
Both respond well to surface hardening at 52–58 HRC. 4140 gives slightly higher surface hardness and a deeper effective case at the same cycle; 4130 is preferred where the part is welded after hardening is impractical. Case depth 1–3 mm is routine for both.
Is 4140 always oil-quenched?
Oil is the standard for crack-free hardening; polymer or water quenching is used selectively on simple geometries to reach deeper hardness, but it raises quench-crack risk substantially in 4140. Ask your supplier to state the quench medium on the heat treatment record.
What certificates should I require for export orders?
EN 10204 3.1 mill test certificates with heat-number traceability, chemistry, tensile, hardness, and (for critical parts) Jominy or CVN data. For oil & gas or safety-critical use, add EN 10204 3.2 with third-party witness of testing.
Which grade is more available in Chinese mills?
4140 (GB 42CrMo) is stocked far more widely than 4130 in bar and plate; 4130 (25CrMo4/GB 30CrMo family) is readily available as seamless tube. Lead times for 4130 bar can be longer, which is another reason it is sometimes mis-sold as 4140 — verify chemistry on the MTC.
Need 4130 or 4140 Bar, Tube, or Plate?
Huaxia-Steel supplies both grades hot-rolled, annealed, or Q&T to your hardness band, with EN 10204 3.1 certification and full chemistry on every heat. Send your drawing or size list — quotation within 24 hours.
Request a quote: Contact Huaxia-Steel.