Carbon Steel Pipe End Preparation: Beveling vs Threading vs Grooving
Pipe end preparation is one of the most overlooked steps in carbon steel procurement, yet it determines whether a pipe will weld cleanly, connect with a fitting or seal under pressure. The three most common preparations are beveling, threading and grooving. Each suits a different connection method, each has its own tolerance standards and each affects the total installed cost. This guide explains when to specify beveled ends (BE), threaded ends (TE) and grooved ends (GE) for your next carbon steel pipe order.
We compare the machining process, applicable standards, joint strength, installation speed, cost and typical applications. By the end you will know which end preparation to write into your purchase specification and what to inspect on arrival.
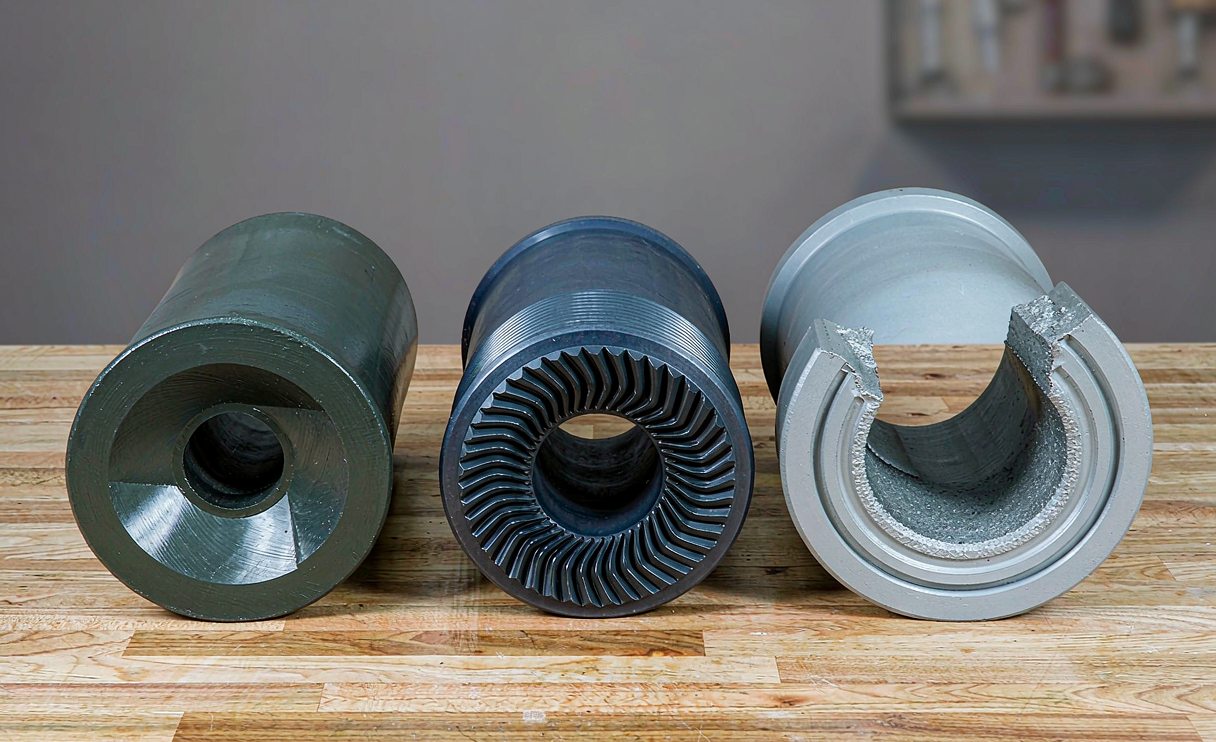
1. What Is Beveled-End Pipe?
A beveled end is machined at an angle to create a V-shaped or U-shaped groove between two pipe ends before welding. The most common angle is 37.5 degrees with a 1.6 mm root face, as specified by ASME B16.25 for butt-welding pipe. Beveled ends are standard for long-distance pipelines, process piping, high-pressure systems and any application where a full-penetration butt weld is required.
2. What Is Threaded-End Pipe?
Threaded ends are cut with tapered or straight threads, usually NPT (National Pipe Thread) or BSPT, so the pipe screws into a coupling, fitting or valve. Threaded connections are common in low-pressure plumbing, fire protection, utility lines and small-bore piping where welding is impractical. The threads must be clean, free of burrs and coated with thread sealant or tape during installation.
3. What Is Grooved-End Pipe?
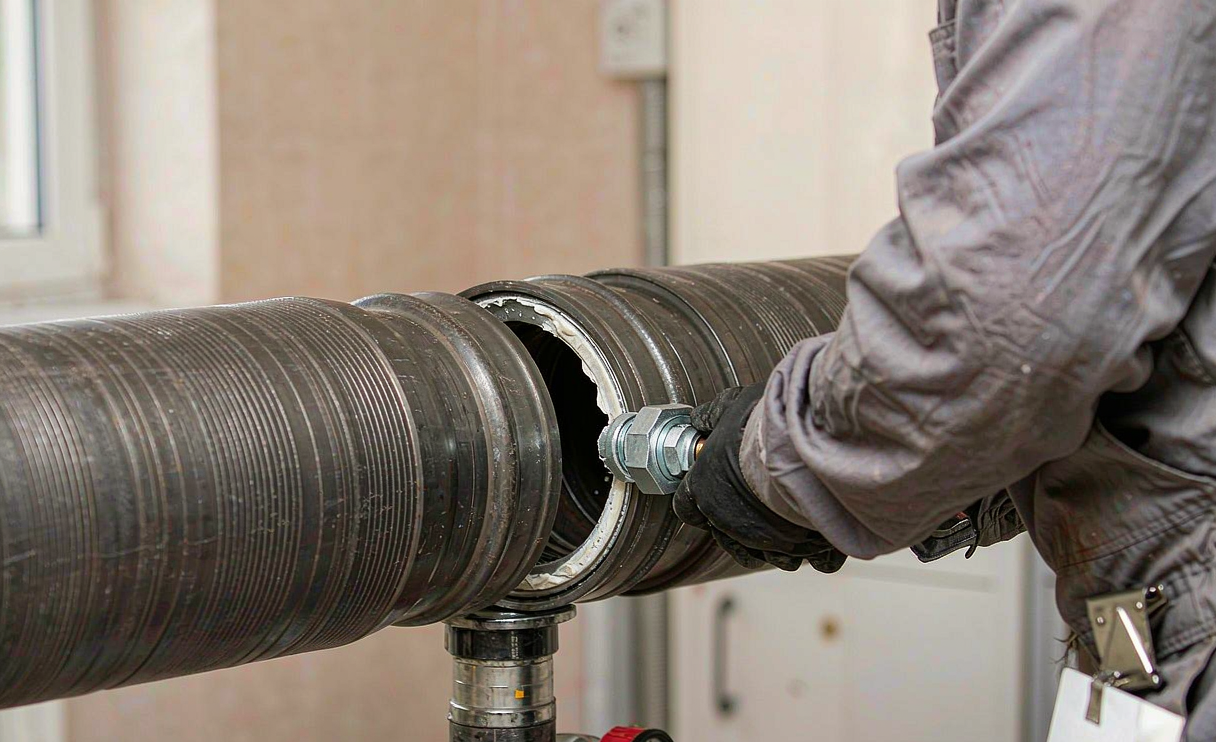
Grooved ends have a circumferential groove rolled or cut near the pipe end. A coupling with rubber gaskets and housing segments fits over the groove and is tightened with bolts. Grooved systems are fast to install, allow some axial movement and are widely used in fire suppression, HVAC, water distribution and mining slurry lines. Victaulic-style grooved couplings dominate this market.
4. Comparison Table
| Feature | Beveled End (BE) | Threaded End (TE) | Grooved End (GE) |
|---|---|---|---|
| Connection method | Butt weld | Screwed coupling/fitting | Grooved coupling with gasket |
| Joint strength | Very high, full penetration | Moderate, thread engagement | Moderate, mechanical grip |
| Pressure rating | High to very high | Low to medium | Low to medium-high |
| Installation speed | Slow (welding + NDT) | Fast | Very fast |
| Skill required | Welder + inspector | Fitter | Fitter |
| Reusability | Permanent | Removable with care | Removable and reusable |
| Typical standards | ASME B16.25, API 5L | ASME B1.20.1, ISO 7/1 | ASTM A53, AWWA C606 |
| Common sizes | 2″ – 120″ | 1/8″ – 6″ | 1″ – 24″ |
| Relative cost | Medium-high | Low | Medium |
5. Standards and Tolerances
Each end preparation has its own tolerance and inspection requirements. Bevel angles are usually checked with a bevel gauge or optical comparator. Threaded ends are gauged with ring and plug gauges. Groove dimensions are checked with a groove micrometer or dedicated Victaulic gauge. The table below lists the key standards buyers should reference.
| End type | Key standards | Inspection focus |
|---|---|---|
| Beveled | ASME B16.25, ASME B31.3, API 5L | Angle, root face, root gap, surface finish |
| Threaded | ASME B1.20.1, ISO 7-1, BS 21 | Thread length, taper, burrs, chamfer |
| Grooved | AWWA C606, ASTM A53, Victaulic specs | Groove width, depth, concentricity, OD tolerance |
6. When to Specify Each End Preparation
- Specify beveled ends for high-pressure pipelines, process piping, oil and gas lines, power plant piping, cryogenic systems and any application where weld integrity is safety-critical.
- Specify threaded ends for plumbing, fire protection sprinkler systems, instrumentation lines, compressed air, low-pressure utility piping and field repairs where welding equipment is not available.
- Specify grooved ends for fire suppression, HVAC chilled water, mining slurry, building services and any project where fast installation, vibration tolerance and future dismantling are important.
7. Cost and Lead-Time Considerations
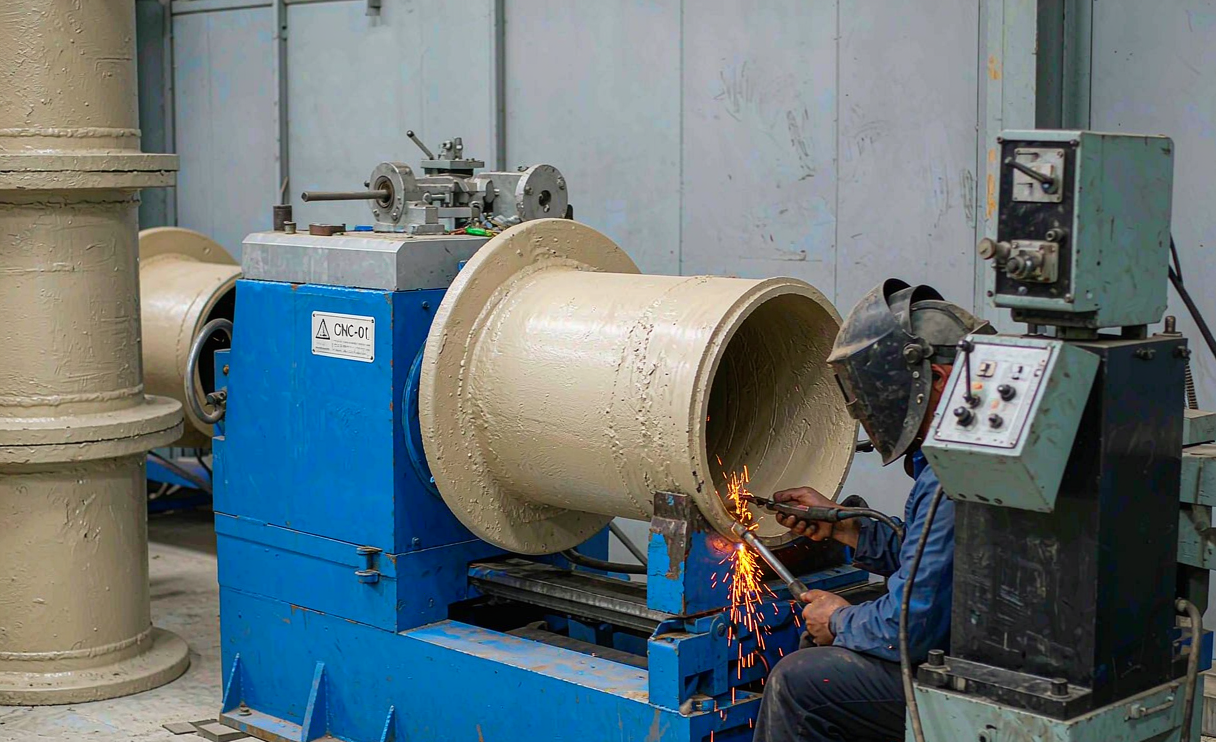
Beveled ends add machining cost and require welded installation, but they eliminate the cost of couplings and flanges. Threaded ends are the cheapest to produce and install, but they limit pressure rating and pipe wall thickness. Grooved ends require a groove-rolling or cutting operation and the purchase of proprietary couplings, yet the labor savings on large commercial projects often offset the material premium.
When you write your purchase order, state the end preparation explicitly in the line-item description. For example: “ASTM A53 Gr.B seamless pipe, 6″ Sch40, plain ends/beveled ends per ASME B16.25, length 6 m, quantity 100 pcs.” Ambiguity is the main cause of rejected pipe on site.
8. Inspection Checklist on Arrival
- Verify end type matches the purchase order (BE / TE / GE / PE).
- Check bevel angle, root face and land length against ASME B16.25.
- Check thread gauge fit and thread length for NPT/BSPT ends.
- Measure groove width, depth and distance from pipe end for grooved ends.
- Inspect for burrs, dents, ovality and coating damage.
- Confirm protective end caps are in place during transit.
FAQ
Can the same pipe have different end preparations on each end?
Yes. It is common to order pipe with one beveled end and one threaded end, or with a flange welded to one end and a bevel on the other. Always specify the requirement clearly in your PO.
What does PE mean on a pipe specification?
PE stands for plain end, meaning the pipe is cut square with no bevel, thread or groove. Plain-end pipe is usually field-prepared or welded with backing rings.
Are grooved couplings suitable for high pressure?
Standard grooved couplings are rated up to about 25 bar, depending on size and coupling style. Higher-pressure applications require heavy-duty or flanged connections and butt-welded beveled ends.
Should I specify thread sealant for threaded pipe?
Yes. NPT threads are not self-sealing. PTFE tape or approved pipe dope must be applied to prevent leaks. The specification should state the acceptable sealant type for the service.
Can Huaxia Steel supply pipe with machined ends?
Yes. We supply carbon steel seamless and welded pipe with beveled, threaded, grooved or plain ends to ASME, API and ASTM standards. End caps and rust-preventive coating are available on request.
Order Carbon Steel Pipe with the Right End Preparation
Send us your pipe size, wall thickness, grade and end-preparation requirement. Our team will confirm the correct standard and machining tolerance before production. Request a quote for beveled, threaded or grooved carbon steel pipe today.
9. Bevel Geometry Details
ASME B16.25 defines several bevel profiles for butt-welding pipe. The most common is the standard V bevel with a 37.5-degree angle and a 1.6 mm root face. For thicker walls, a compound bevel or J-bevel reduces the volume of weld metal and distortion. The root opening is typically 1–3 mm and must be controlled during fit-up to ensure full penetration without burn-through.
| Bevel type | Angle | Best for |
|---|---|---|
| Standard V | 37.5° | Wall thickness 3 – 20 mm |
| Compound V | Variable | Wall thickness 20 – 50 mm |
| U / J bevel | Curved root | Thick wall, high-volume production |
| Square butt | 0° | Thin wall, automatic TIG |
10. Grooving Methods: Roll Grooving vs Cut Grooving
Roll grooving forms the groove by pressing rotating dies against the pipe OD. It is fast, produces no chips and is preferred for thin-wall pipe. Cut grooving removes material with a cutter and is used for thicker walls or when the pipe is already lined. The table below compares the two methods.
| Method | Speed | Wall thickness | Deformation | Cost |
|---|---|---|---|---|
| Roll grooving | Very fast | Thin to medium | Slight OD compression | Lower |
| Cut grooving | Moderate | Medium to thick | Minimal | Higher |
11. Thread Sealants and Compatibility
Threaded carbon steel connections rely on sealant to fill the spiral leak path. The choice of sealant depends on the service fluid, temperature and whether the joint will be disassembled. PTFE tape is common for water and air. Anaerobic pipe sealants cure in the absence of air and are used where vibration loosening is a concern. For fuel oil, gas and high-temperature steam, use a sealant rated for the specific service.
- PTFE tape: water, compressed air, general low-pressure service
- Anaerobic sealant: permanent or semi-permanent joints, vibration resistance
- Hemp and paste: traditional plumbing, gas lines in some regions
- High-temperature thread compound: steam, hot oil and thermal cycling
12. Buyer Checklist for Pipe End Preparation
- Define end type clearly: PE / BE / TE / GE / BW / SW / FL.
- Reference the applicable standard (ASME B16.25, B1.20.1, AWWA C606).
- Specify pipe length tolerance with end preparation included.
- Ask for end-cap protection during transit.
- Require inspection report for thread gauge fit or groove dimensions.
- Confirm surface preparation and coating around machined ends.