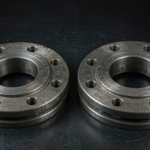
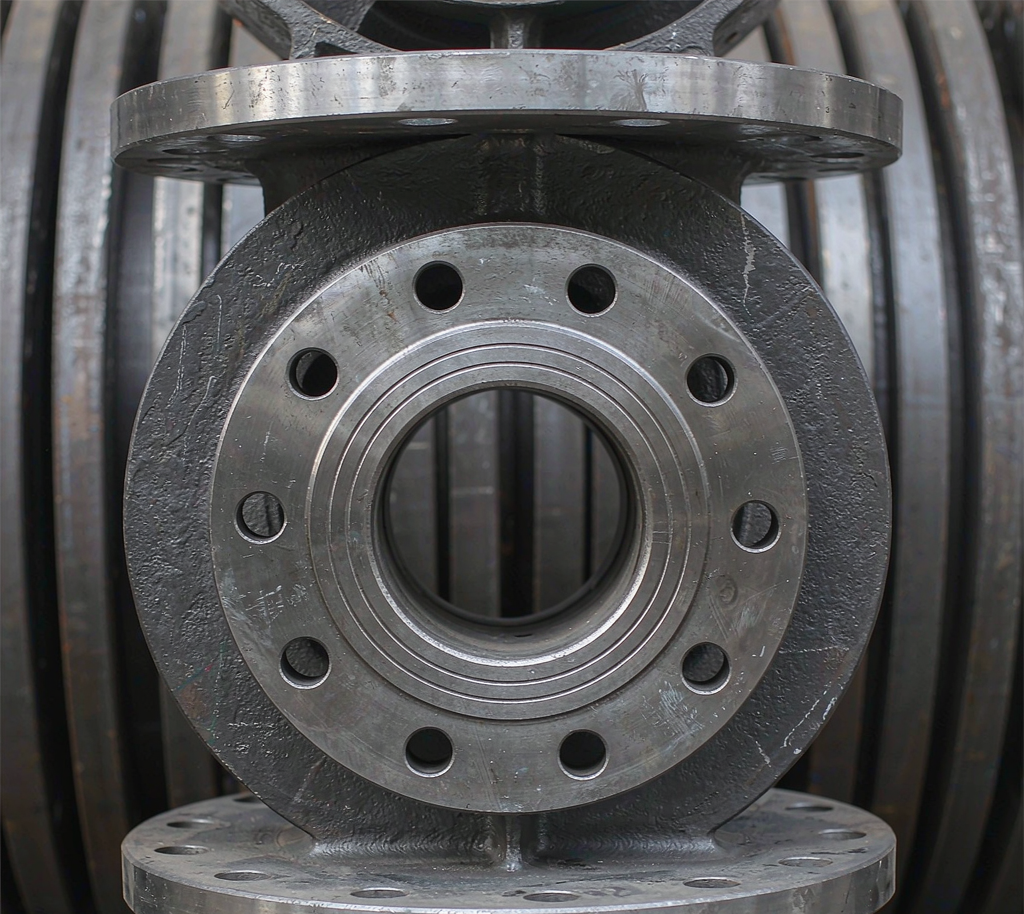
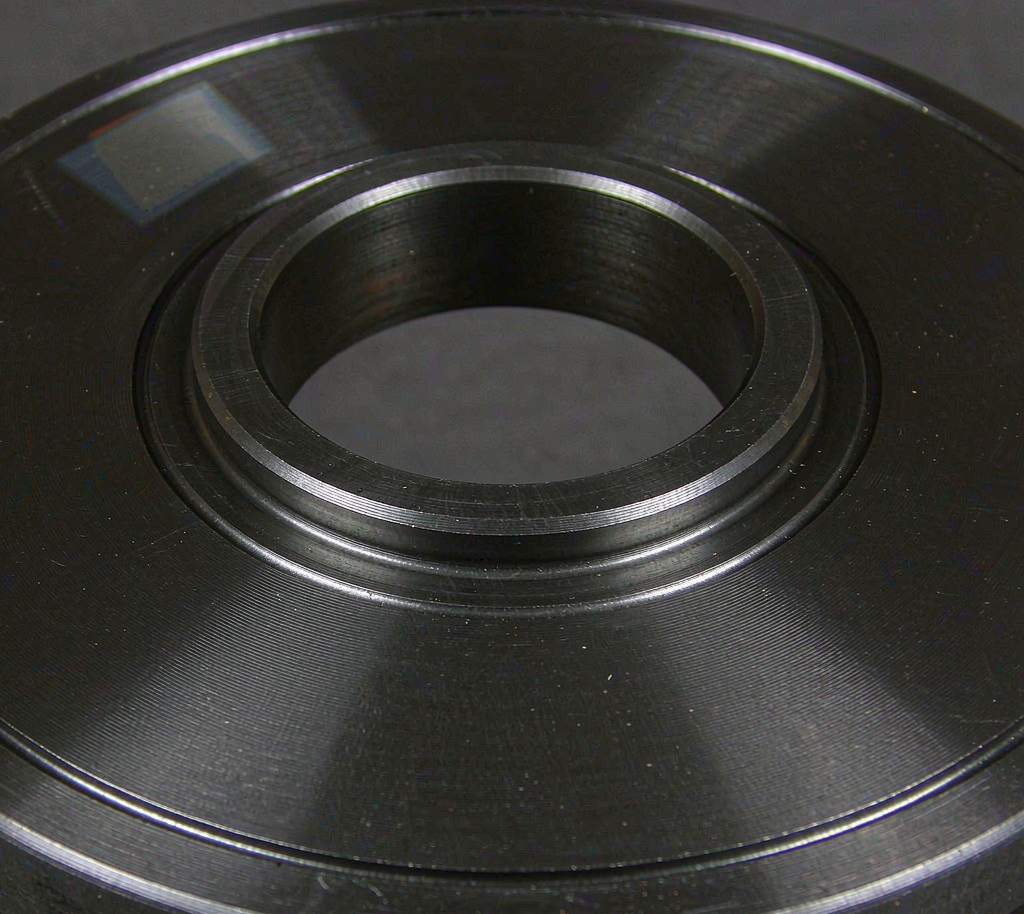
The EN 1092-1 plate flange (Type 01) is the most economical flange style in the European system: a flat disc cut from steel plate, drilled to the standard bolt pattern, and slipped over the pipe before a single fillet weld joins it. Used across water treatment, HVAC, fire protection, shipbuilding and low-pressure process piping, plate flanges cost 30–50% less than forged slip-on or weld-neck flanges while delivering reliable service up to PN40 on many sizes. Huaxia-Steel exports Type 01 plate flanges in DN15–DN600, PN6–PN40, in carbon steel grades P250GH and S235JR with EN 10204 3.1 certification.
Product Overview
EN 1092-1 defines flange types by a two-digit code: Type 01 is the plate flange for welding, Type 02 the loose plate flange, Type 05 blank (blind), Type 11 weld-neck and so on. The Type 01 plate flange is characterized by its flat, unhubbed profile and bore equal to the pipe OD plus a small clearance. Because it is cut from rolled plate rather than forged, the grain structure is not flow-optimized — which is why design codes restrict plate flanges to moderate pressure-temperature combinations and why the standard’s pressure/temperature rating tables must be checked against your system conditions.
Dimensions and Specifications
| Size | OD (PN16) | Bolt circle | Bolts | Flange thickness |
|---|---|---|---|---|
| DN50 | 165 mm | 125 mm | 4 × M16 | 18 mm |
| DN80 | 200 mm | 160 mm | 8 × M16 | 20 mm |
| DN100 | 220 mm | 180 mm | 8 × M16 | 20 mm |
| DN150 | 285 mm | 240 mm | 8 × M20 | 22 mm |
| DN200 | 340 mm | 295 mm | 12 × M20 | 24 mm |
| DN300 | 445 mm | 400 mm | 12 × M20 | 26 mm |
| DN400 | 565 mm | 515 mm | 16 × M24 | 28 mm |
| DN500 | 670 mm | 620 mm | 20 × M24 | 30 mm |
| DN600 | 780 mm | 725 mm | 20 × M27 | 32 mm |
Above dimensions are indicative for PN16; PN10 shares the same bolt pattern through DN300 (interchangeability), while PN25/PN40 use thicker flanges and larger bolt sizes per the EN 1092-1 tables. Full dimension certificates are issued with each order, and machining to customer drawings is supported.
Materials and Grades
| EN material | Type | Typical use |
|---|---|---|
| S235JR (1.0038) | Structural plate | Water, HVAC, general service to 0 °C |
| P250GH (1.0460) | Pressure-grade plate | Pressure piping per EN 13445 context |
| P265GH (1.0425) | Pressure-grade plate | Higher temperature service |
| 16Mo3 / alloy options | Alloy plate | Elevated temperature on request |
Manufacturing and Tolerances
Production route: plate sourcing with 3.1 certificates → plasma or laser profile cutting of the ring blank → facing of the sealing surface (raised face type B1 per EN 1092-1, or flat face) → drilling on CNC multi-spindle tables → deburring and marking. Key tolerances: flange OD ±1.5 mm (DN ≤ 200) to ±4 mm (DN 600); thickness not below the nominal value in the standard tables; bolt hole spacing ±1.0 mm; raised face height +0.5/0 mm. Sealing surface roughness Ra 3.2–6.3 μm for spiral-wound gasket seating; hydrostatic or pneumatic testing of the mating system is done on site, not on the flange.
Surface Treatment Options
- Black (self-color) with anti-rust oil — default for welding into coated systems.
- Hot dip galvanized to EN ISO 1461 — water and fire mains.
- Electro-galvanized or painted (epoxy/RAL) on request.
Applications
Plate flanges join pipes to valves, pumps, meters and vessel nozzles in waterworks, district heating, fire sprinkler networks, ballast systems and low-pressure utility headers. They are the standard choice when cost matters and system pressure is moderate; for high pressure, thermal cycling or critical refinery service, upgrade to Type 11 weld-neck flanges whose hub gives better fatigue performance.
Quality Assurance and Certification
- Material certificates EN 10204 3.1 per heat; 3.2 via third-party on request.
- Dimensional inspection report with bolt-hole template check and thickness survey per lot.
- Marking per EN 1092-1: manufacturer, material grade, DN/PN designation and type (01/B1).
- PMI or spectrographic verification on request for mixed-material projects.
Packing and Shipping
Flanges are packed in plywood or steel pallets with bolt-hole protectors and interleaved cardboard, seaworthy wrapped and labeled with DN/PN/grade and quantity. Container loads of 20–25 tonnes are standard; small mixed-size orders are consolidated on one pallet set for single-container shipping. Typical delivery: 7–15 days from stock for common PN10/PN16 sizes, 20–30 days for production runs and special pressure classes.
PN Class Comparison: Choosing the Right Rating
PN (pressure nominal) classes define the flange’s pressure-temperature envelope with the mating gasket and bolts. For most utility systems the choice collapses quickly:
| Class | Max pressure at 20 °C (approx.) | Typical service | Cost index (DN100) |
|---|---|---|---|
| PN6 | 6 bar | Ventilation, low-pressure water | 0.8 |
| PN10 | 10 bar | Water mains, irrigation, fire lines | 1.0 |
| PN16 | 16 bar | District heating, compressed air, general process | 1.15 |
| PN25 | 25 bar | Process headers, pump discharge | 1.35 |
| PN40 | 40 bar | Higher-pressure utilities, chemical transfer | 1.6 |
Interchangeability matters in retrofit work: PN10 and PN16 flanges share bolt patterns through DN300 (drilling differs above DN300), so a PN16 flange can replace PN10 in the field without re-drilling pipe — one reason PN16 is the export default even where PN10 would technically suffice.
Type 01 vs Other EN 1092-1 Flange Types
| Type | Name | Hub | Relative strength | Relative cost |
|---|---|---|---|---|
| 01 | Plate flange for welding | None | Moderate | 1.0 (baseline) |
| 02 | Loose plate flange | None, used with lap stub | Moderate | 1.1–1.2 |
| 04 | Loose flange with neck | On collar | Higher | 1.3 |
| 11 | Weld-neck flange | Tapered hub | Highest (fatigue rated) | 1.6–2.0 |
The rule of thumb used by piping engineers: below PN16 and 200 °C with low cyclic loading, Type 01 plate flanges are fully appropriate. Above that envelope — high pressure, thermal cycling, vibration, or safety-critical containment — the weld-neck’s forged hub earns its premium.
Gaskets and Bolt Torque Guidance
Raised face type B1 surfaces pair with spiral-wound gaskets (with centering ring) on PN16 and above, and with EPDM/NBR flat gaskets on water systems. Suggested assembly torque for M16 bolts on DN100 PN16 with a spiral-wound gasket starts around 90–110 N·m, tightened in a star pattern in three passes (30%, 60%, 100%) — always defer to the gasket manufacturer’s tables for your media and temperature. Supplying galvanized flanges with galvanized A2-70 bolts and coated washers avoids mixed-metal corrosion in outdoor water service.
Frequently Asked Questions
Are EN 1092-1 flanges compatible with ANSI B16.5 flanges?
No — the bolt patterns, raised face diameters and pressure ratings differ. Mixing the two systems requires transition flanges or adapters; verify drilling templates before ordering valves to connect into an EN flanged line.
Can plate flanges be galvanized after cutting?
Yes, and it is standard practice for water works. Hot dip galvanizing adds 50–85 μm of zinc; drill holes stay clear because drilling happens before galvanizing, and the coating thickness inside bolt holes remains adequate for M16–M27 hardware.
What plate thickness should I expect for DN300 PN16?
Per EN 1092-1 the DN300 PN16 Type 01 flange is approximately 26 mm thick with 12 × M20 bolts on a 400 mm bolt circle — confirm against the official table for your gasket type and facing.
Inspection Before Shipment
- Dimensional survey: OD, bolt circle, hole diameter, hole count, thickness and bore — checked against the EN 1092-1 table for the declared DN/PN.
- Facing inspection: raised face concentricity, surface roughness and freedom from scratches or tool chatter across the sealing band.
- Material verification: heat number transfer from plate cert to finished flange, with optional PMI on alloy orders.
- Coating check: galvanizing thickness and adhesion where specified.
- Packing audit: hole protectors, pallet integrity and label legibility in the destination language.
Ordering Checklist and Common Mistakes
- State the full designation: “EN 1092-1 Type 01 / PN16 / DN150 / B1 / S235JR” leaves no ambiguity.
- Confirm facing type — raised face B1 is standard, flat face is common on cast-iron or plastic connections; mixing them breaks the seal.
- Do not assume PN10/PN16 interchangeability above DN300 — drilling differs.
- Match bore to pipe OD, not NB — a DN150 flange must be bored for 168.3 mm pipe unless your system uses a different series.
- Ask for the test report with the goods, not after shipment.
Flange orders are simple but unforgiving: a wrong bolt circle or facing type turns every flange in the container into scrap. A ten-line RFQ with the full designation and a dimension sheet for approval removes that risk entirely.
Welding Plate Flanges: Practical Notes
Type 01 plate flanges are attached with two fillet welds: one on the outside face and one, where access permits, on the inside. Fit-up is the discipline that decides whether the joint leaks: square the flange to the pipe within 1 mm across the face, maintain a 1.5–3 mm gap, and tack at four points 90° apart before welding. Weld with E7018 or equivalent low-hydrogen consumables; the flange material’s low CEV means preheat is normally unnecessary below 25 mm. After welding, re-check face squareness — a flange pulled out of square by uneven weld shrinkage will not seat and will weep under pressure. For galvanized systems, weld first, then repair the zinc locally with cold galvanizing compound.
Storage and Handling
Flanges should be stored flat on pallets, not stacked on edge where sealing faces rub and scratch. Protect raised faces with cardboard or plastic rings until assembly, keep galvanized and black stock separated to avoid zinc contamination on painted fabrication, and store bolts and gaskets in a dry store — a rusty bolt set costs more in downtime than the whole flange assembly. On site, never use a flange as a lifting point or step; a distorted sealing face is unrecoverable in the field.
Why Source Plate Flanges Factory Direct
Flange orders are repetitive: once a project is approved, the same DN/PN list is re-ordered for years. Sourcing direct locks in three advantages — stable pricing tied to plate index rather than to a trader’s spot margin, consistent dimensional geometry from the same CNC drilling programme so replacement flanges fit existing pipework, and complete heat traceability from plate certificate to finished part. Our export team keeps approved dimension sheets on file for each client, so re-orders need only a purchase order reference rather than a fresh approval cycle.
Request a Plate Flange Quote
Send your DN/PN list, material grade and destination port — Huaxia-Steel replies within 24 hours with FOB/CIF pricing, stock photos of actual inventory and a dimension sheet for your approval before production.